To view the technical documents, please fill out the form below. We will get back to you as soon as possible and you can log in and review with the password given by us. If you have a password, you can log in and continue by clicking "Sign In".
You can access the documentation by logging in from this area with the password given to you.
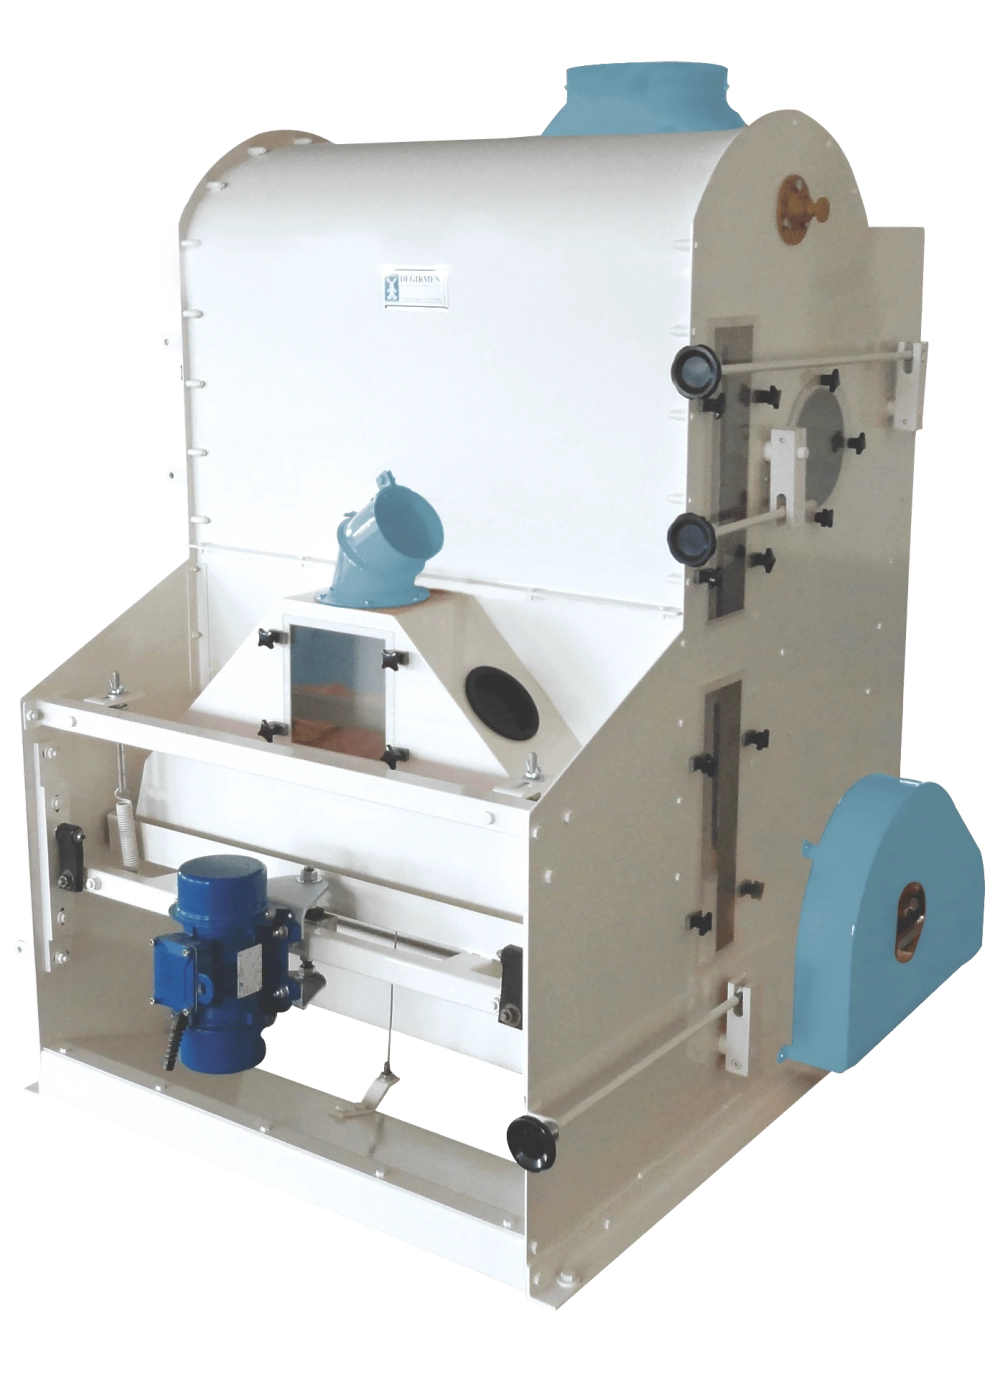
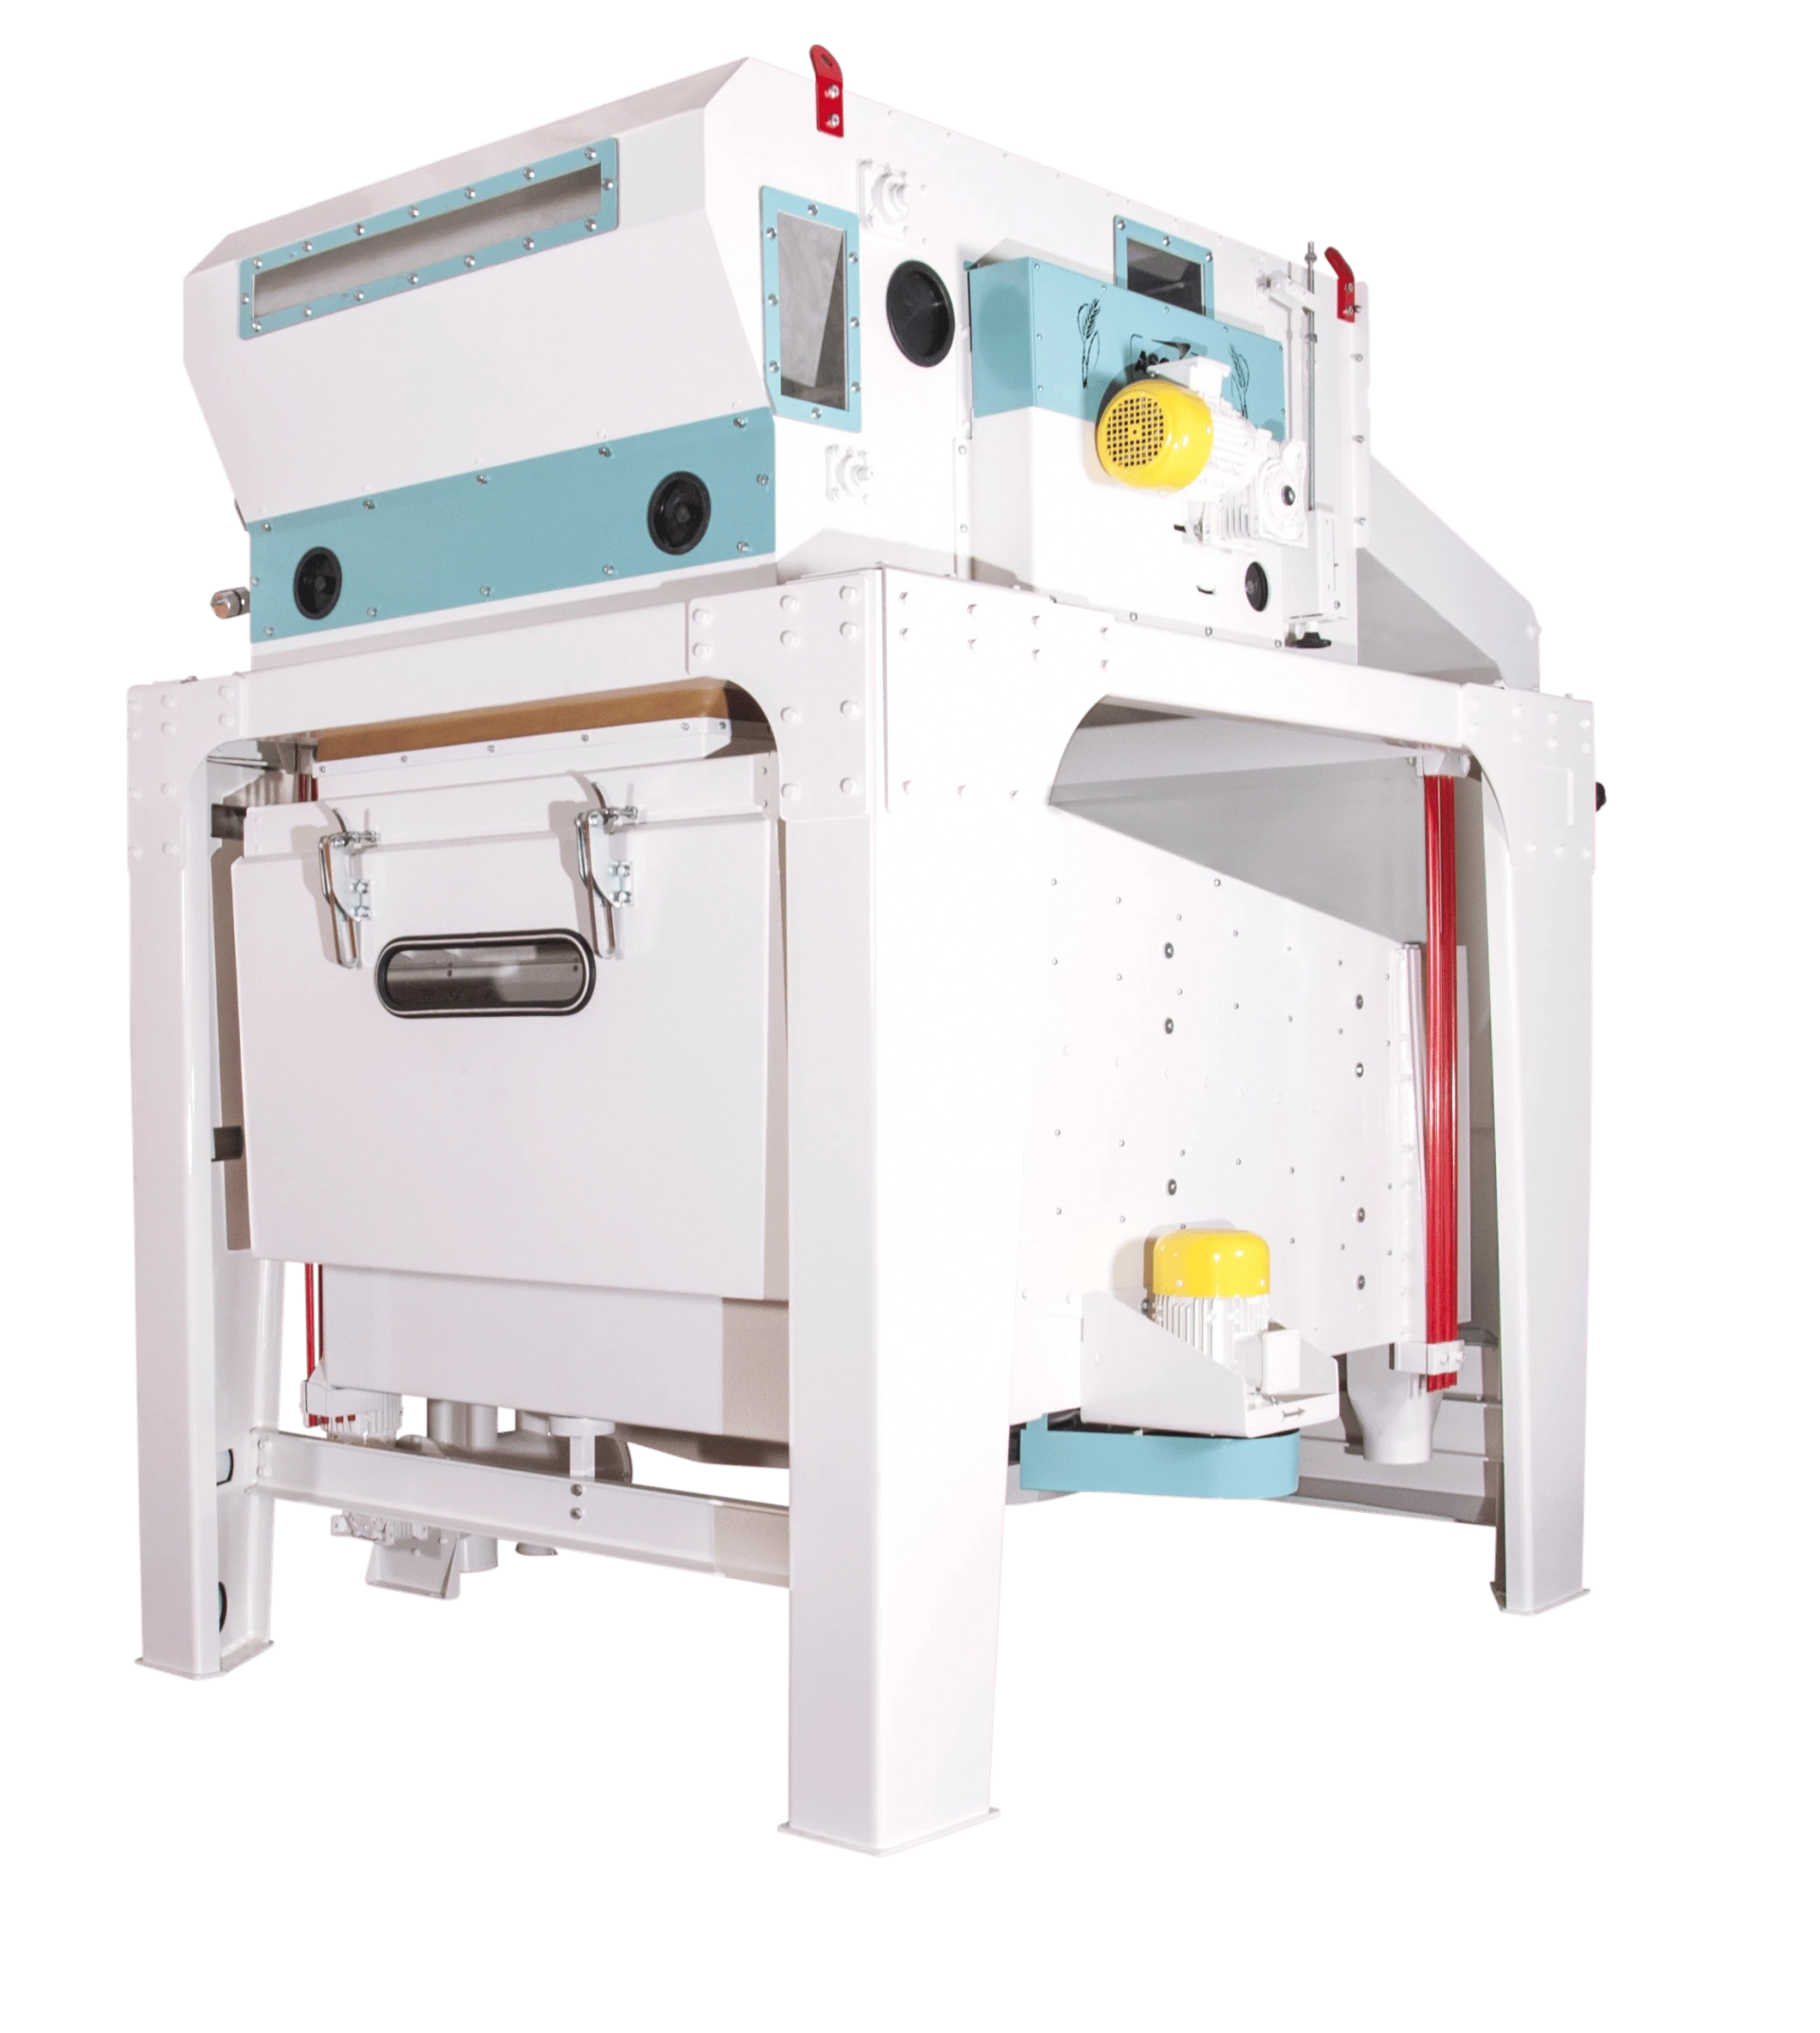
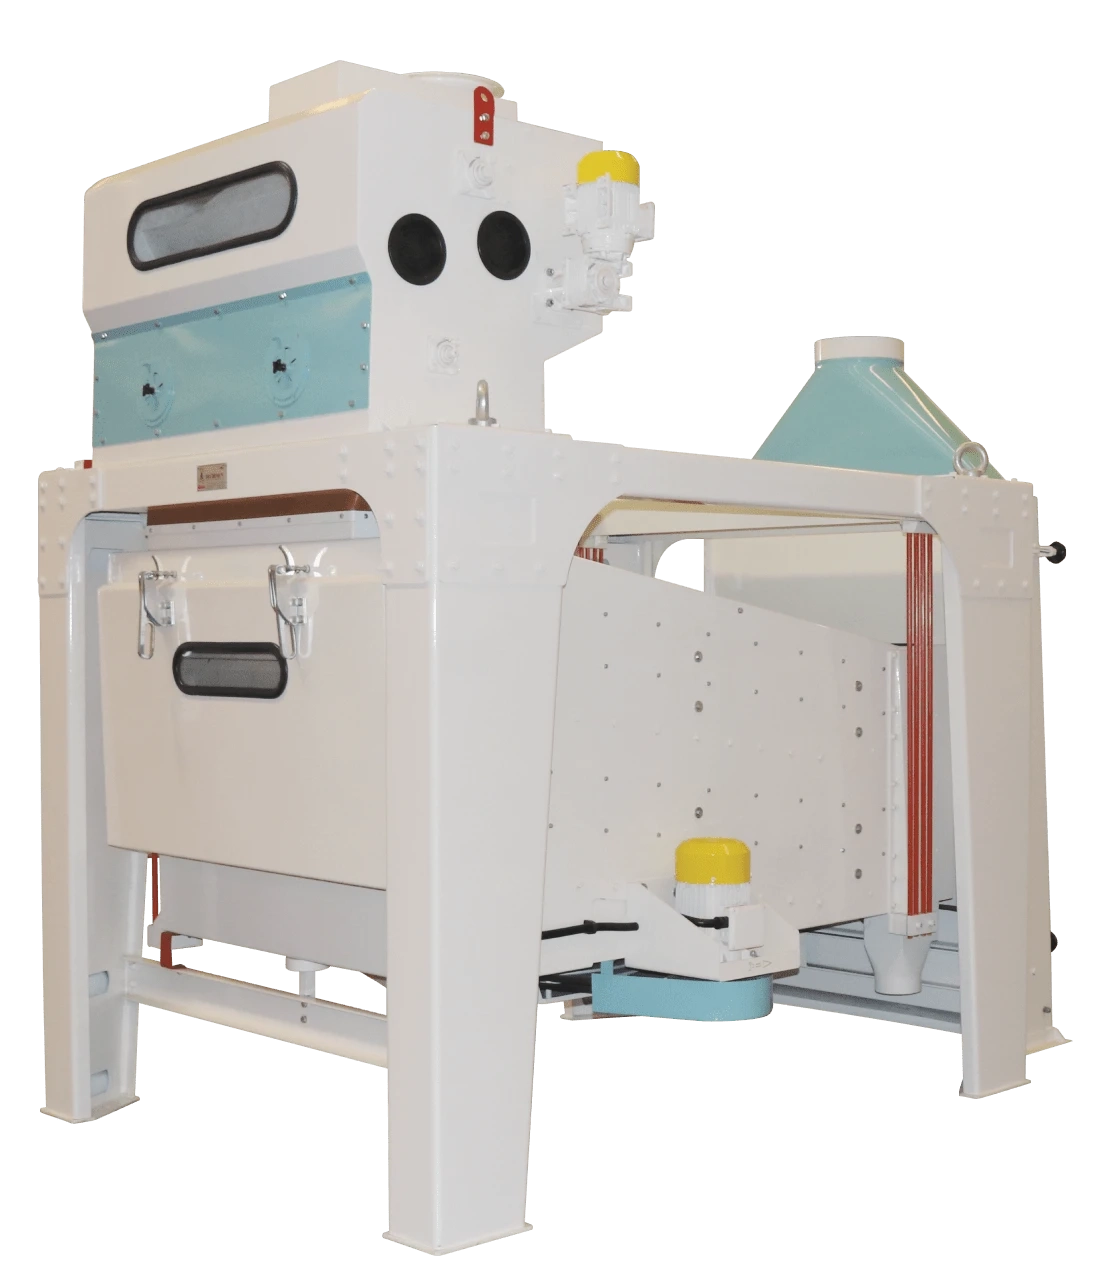
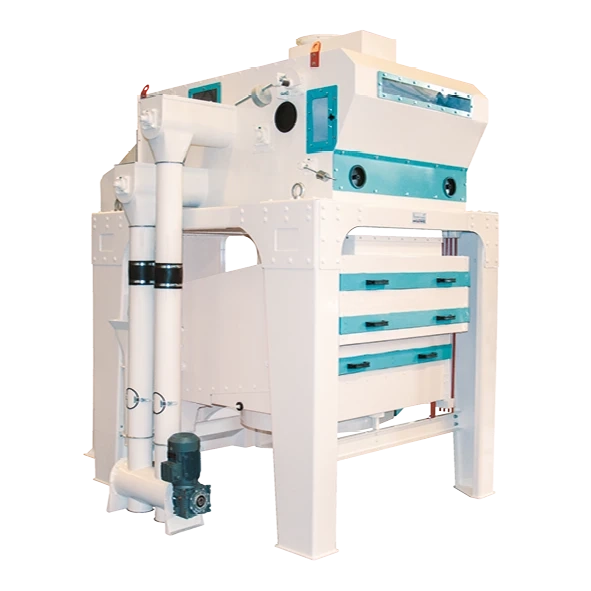
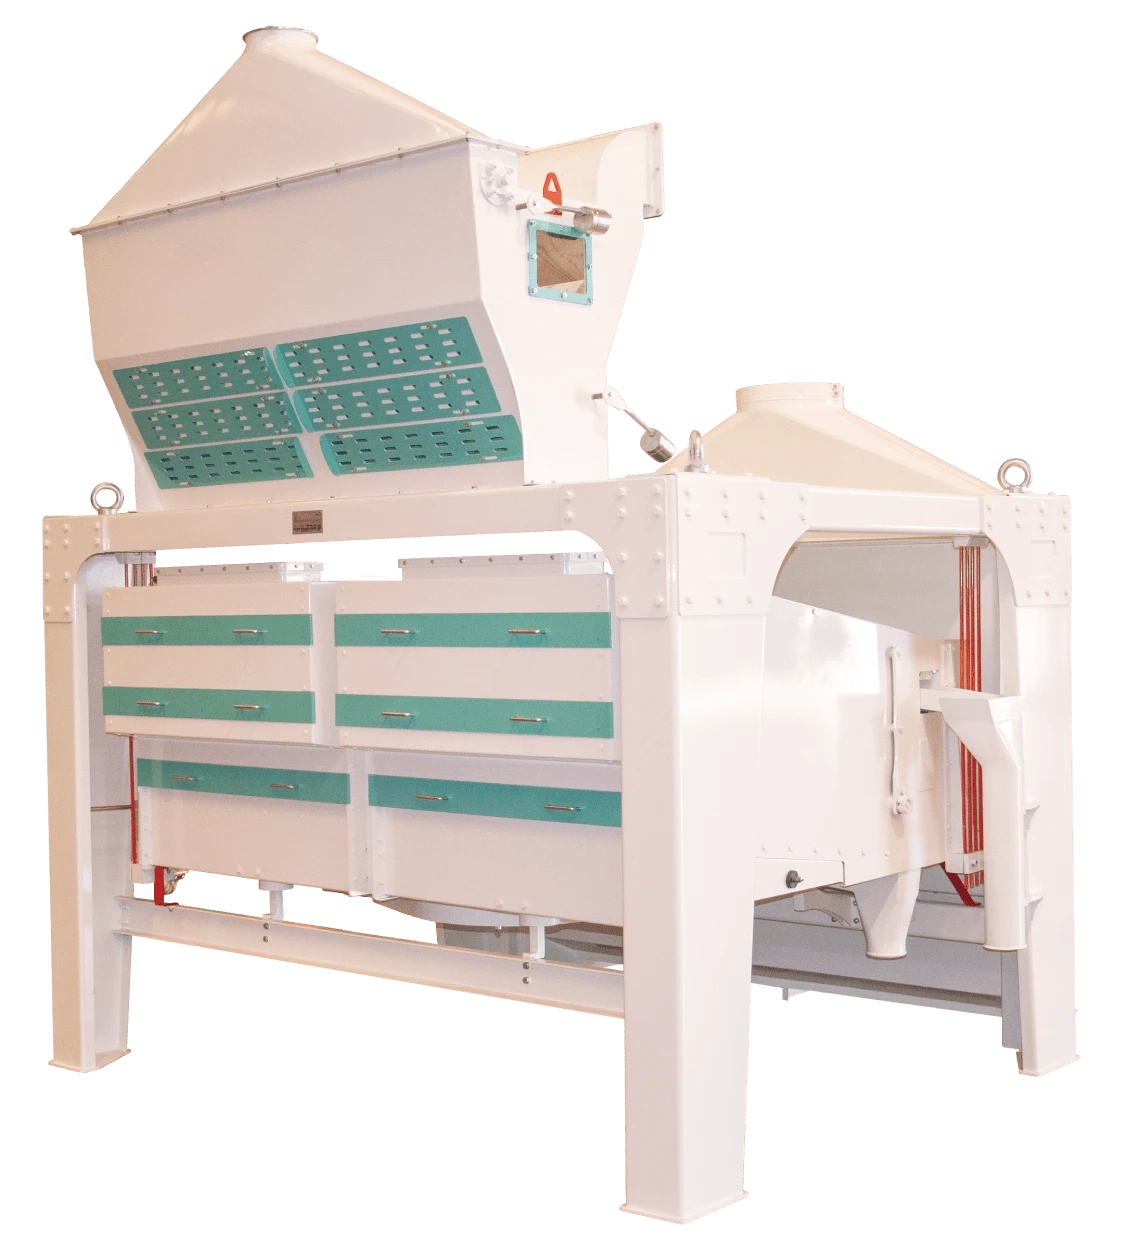
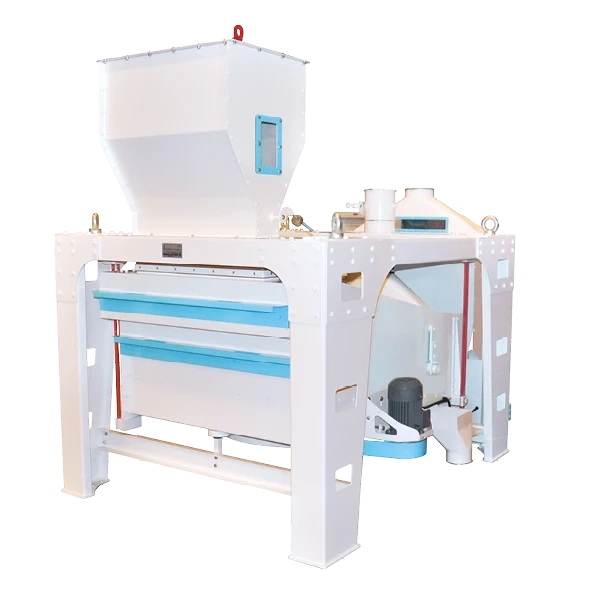
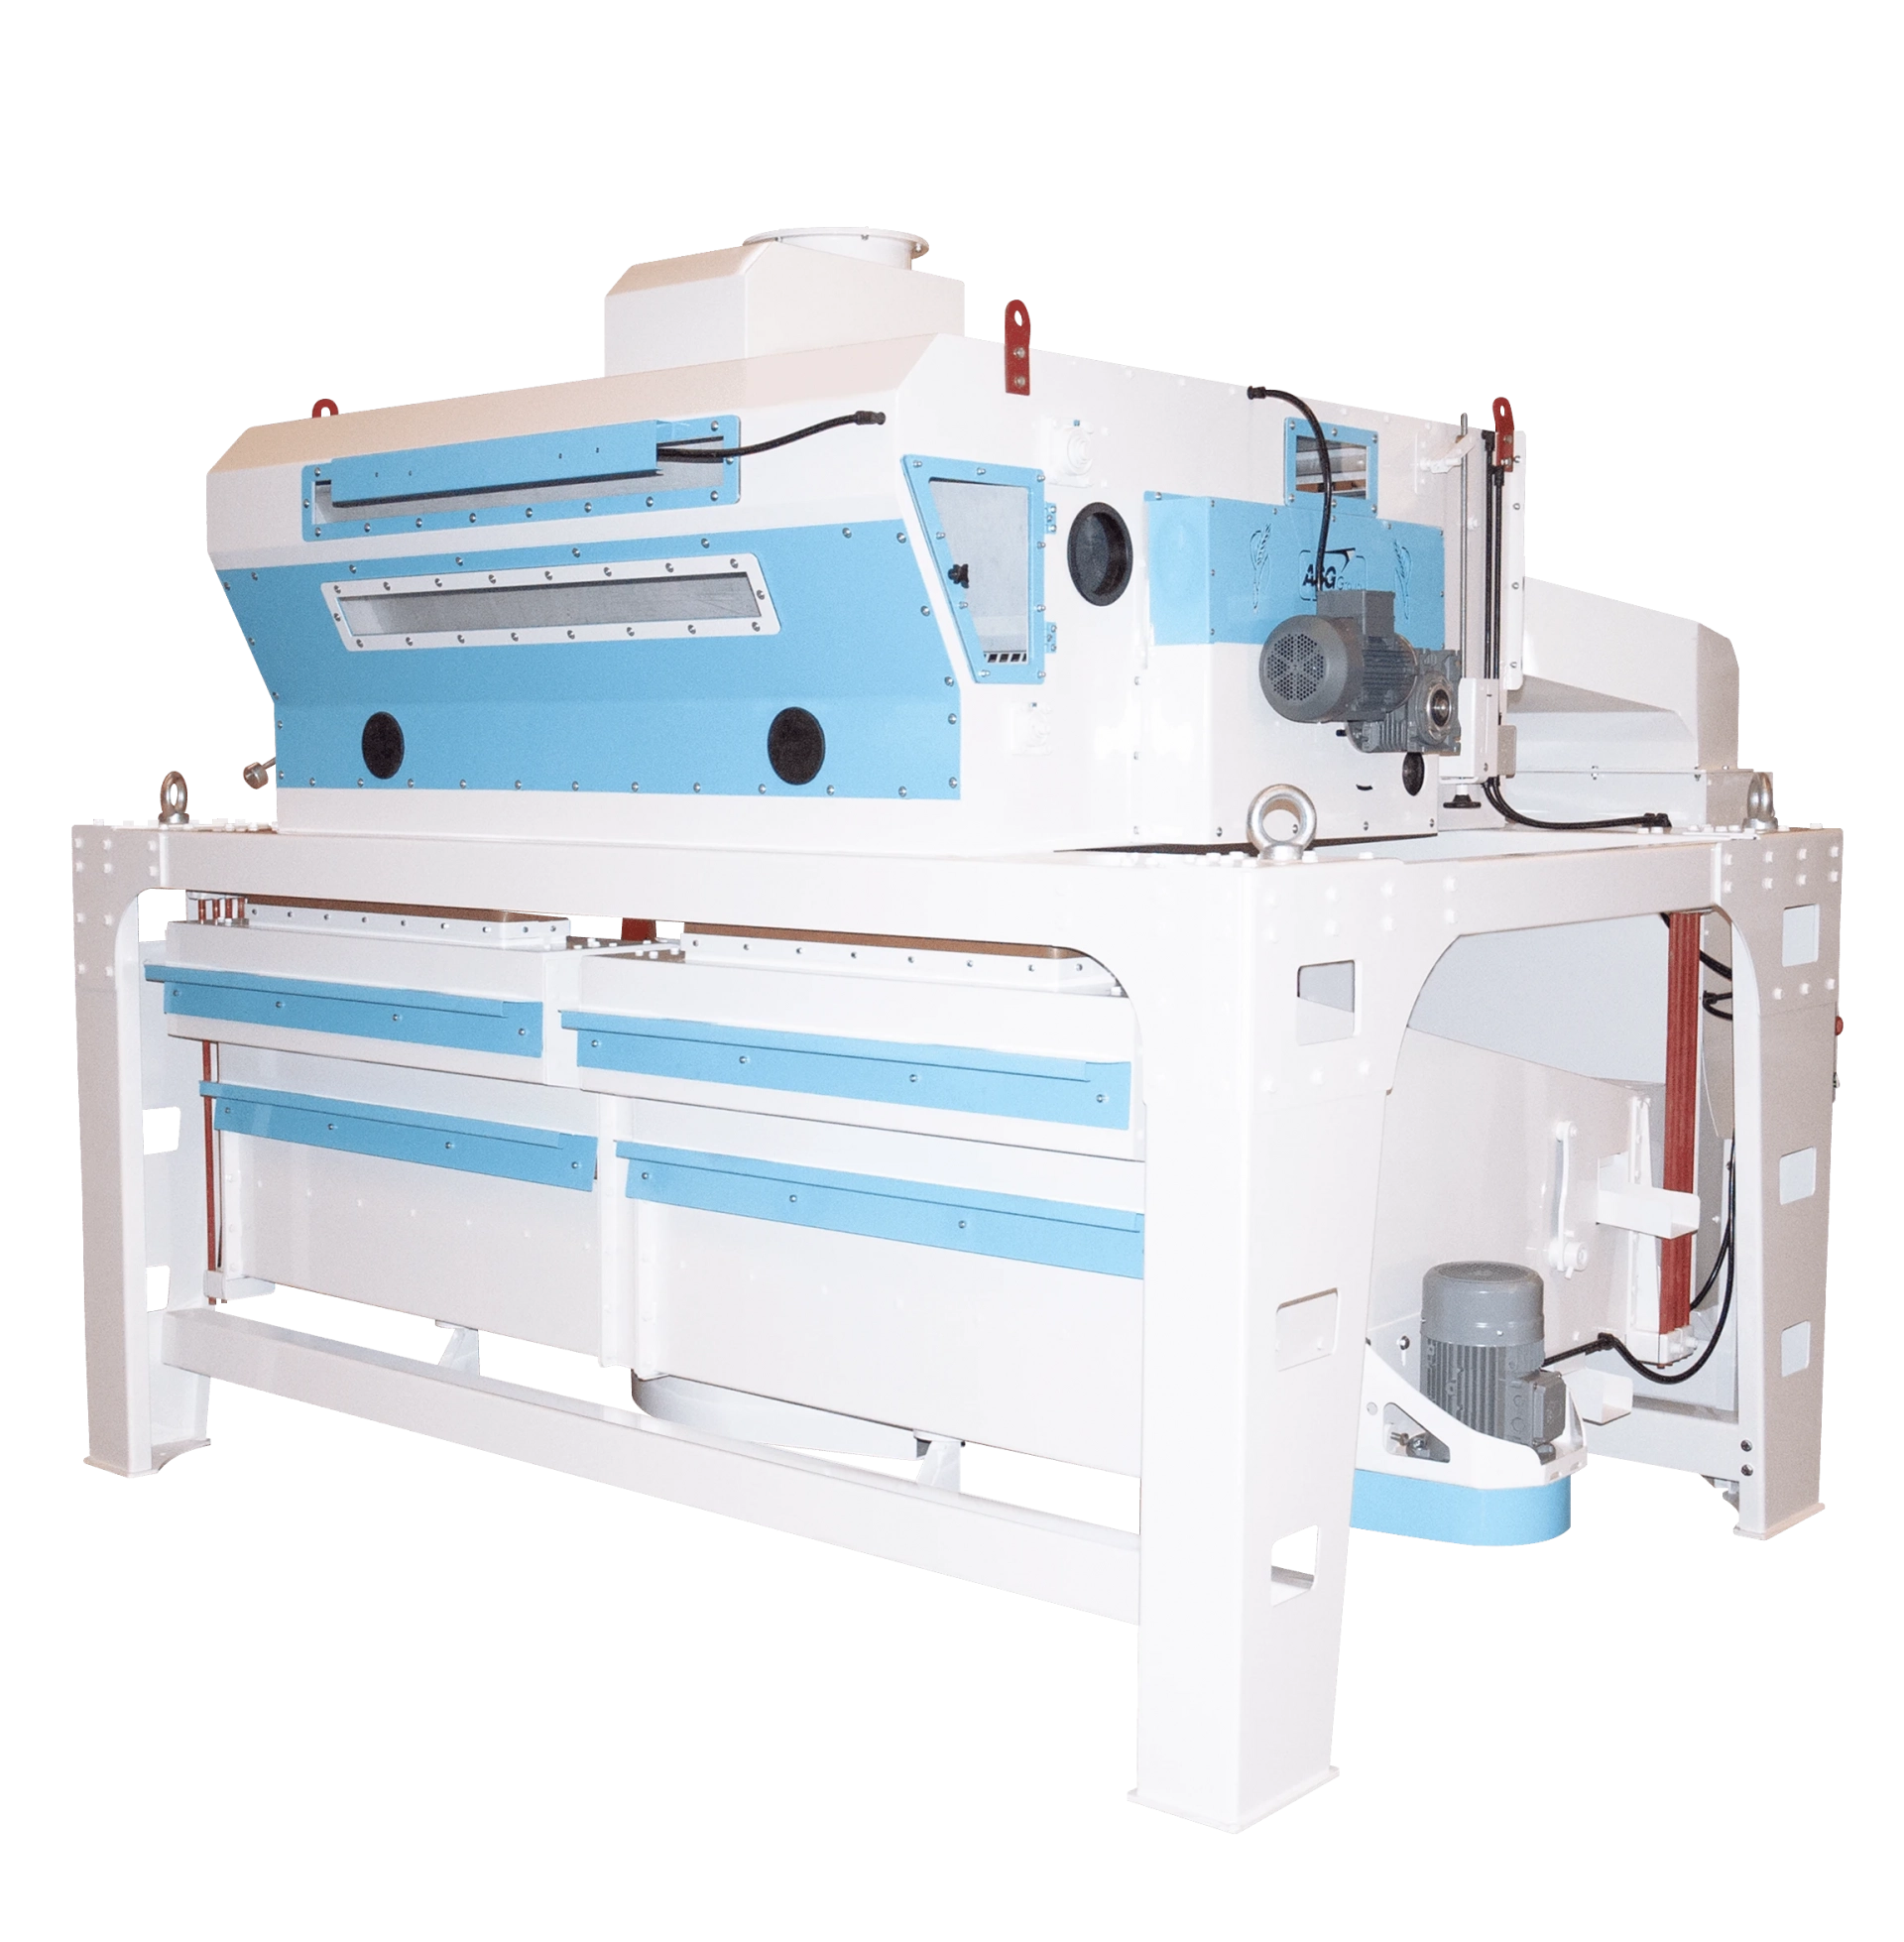
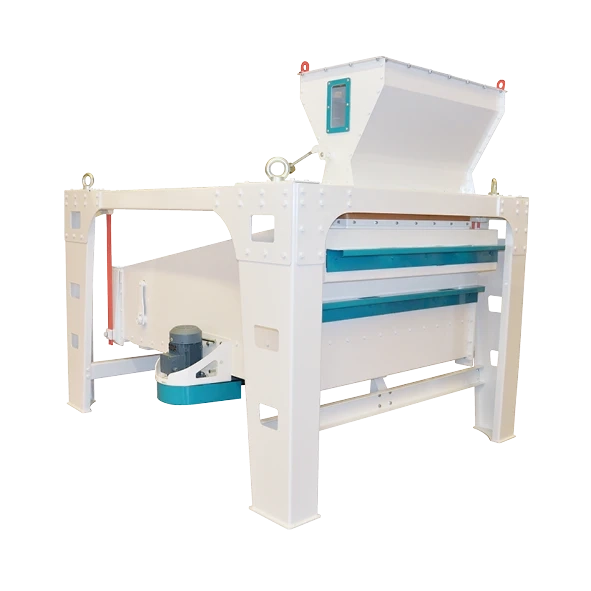
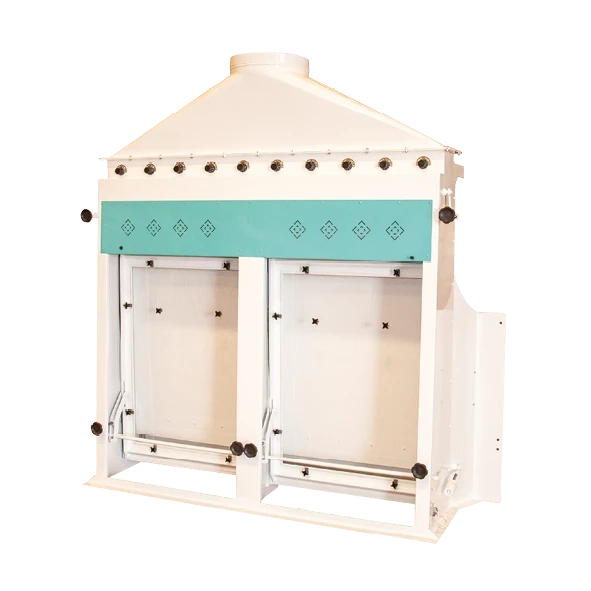
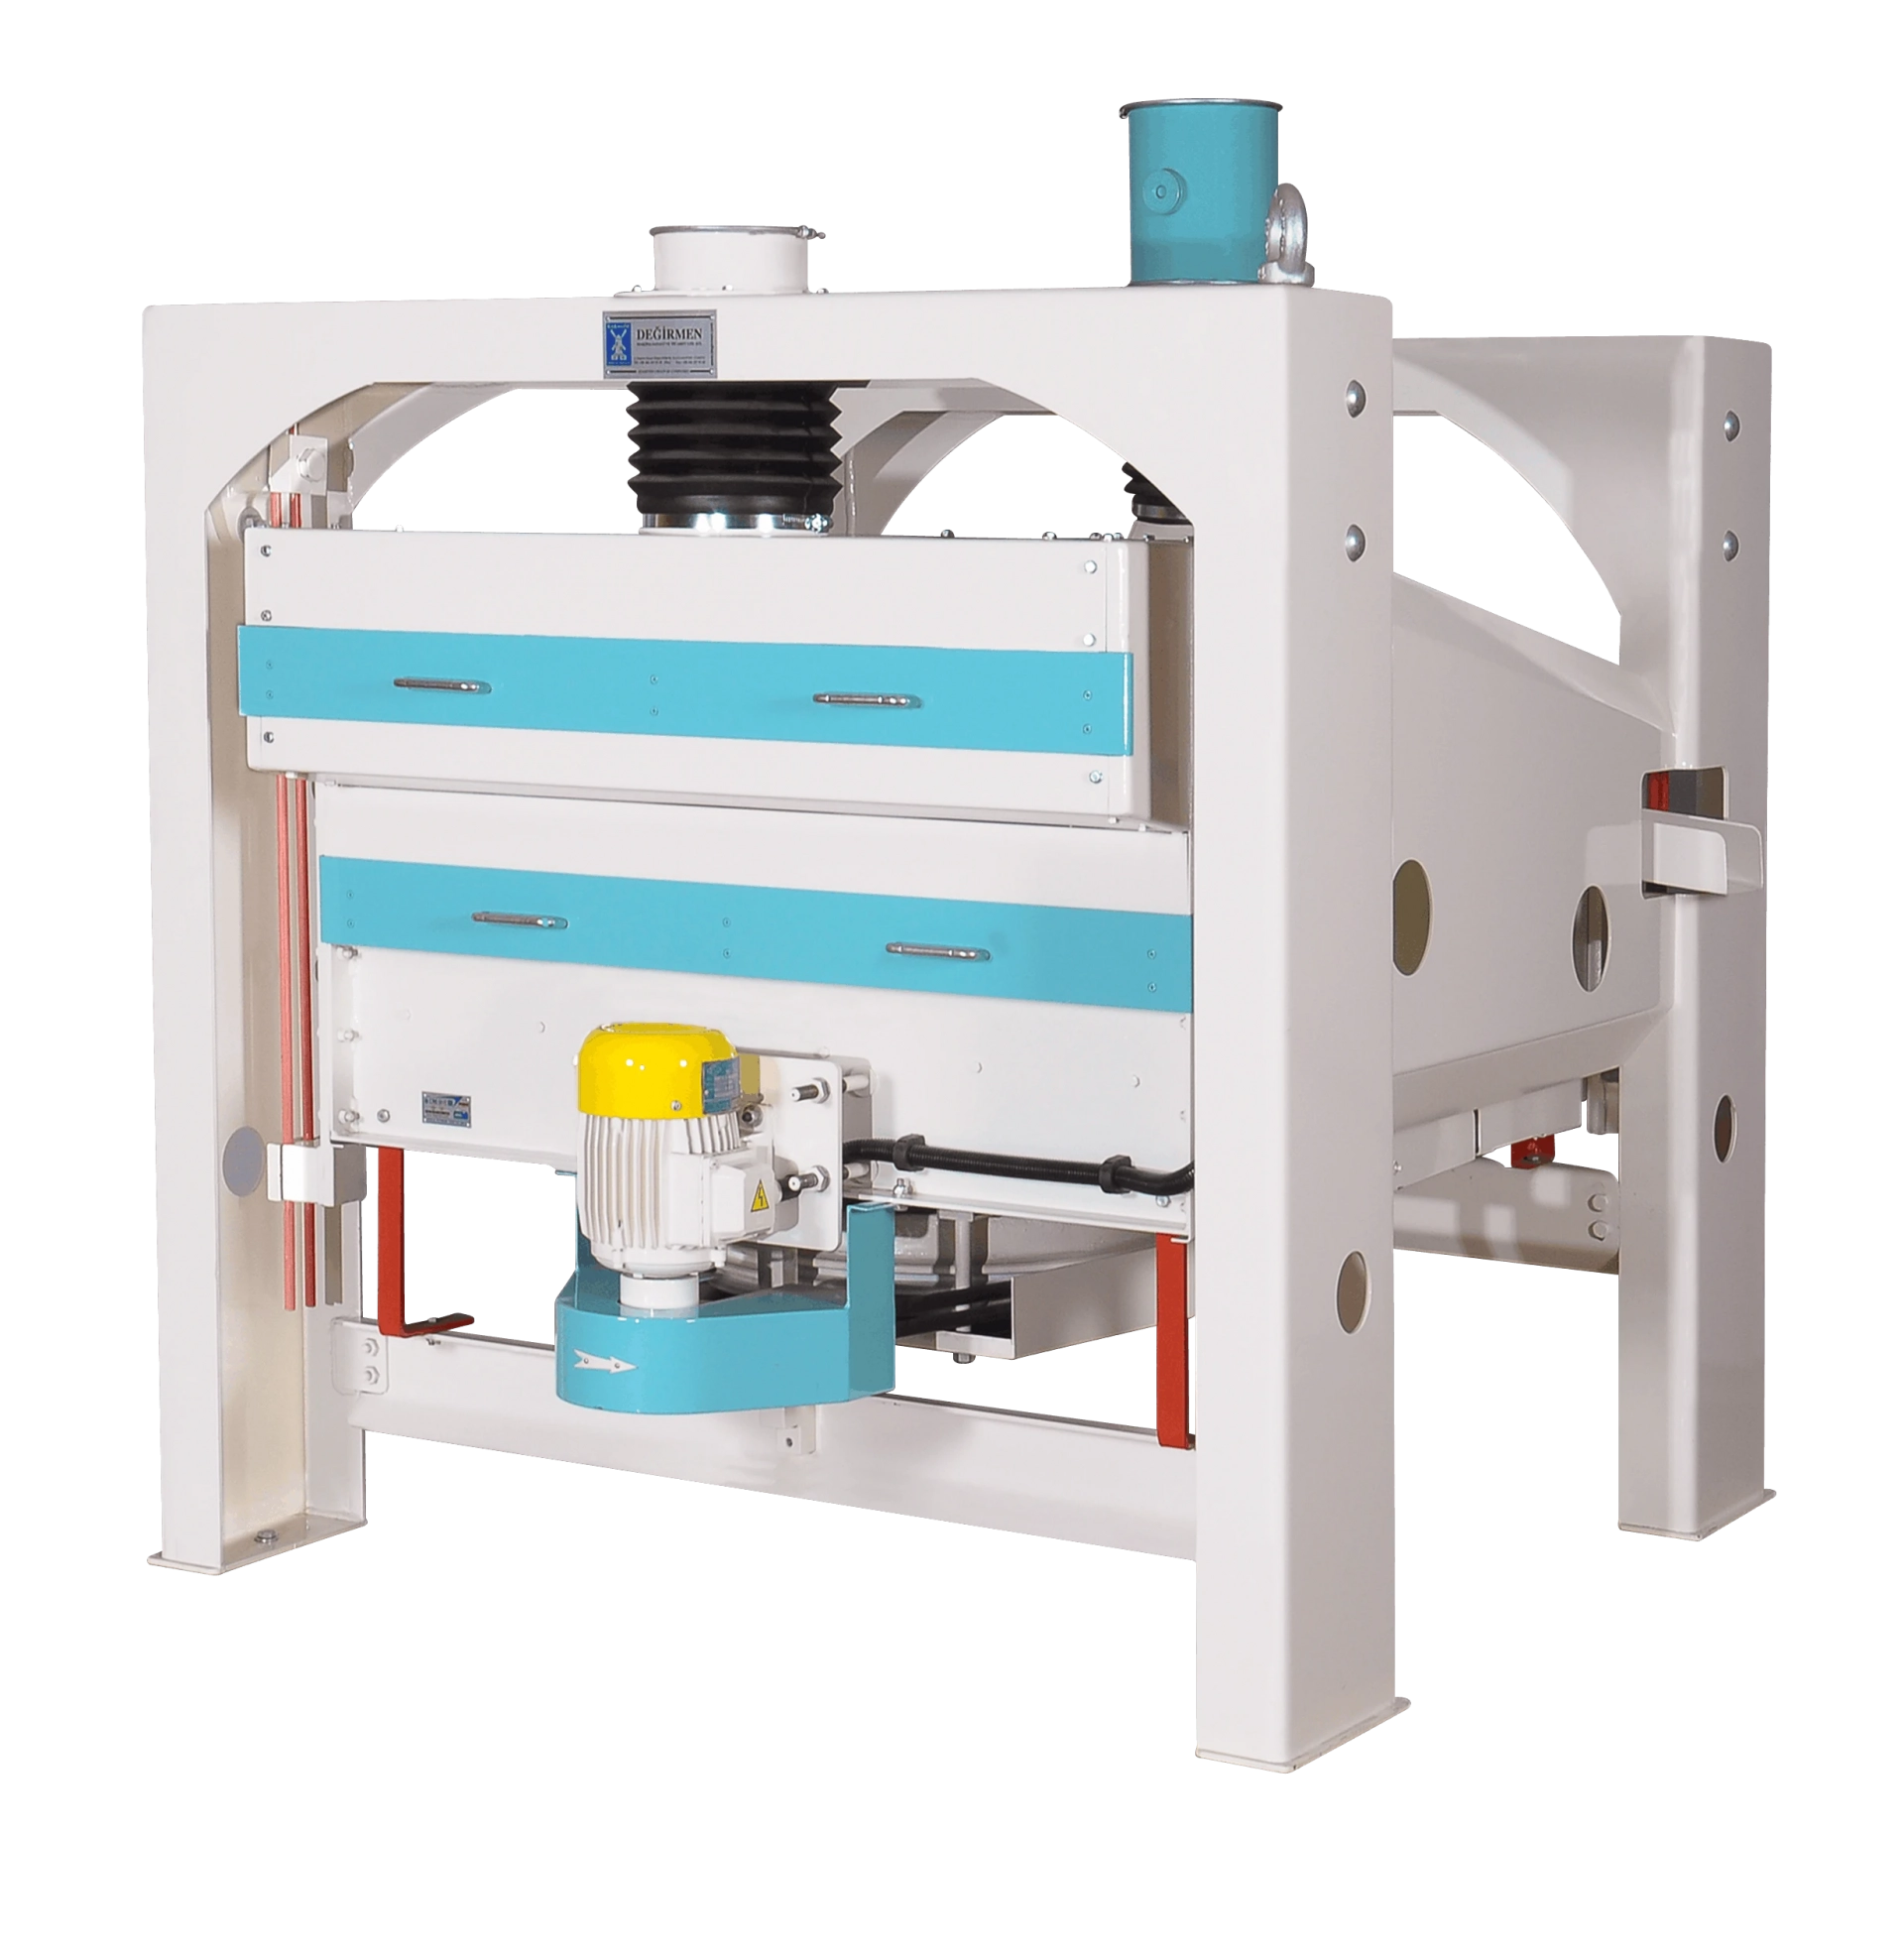
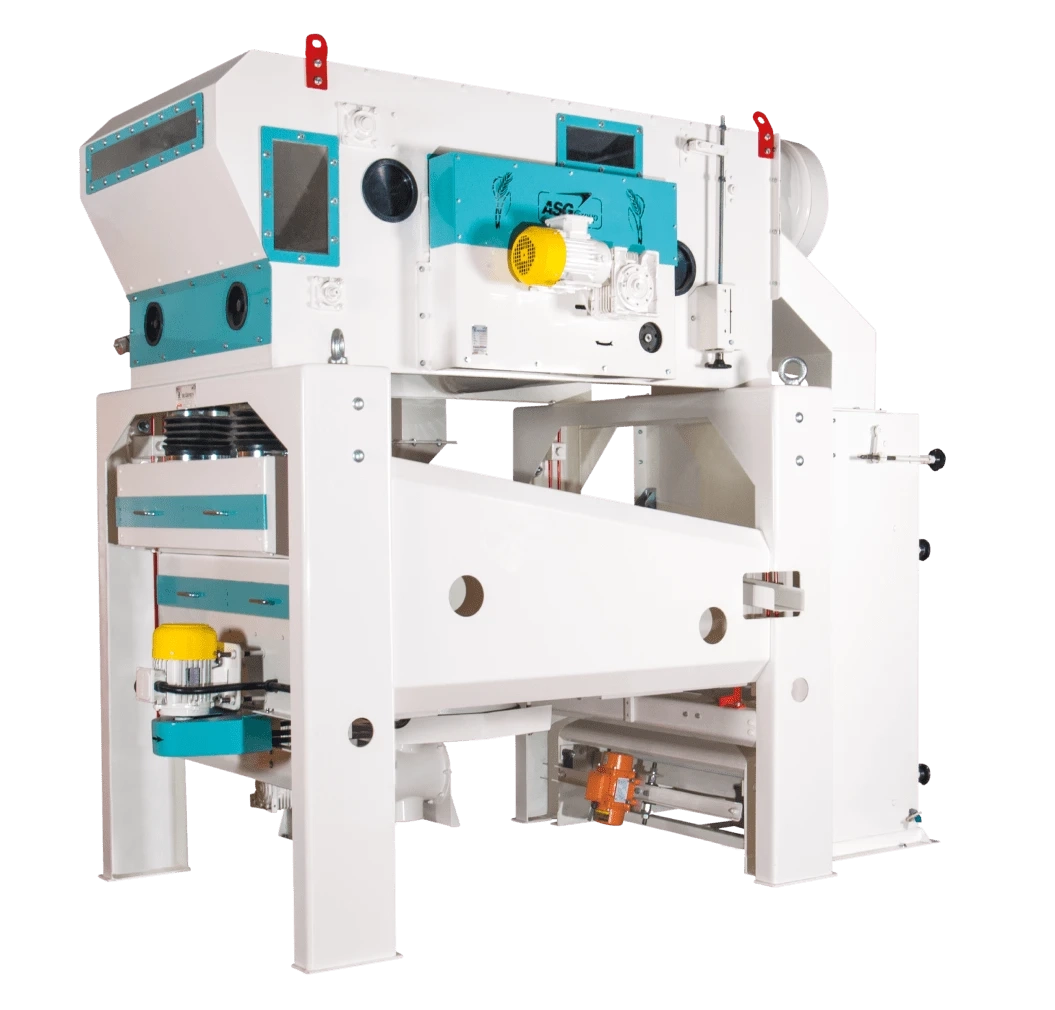
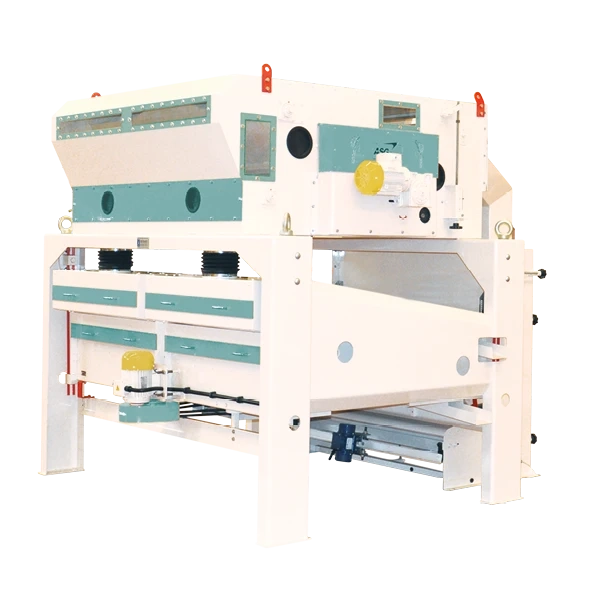
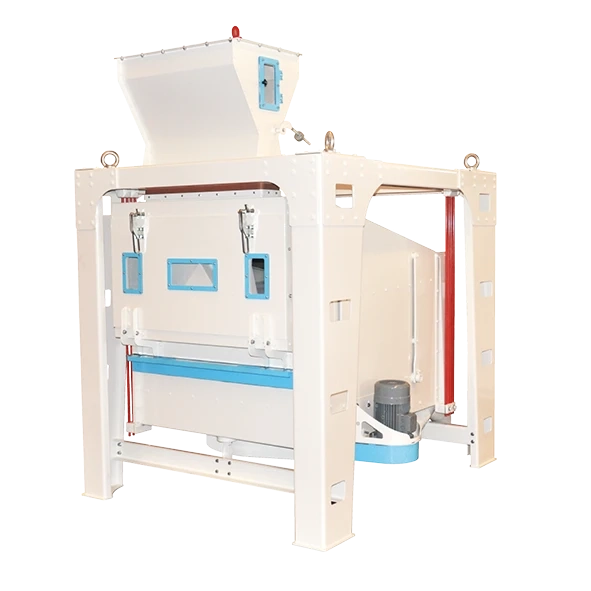
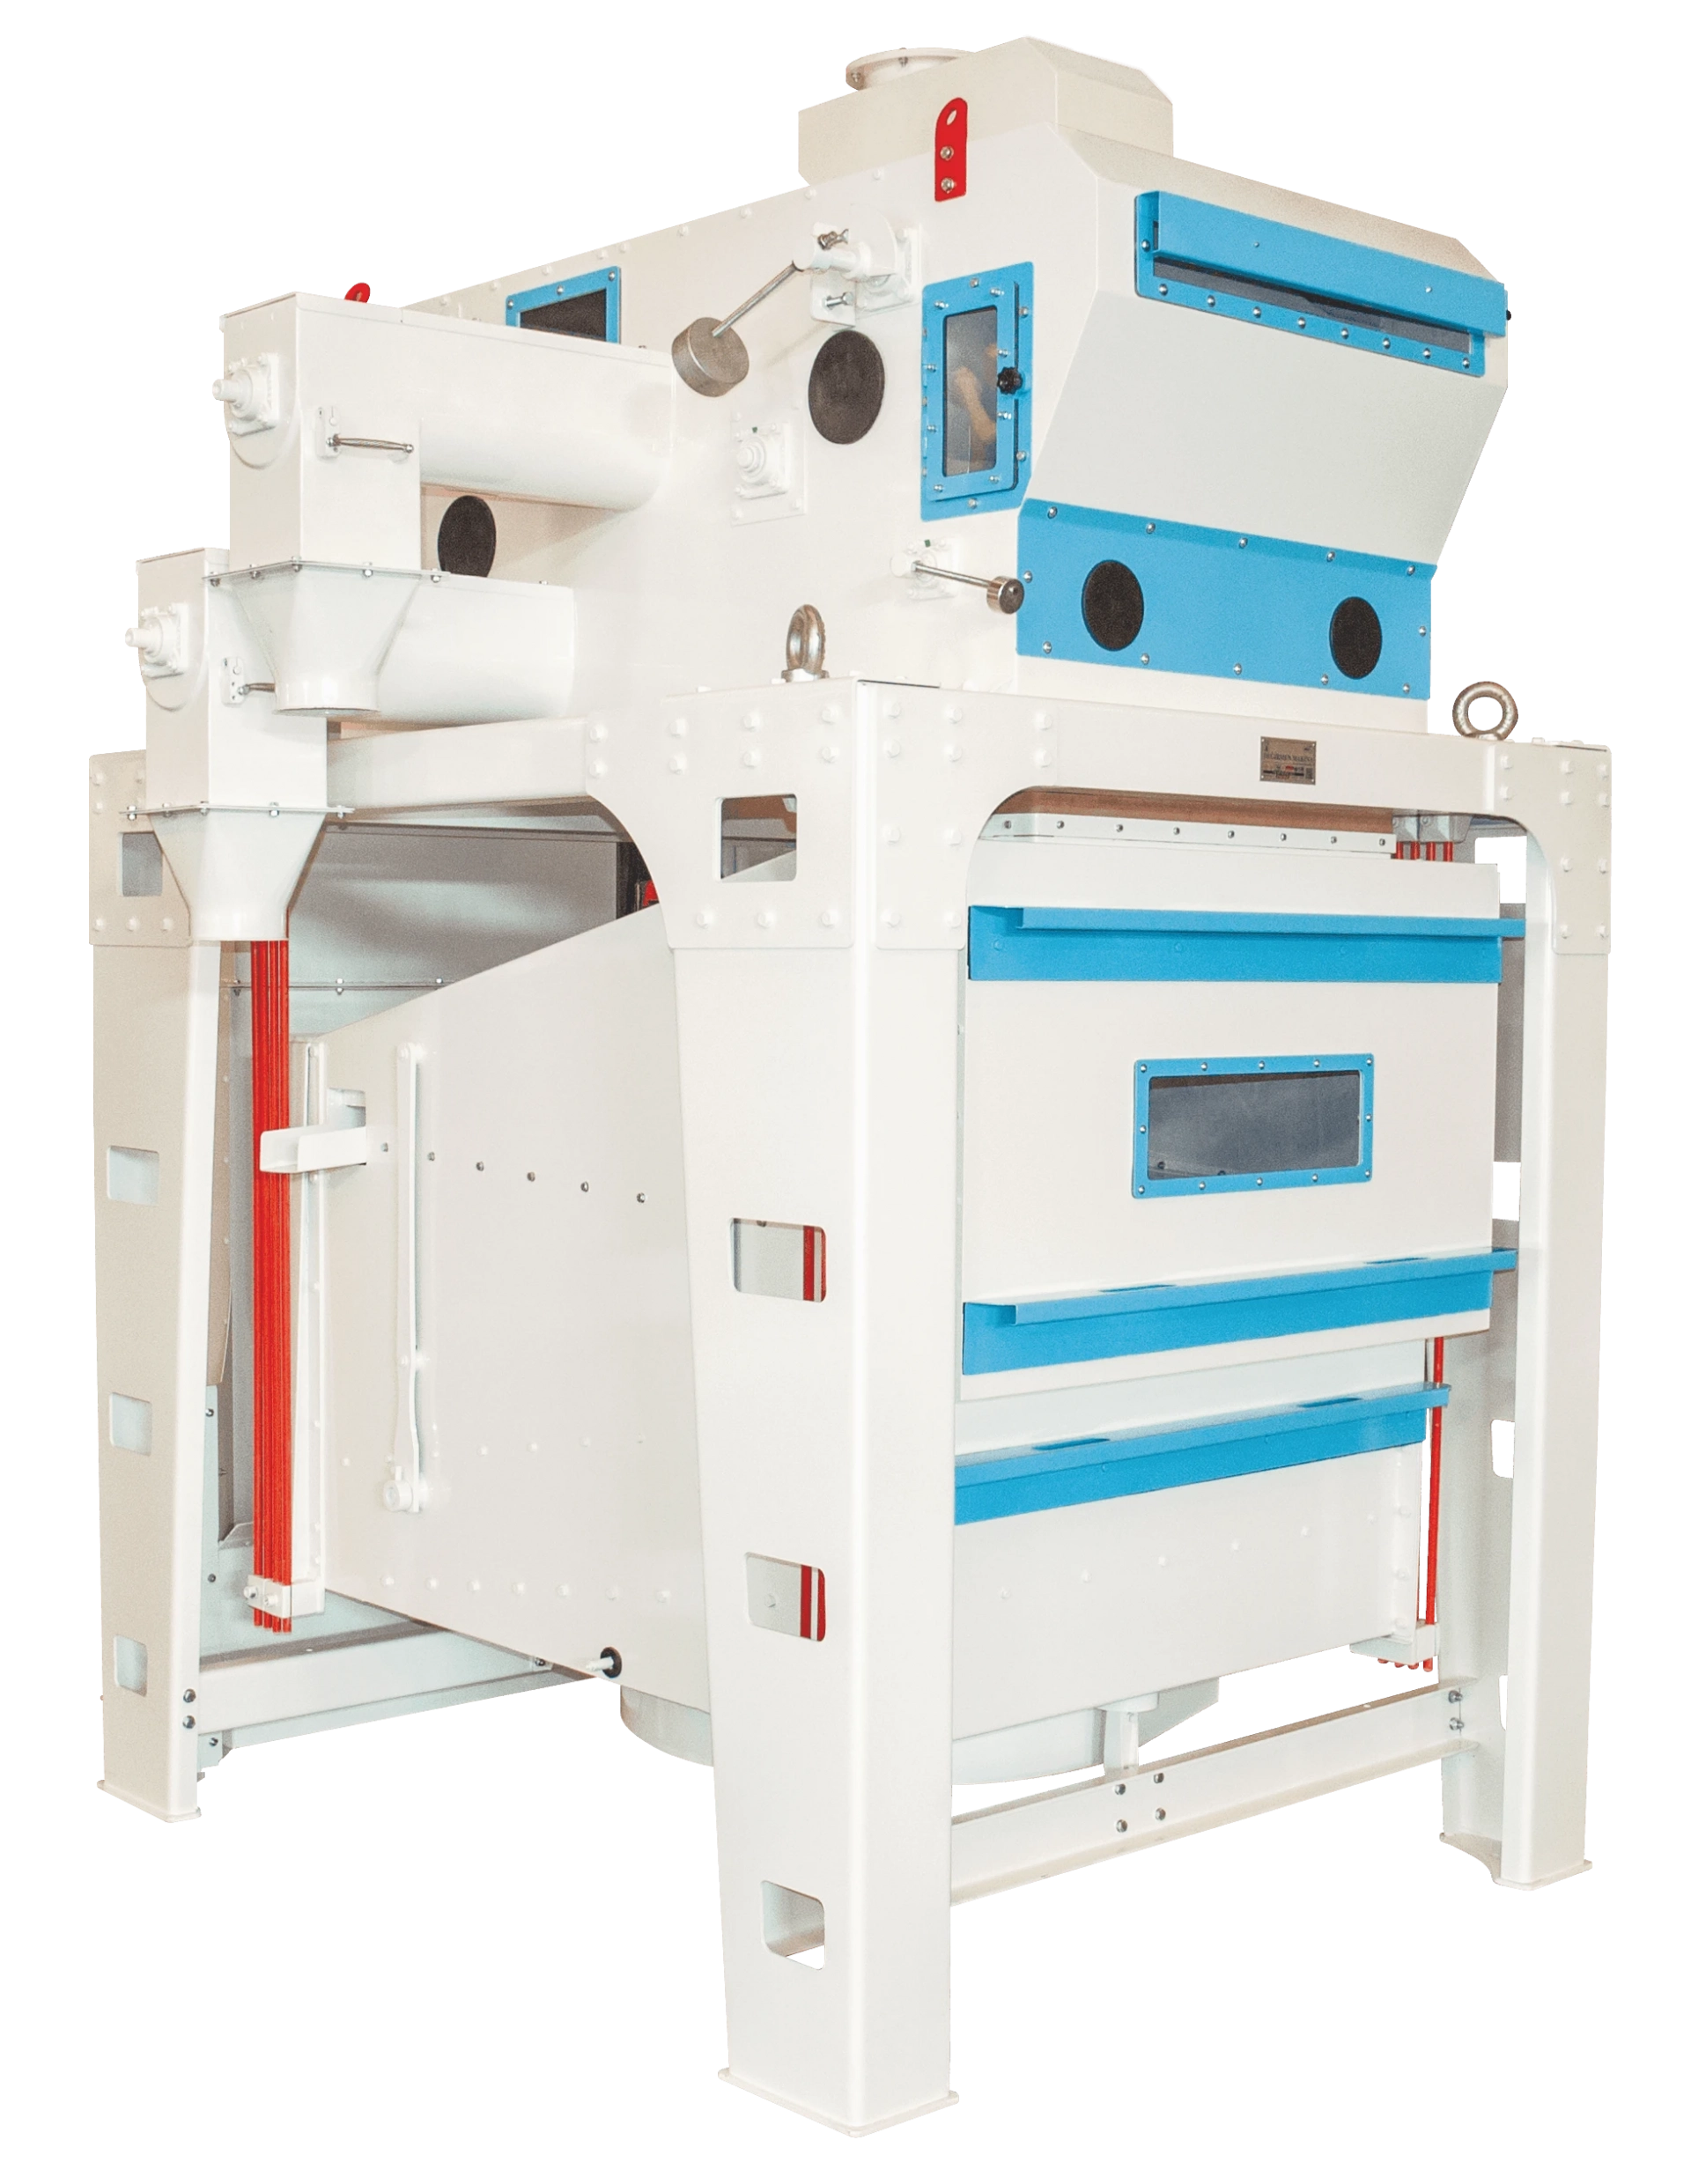
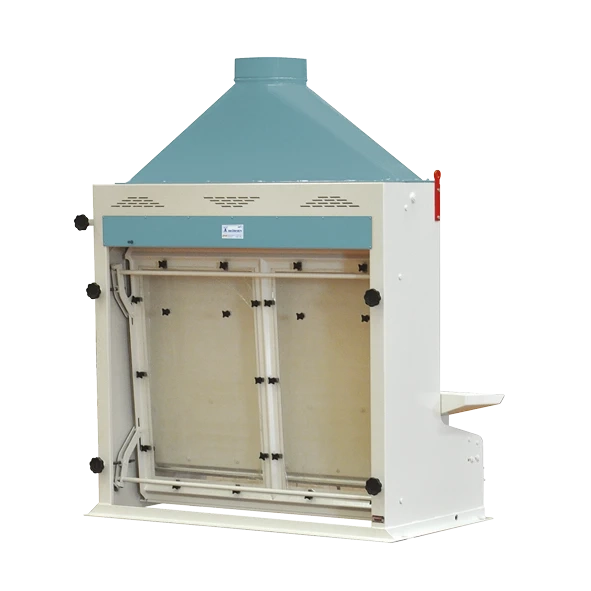
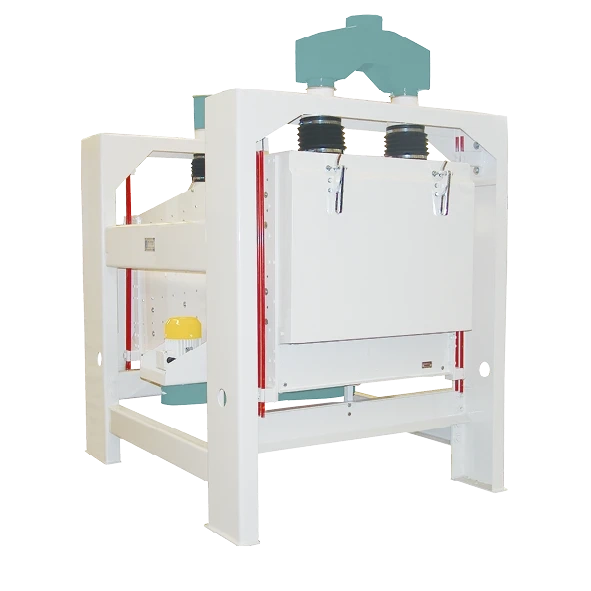
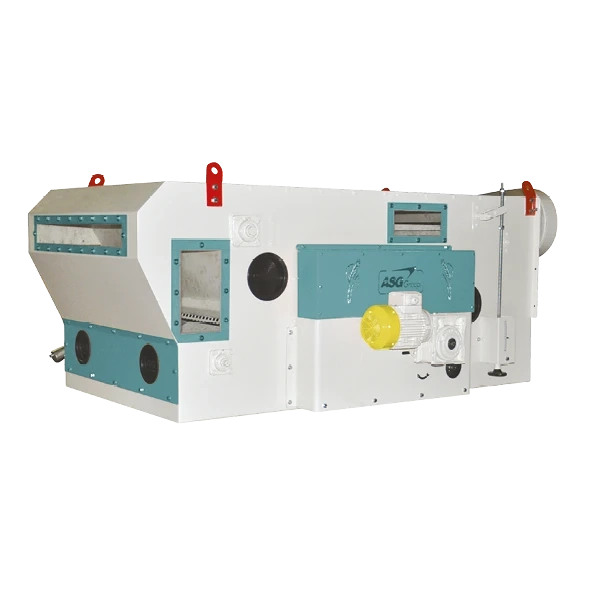
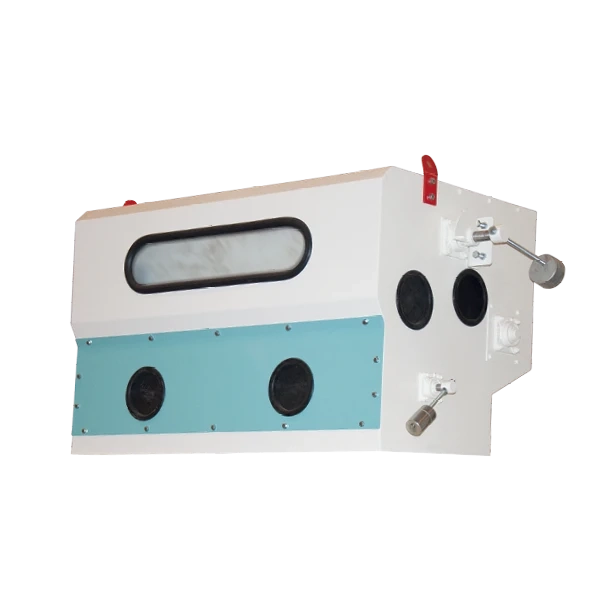
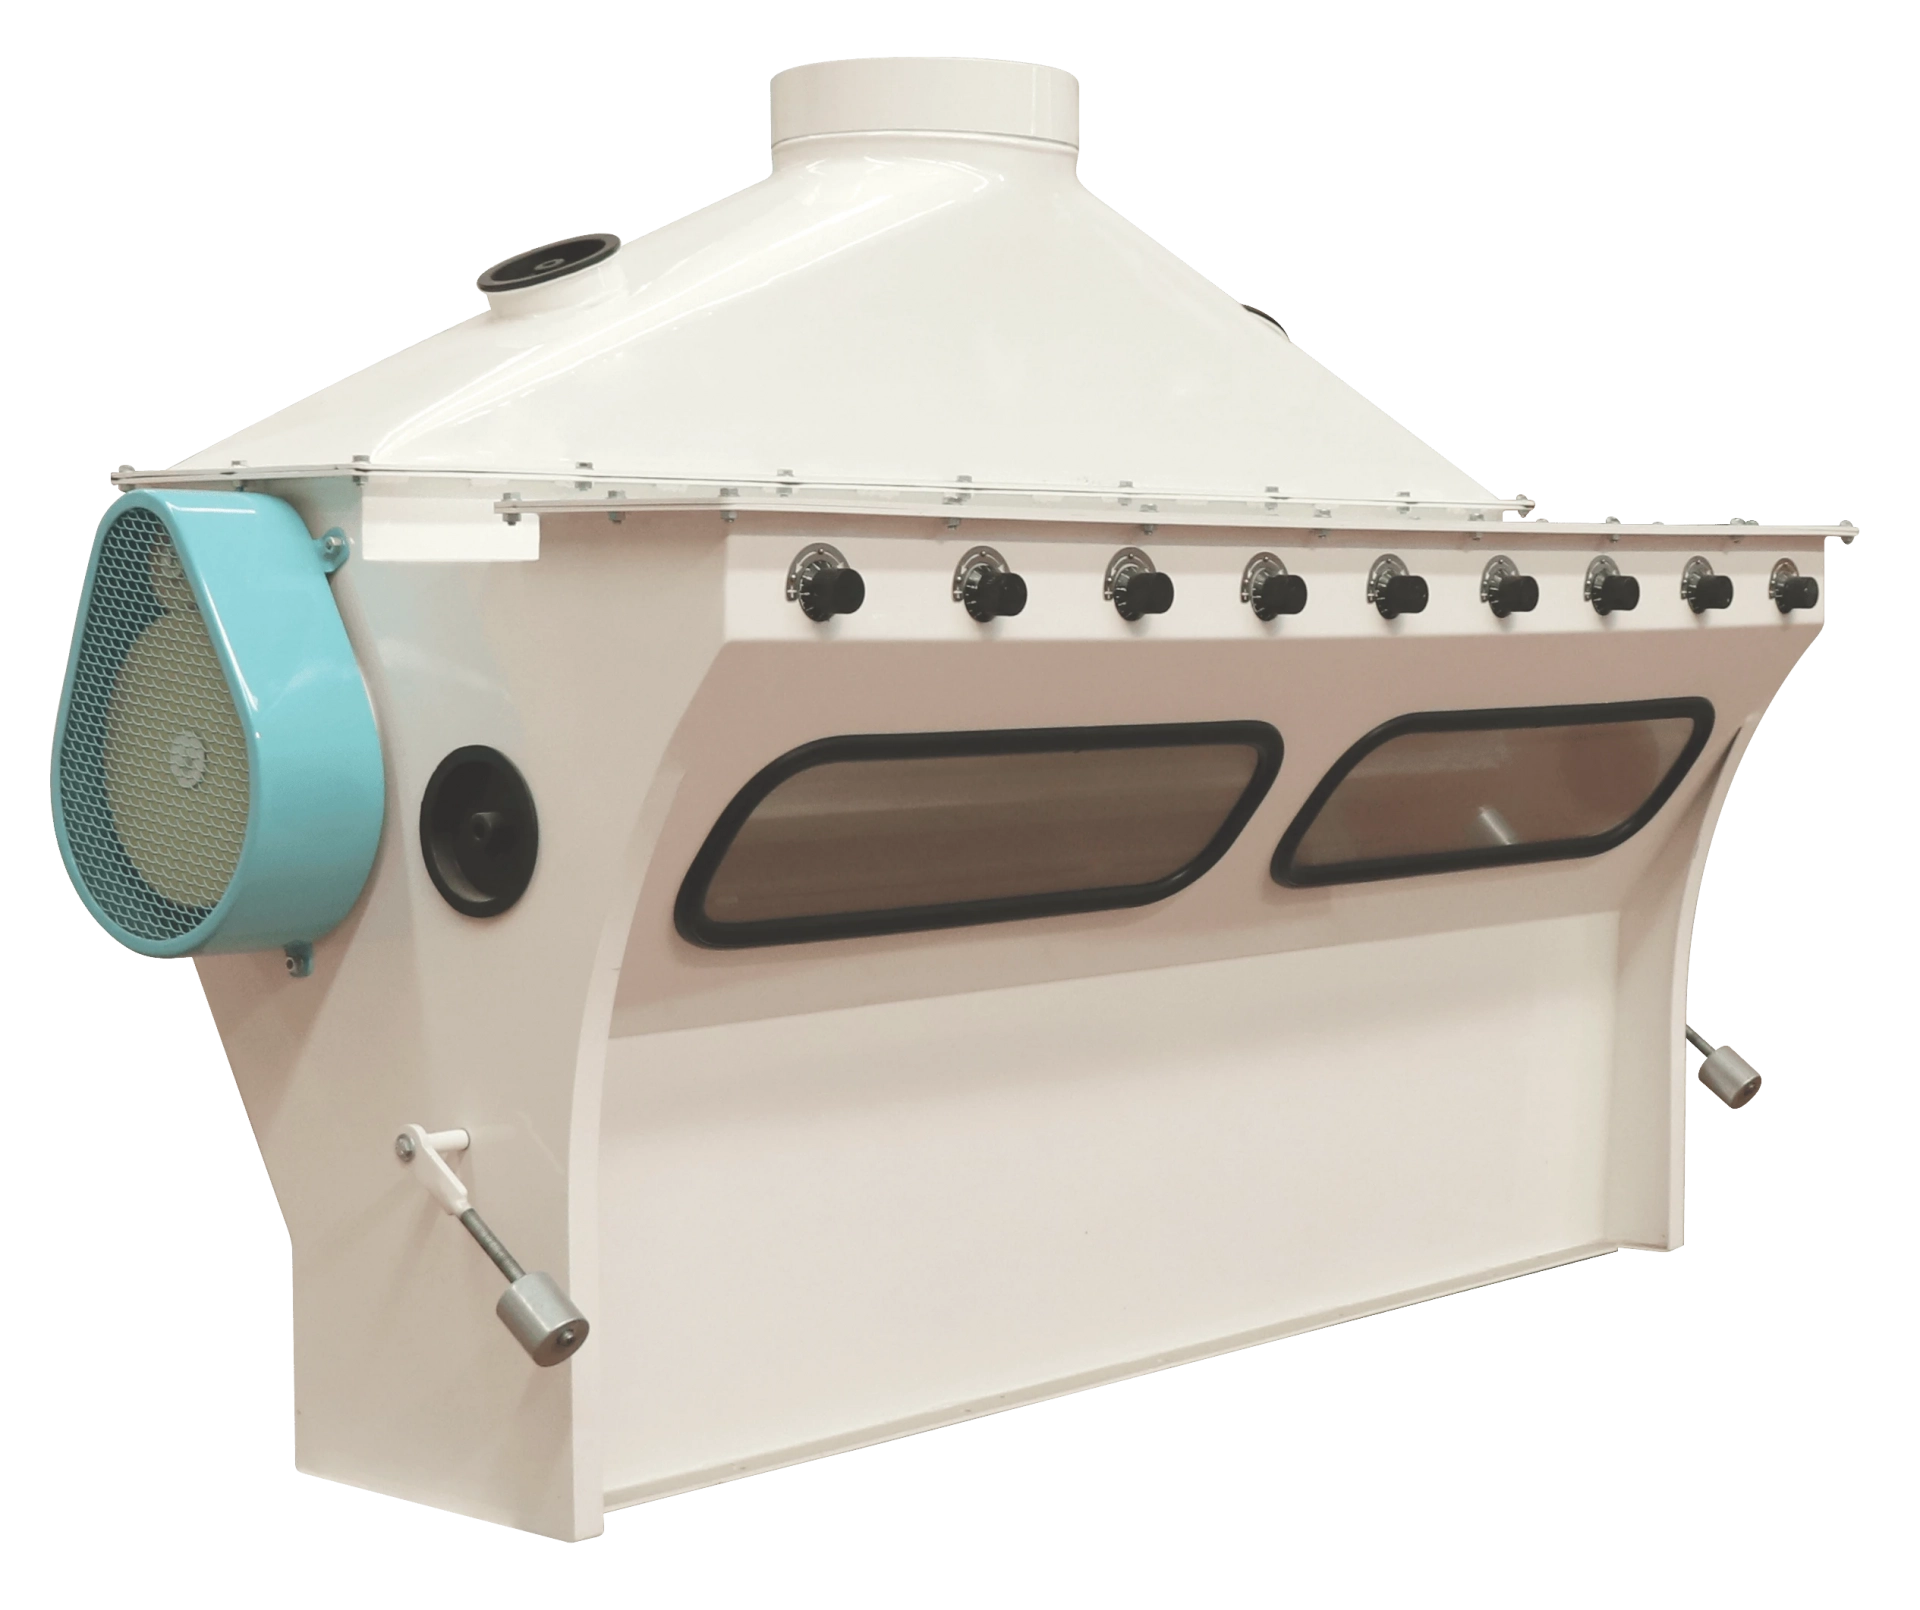
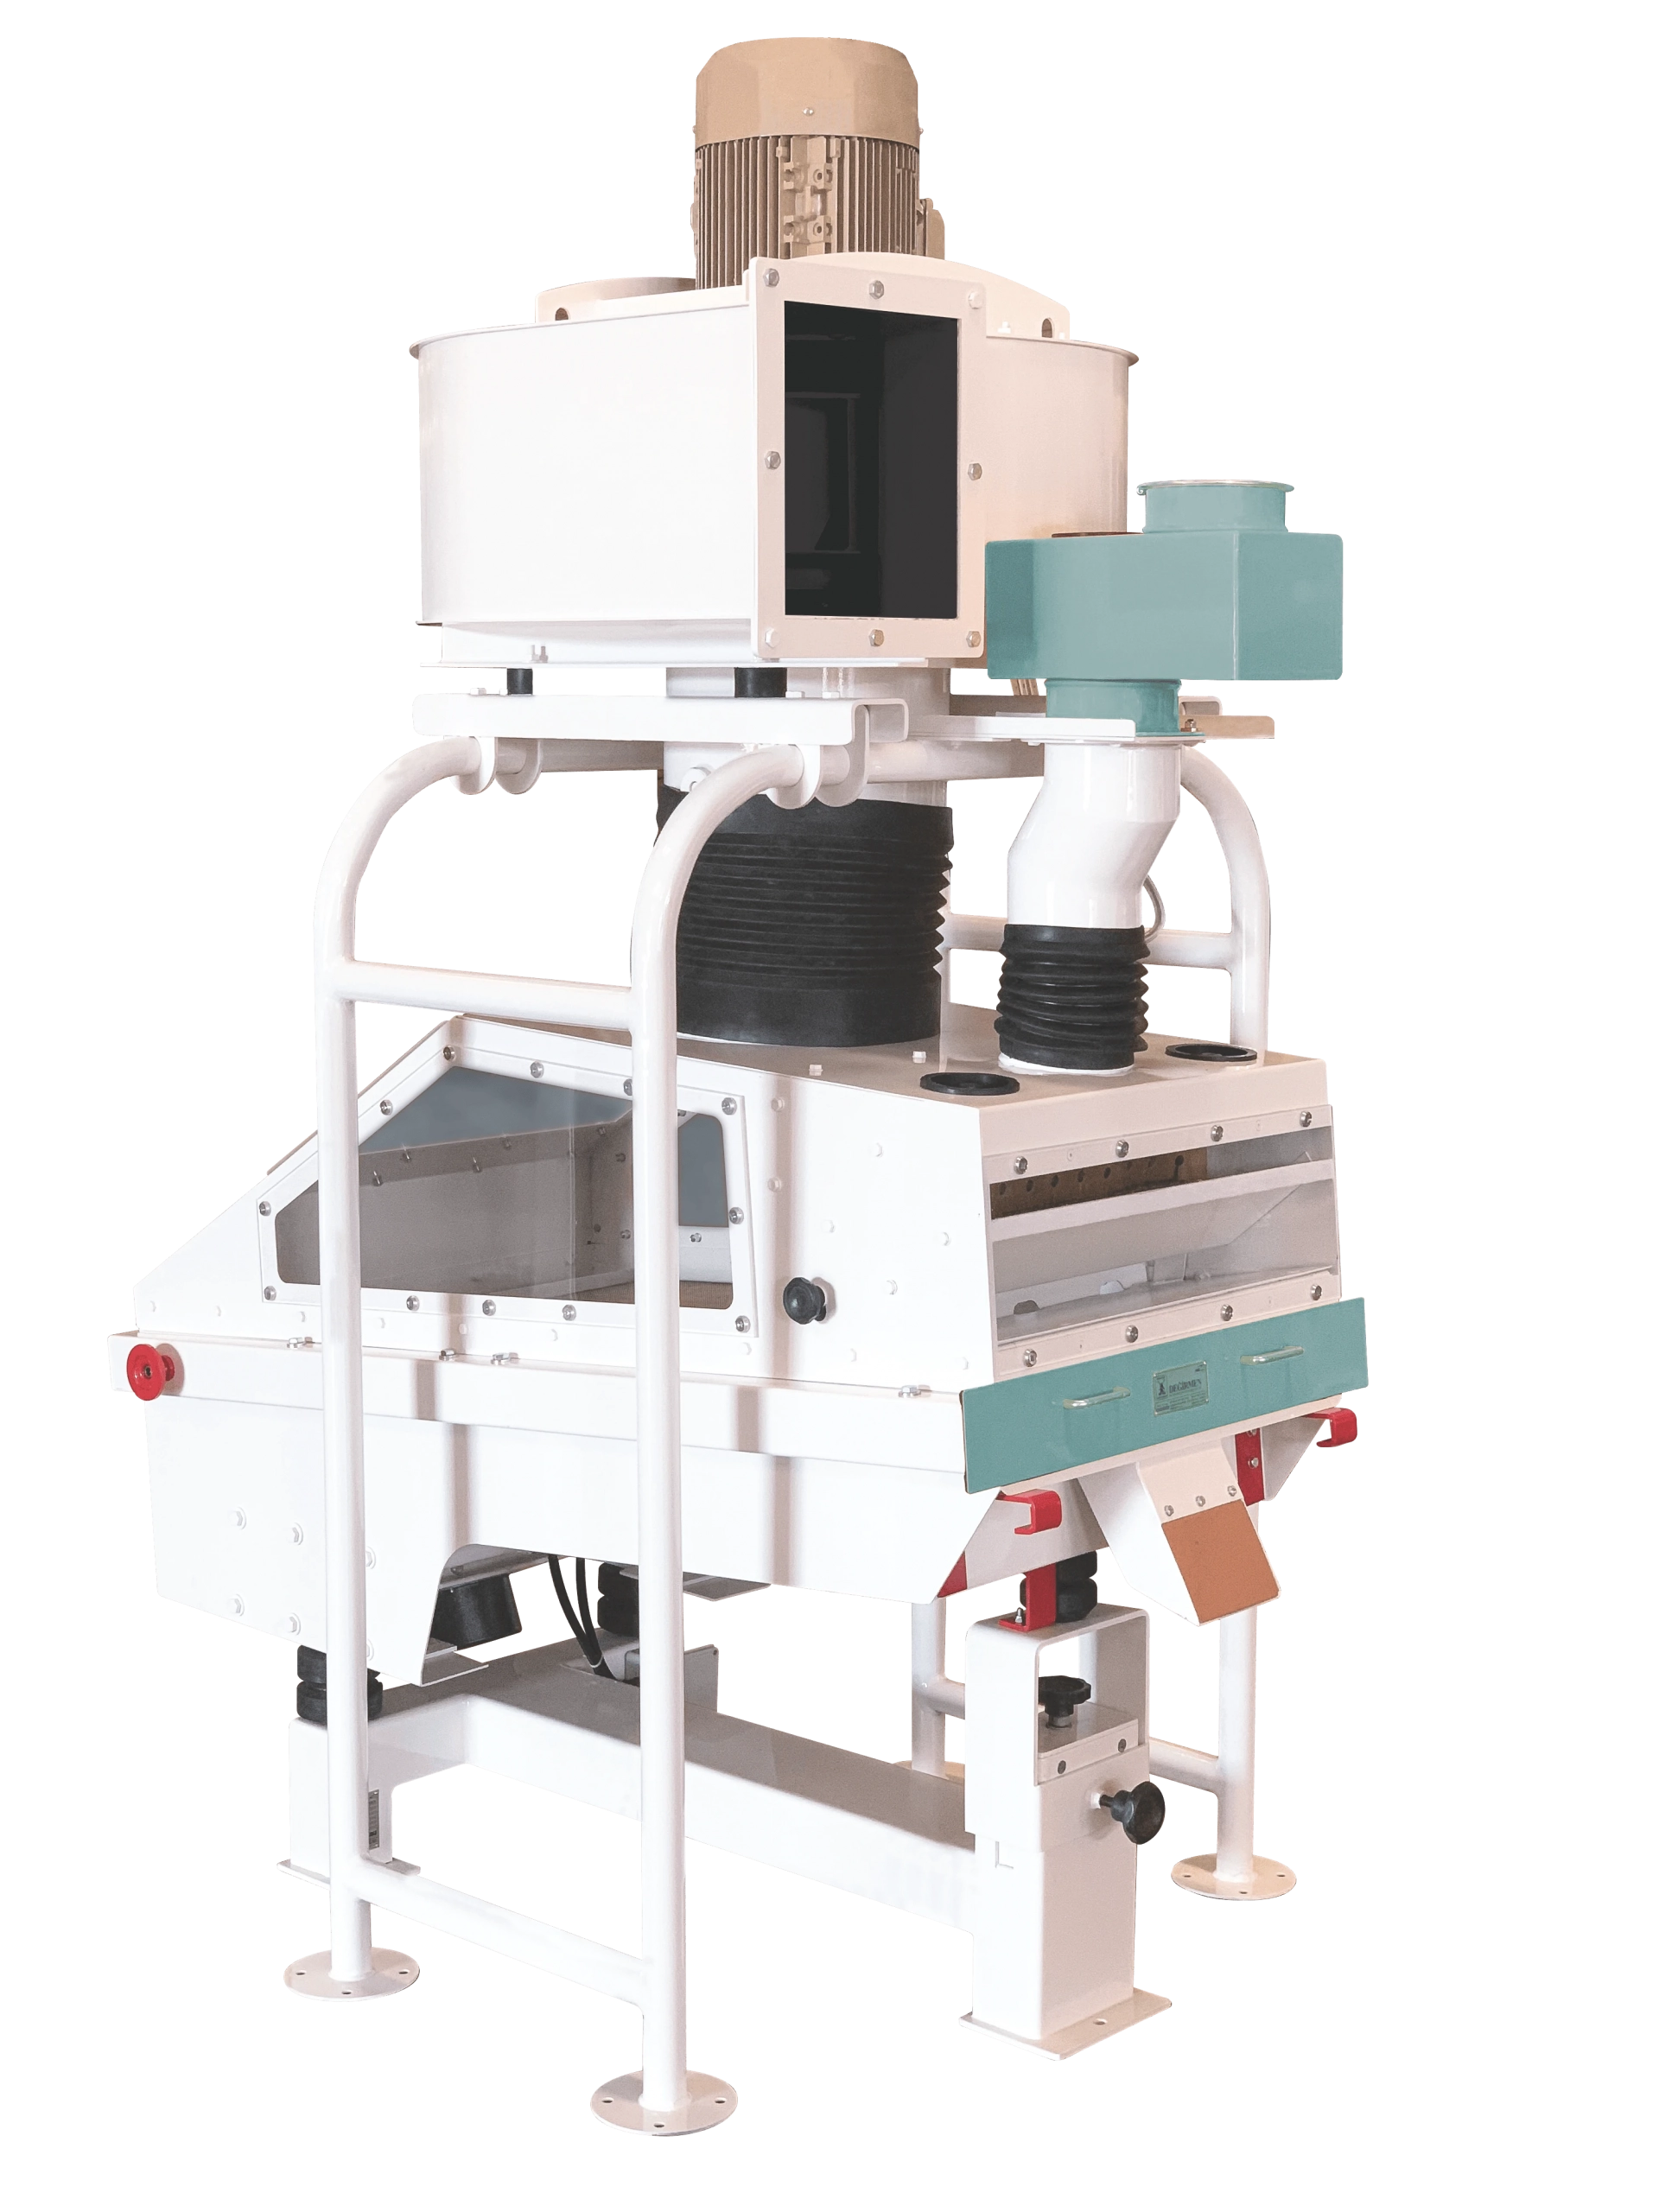
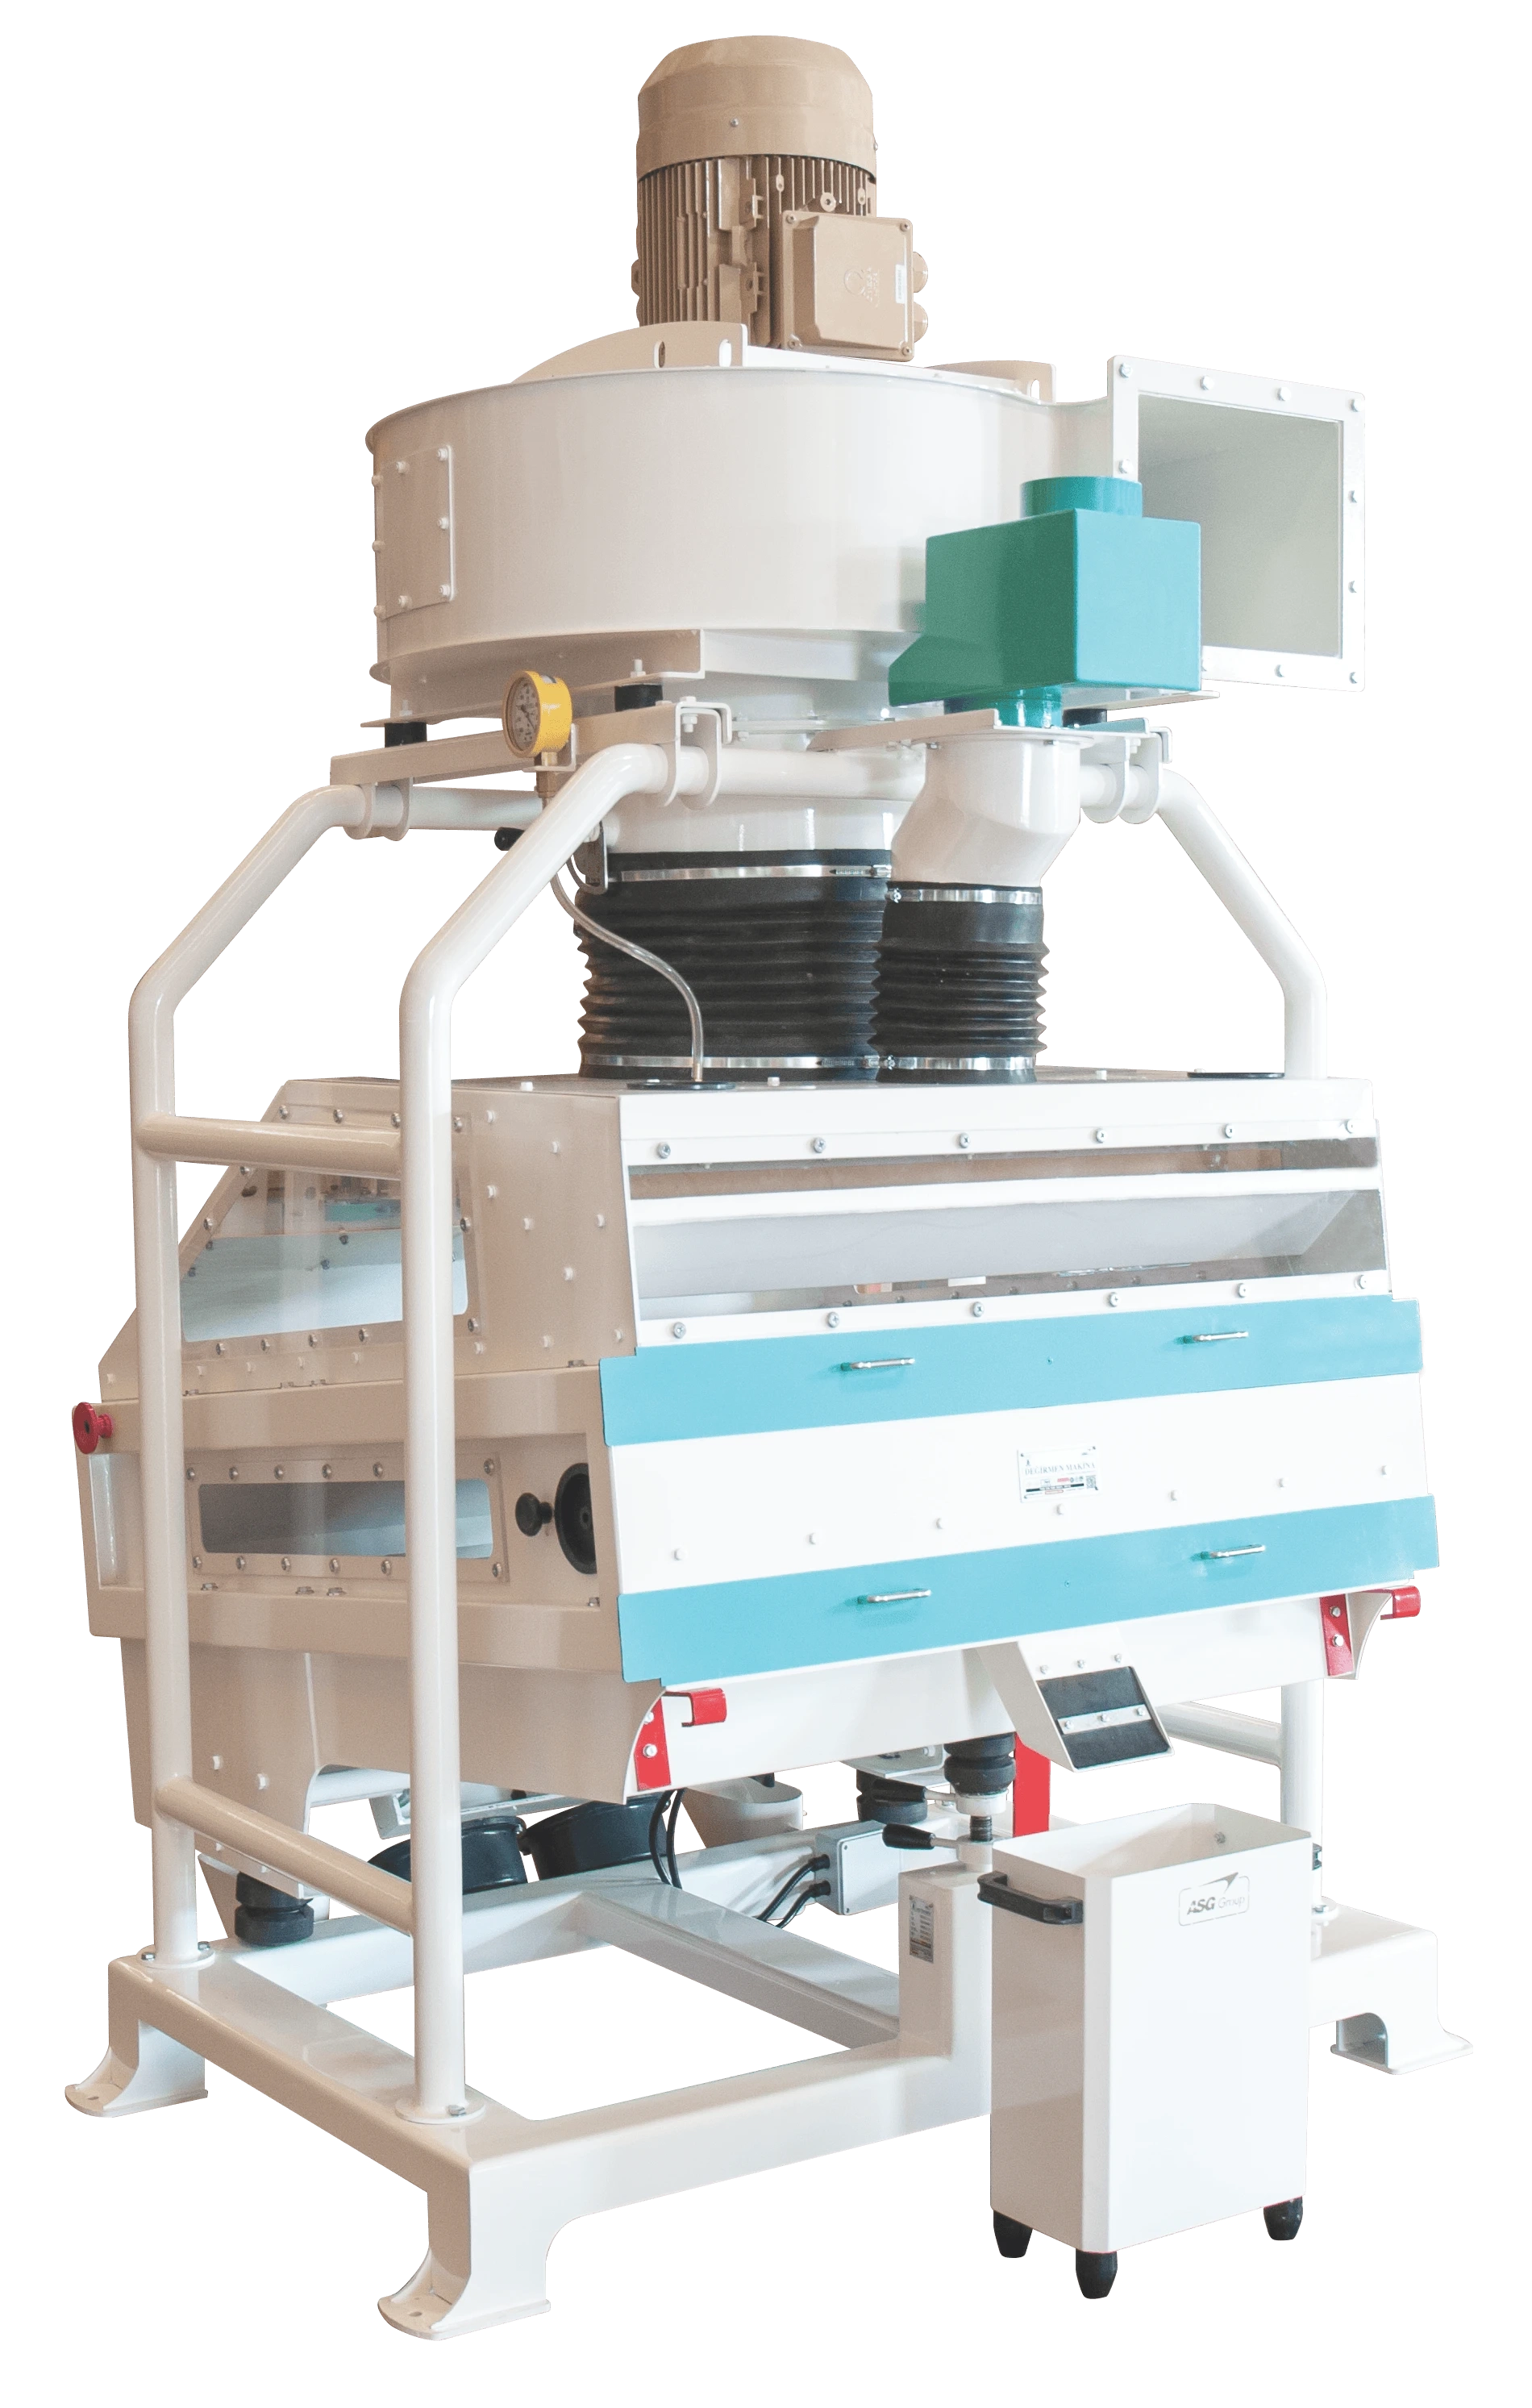
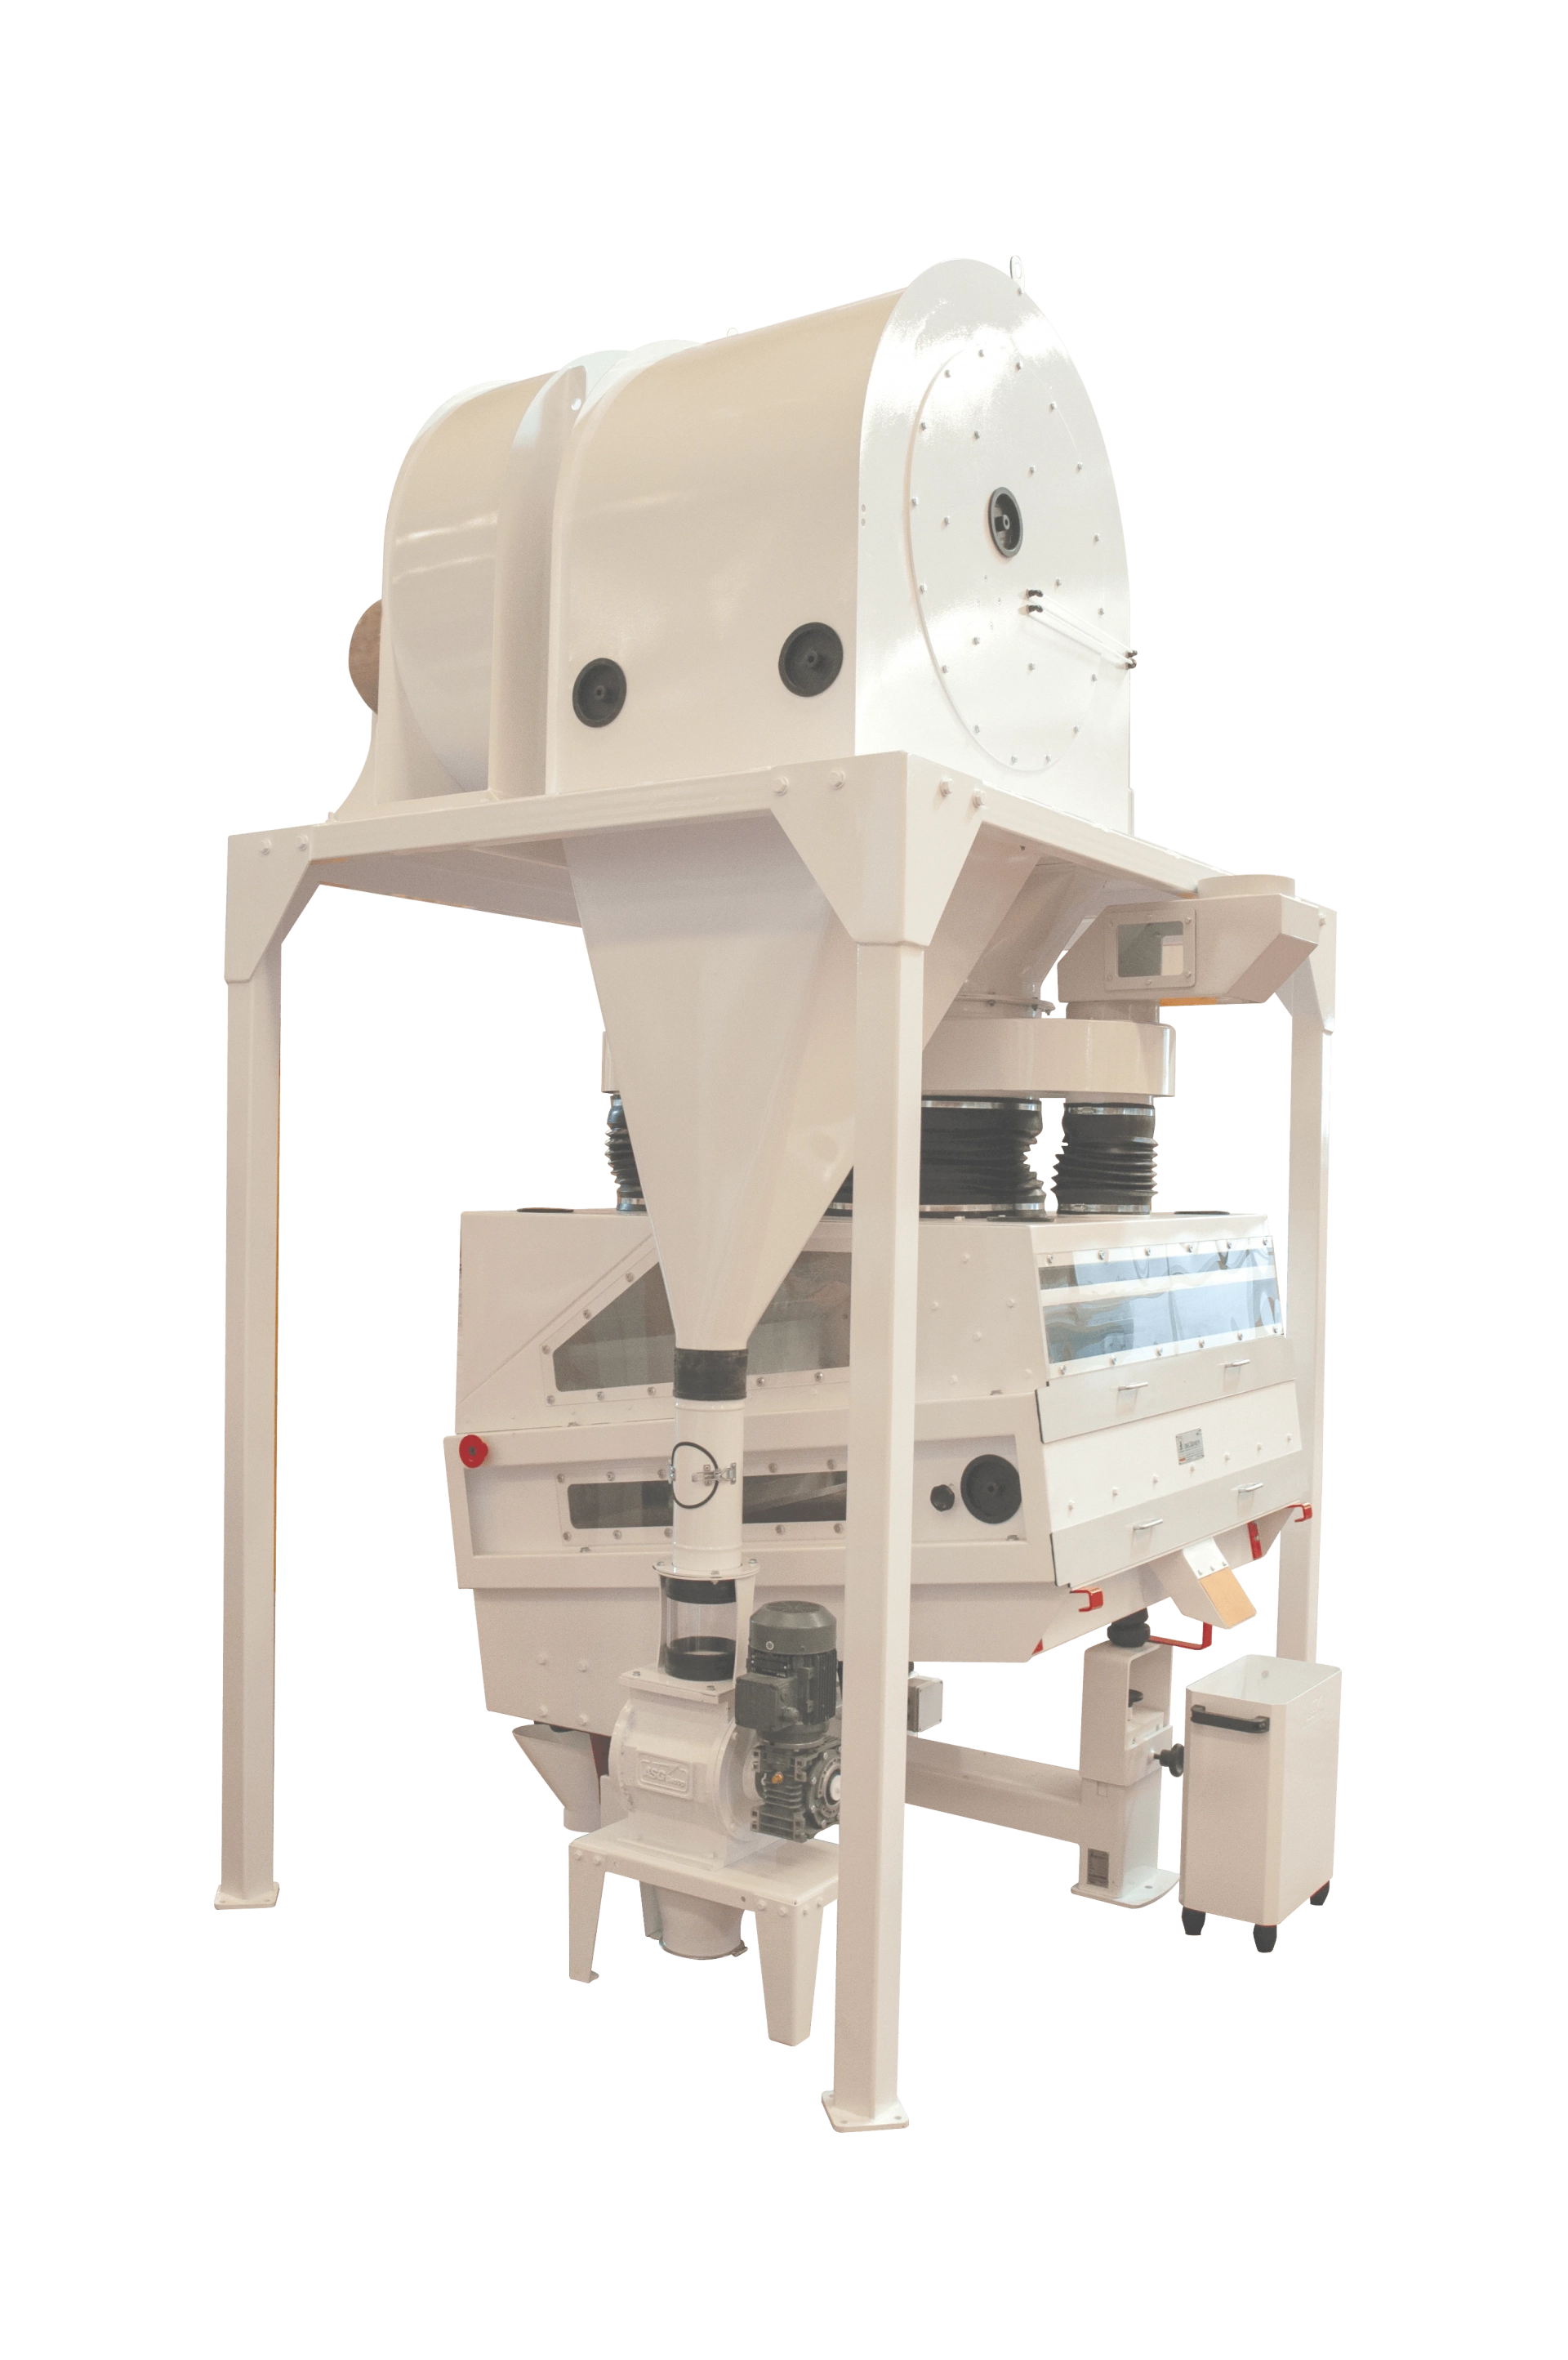
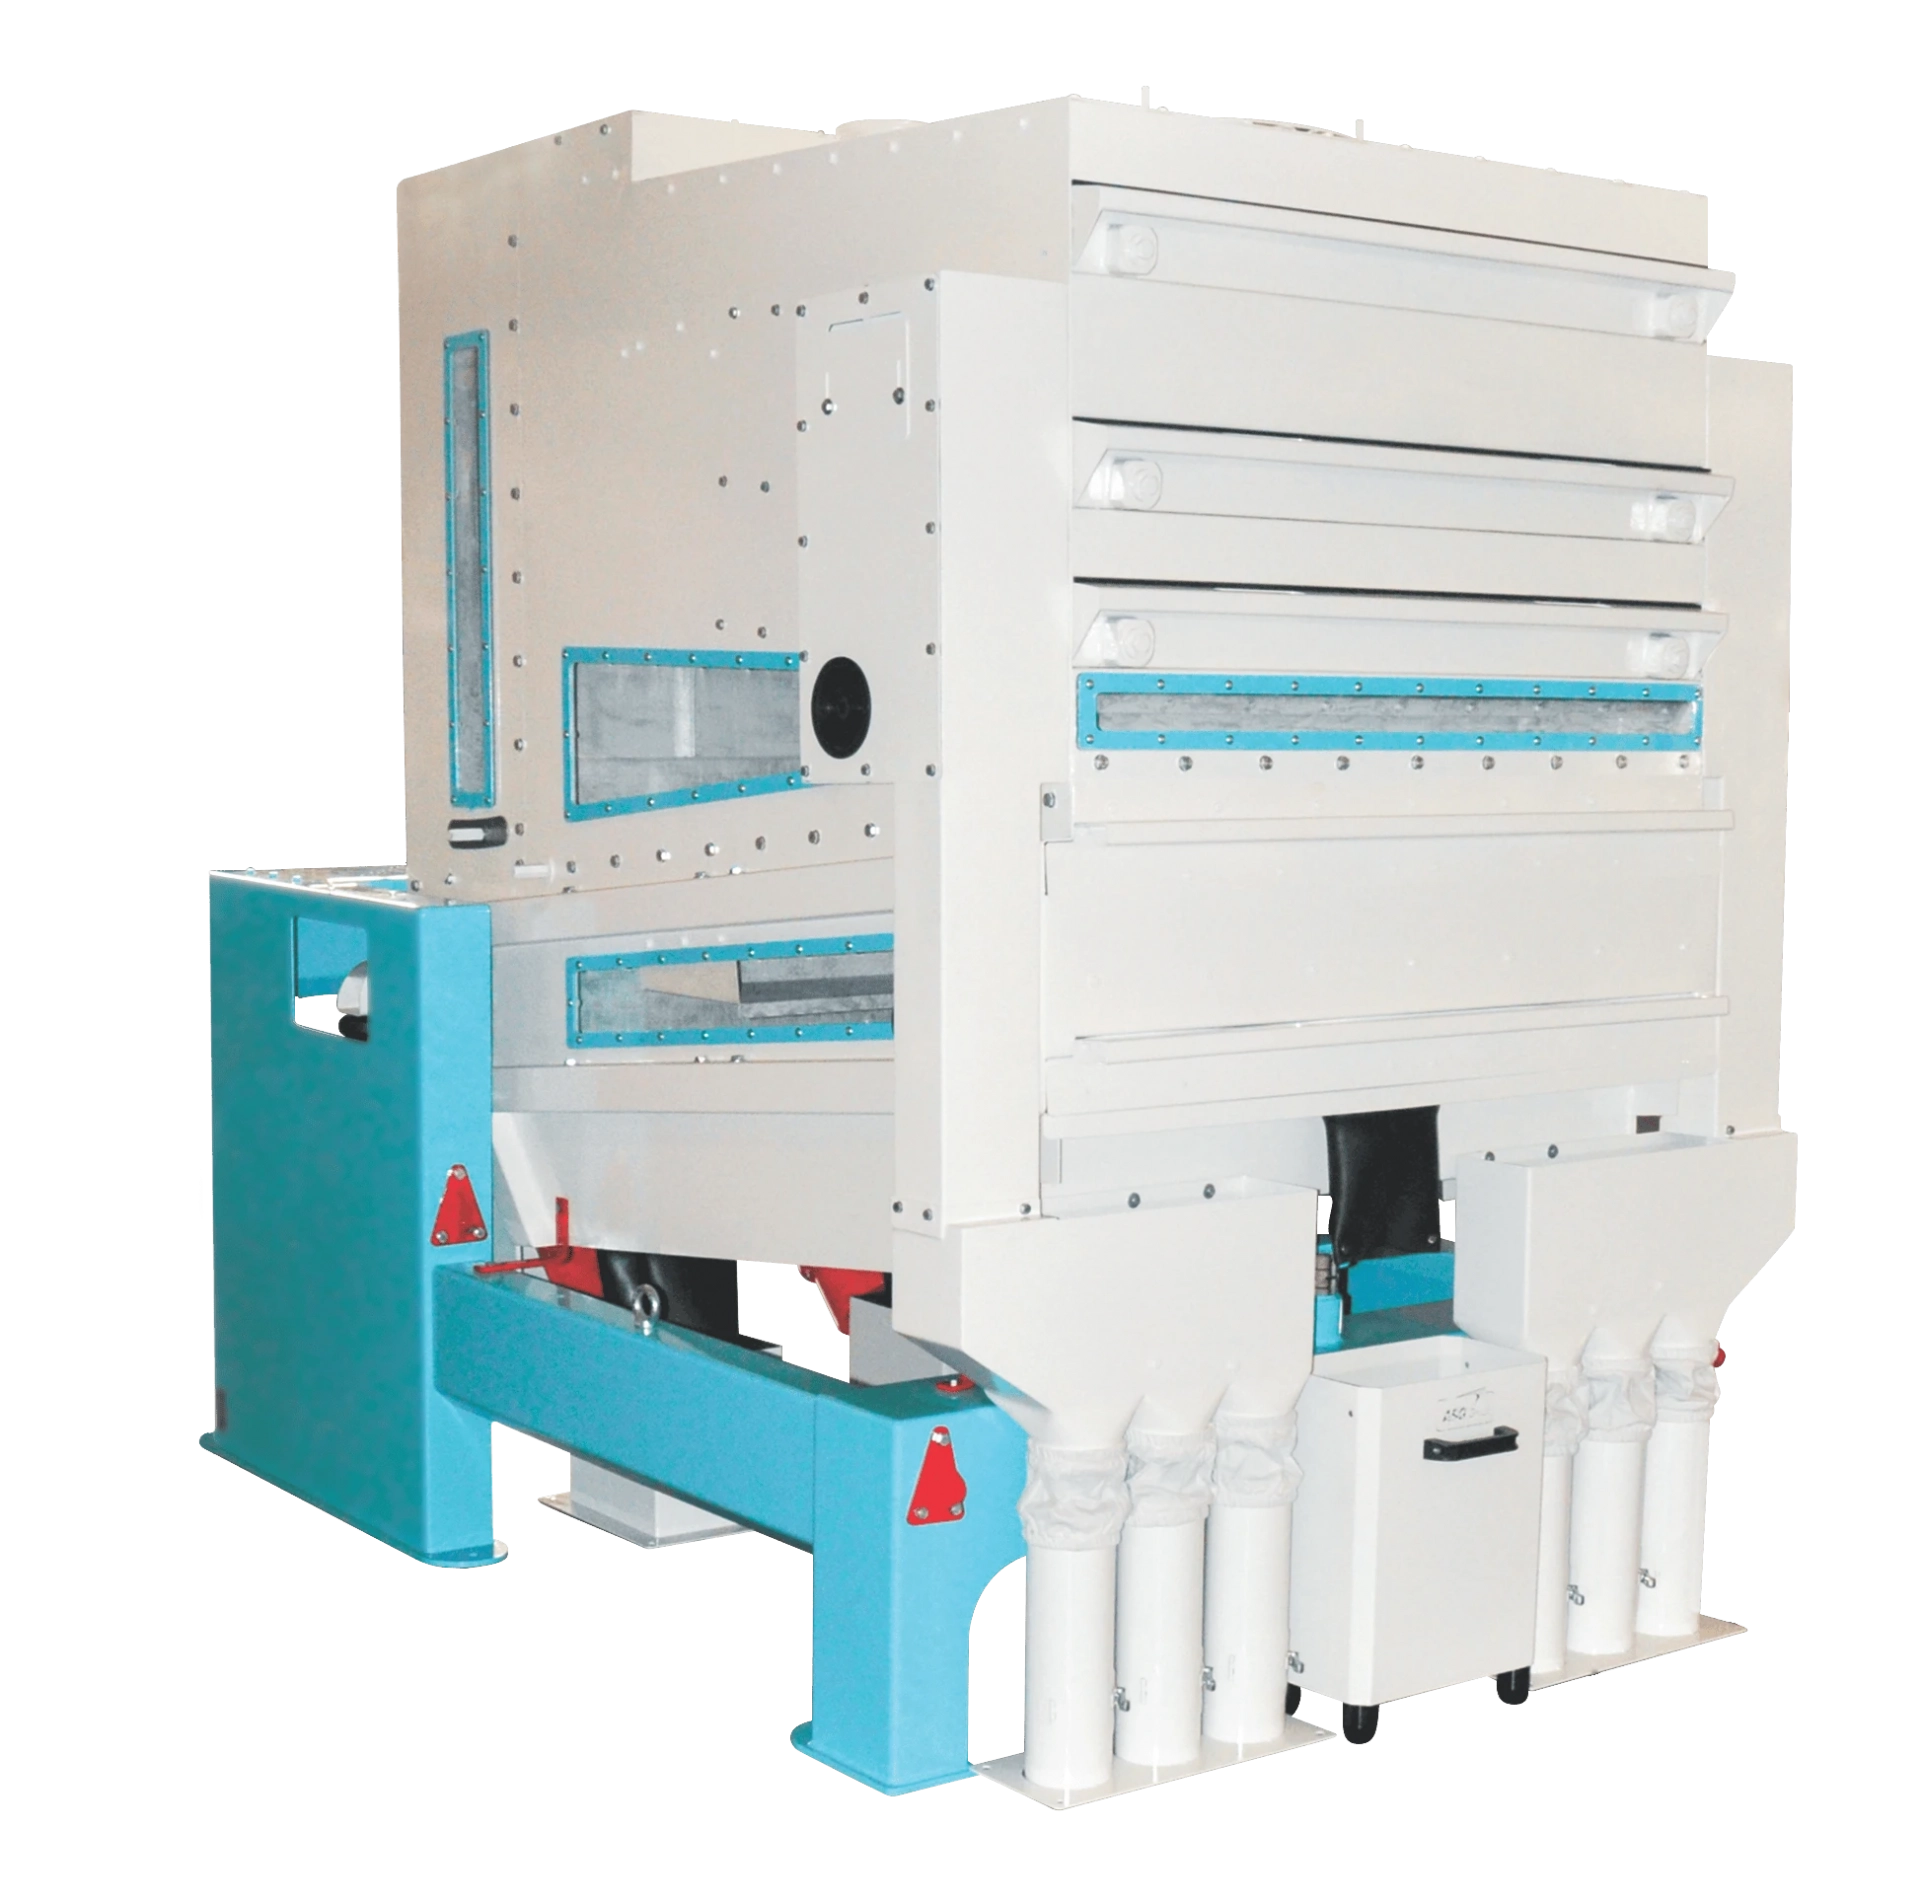
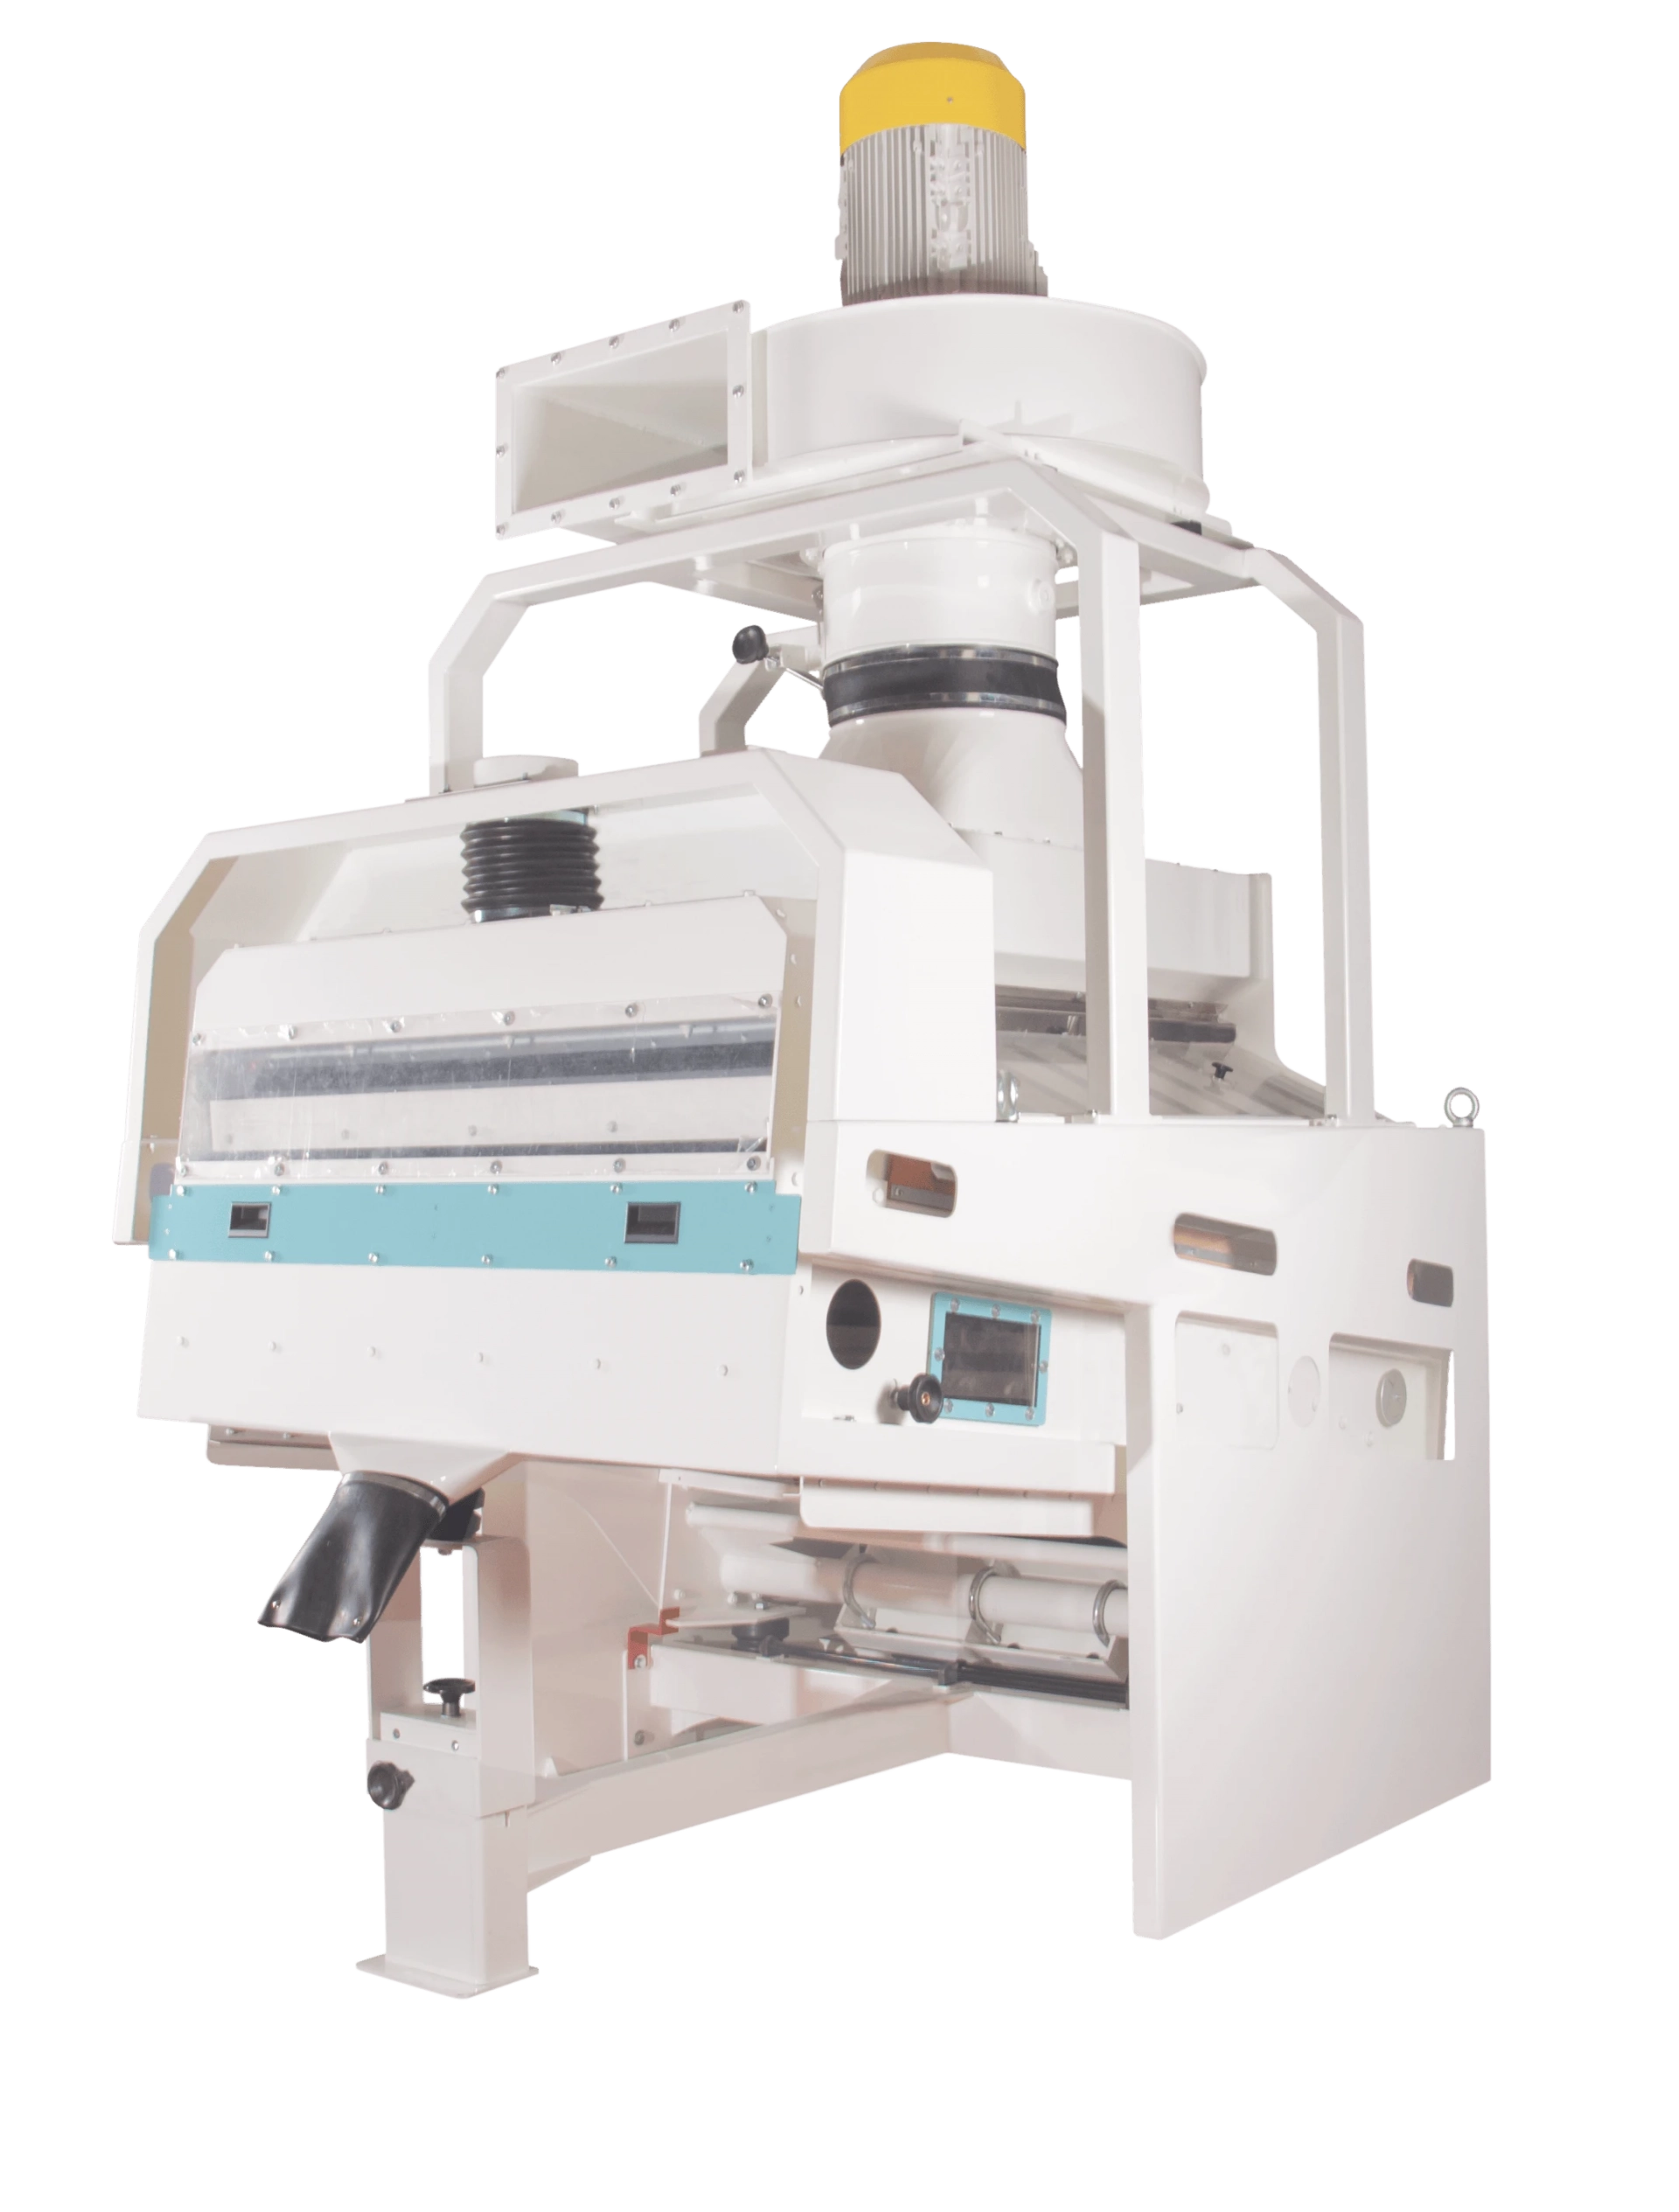
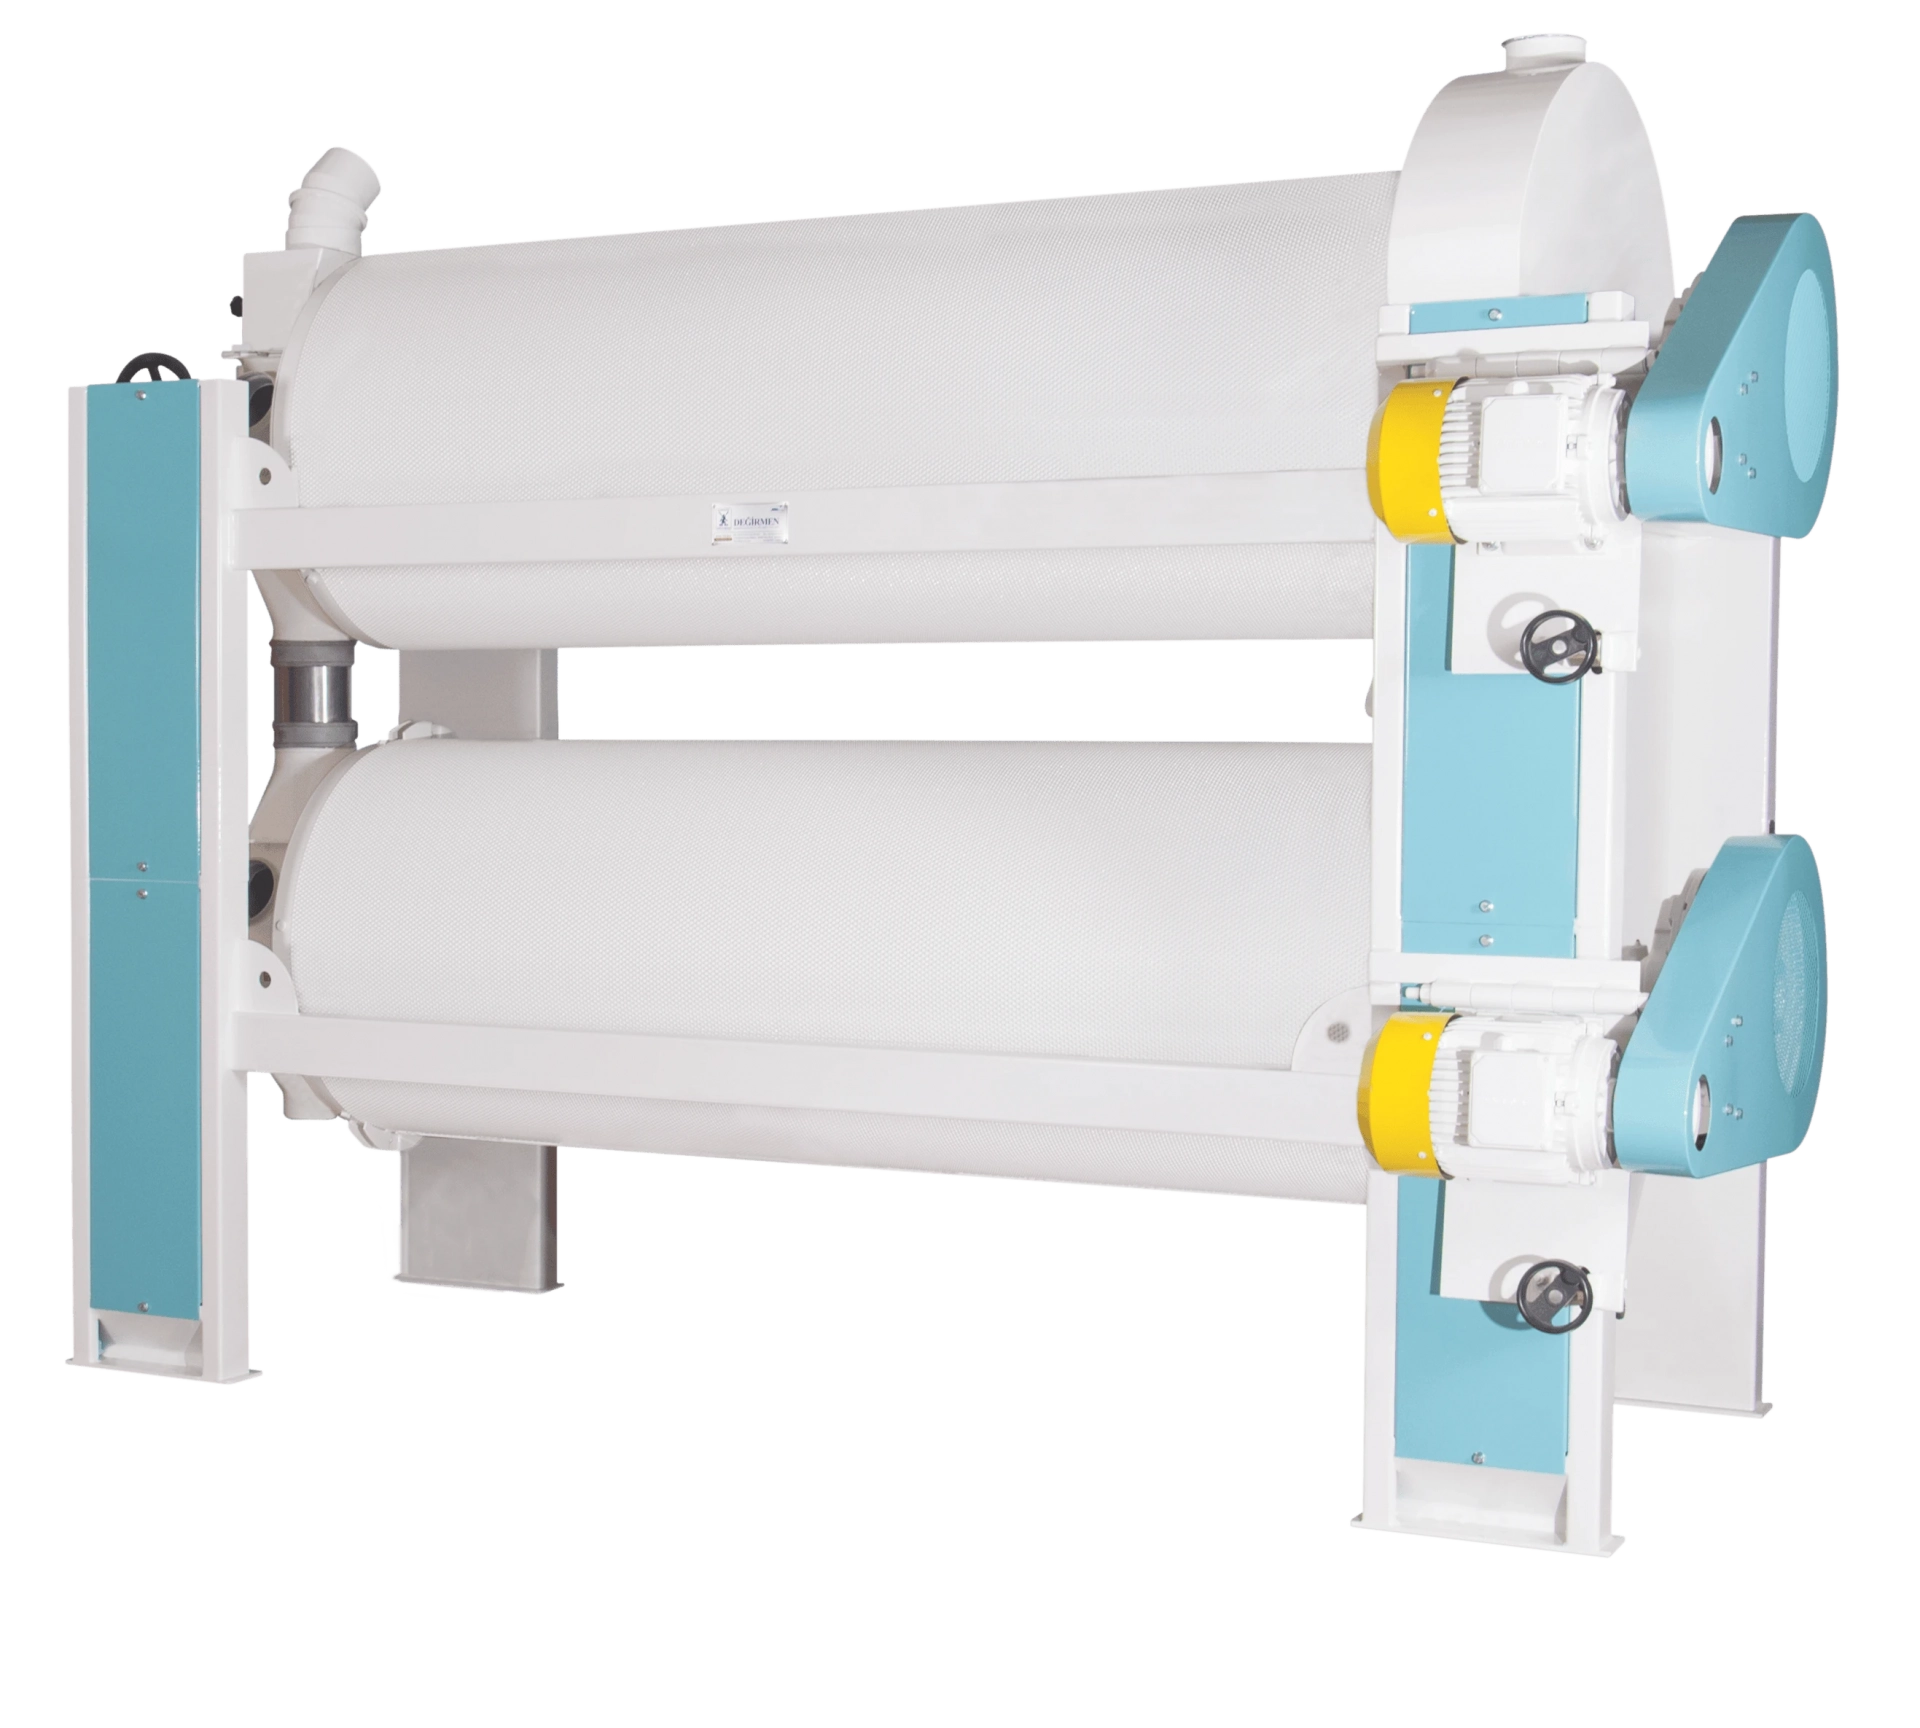
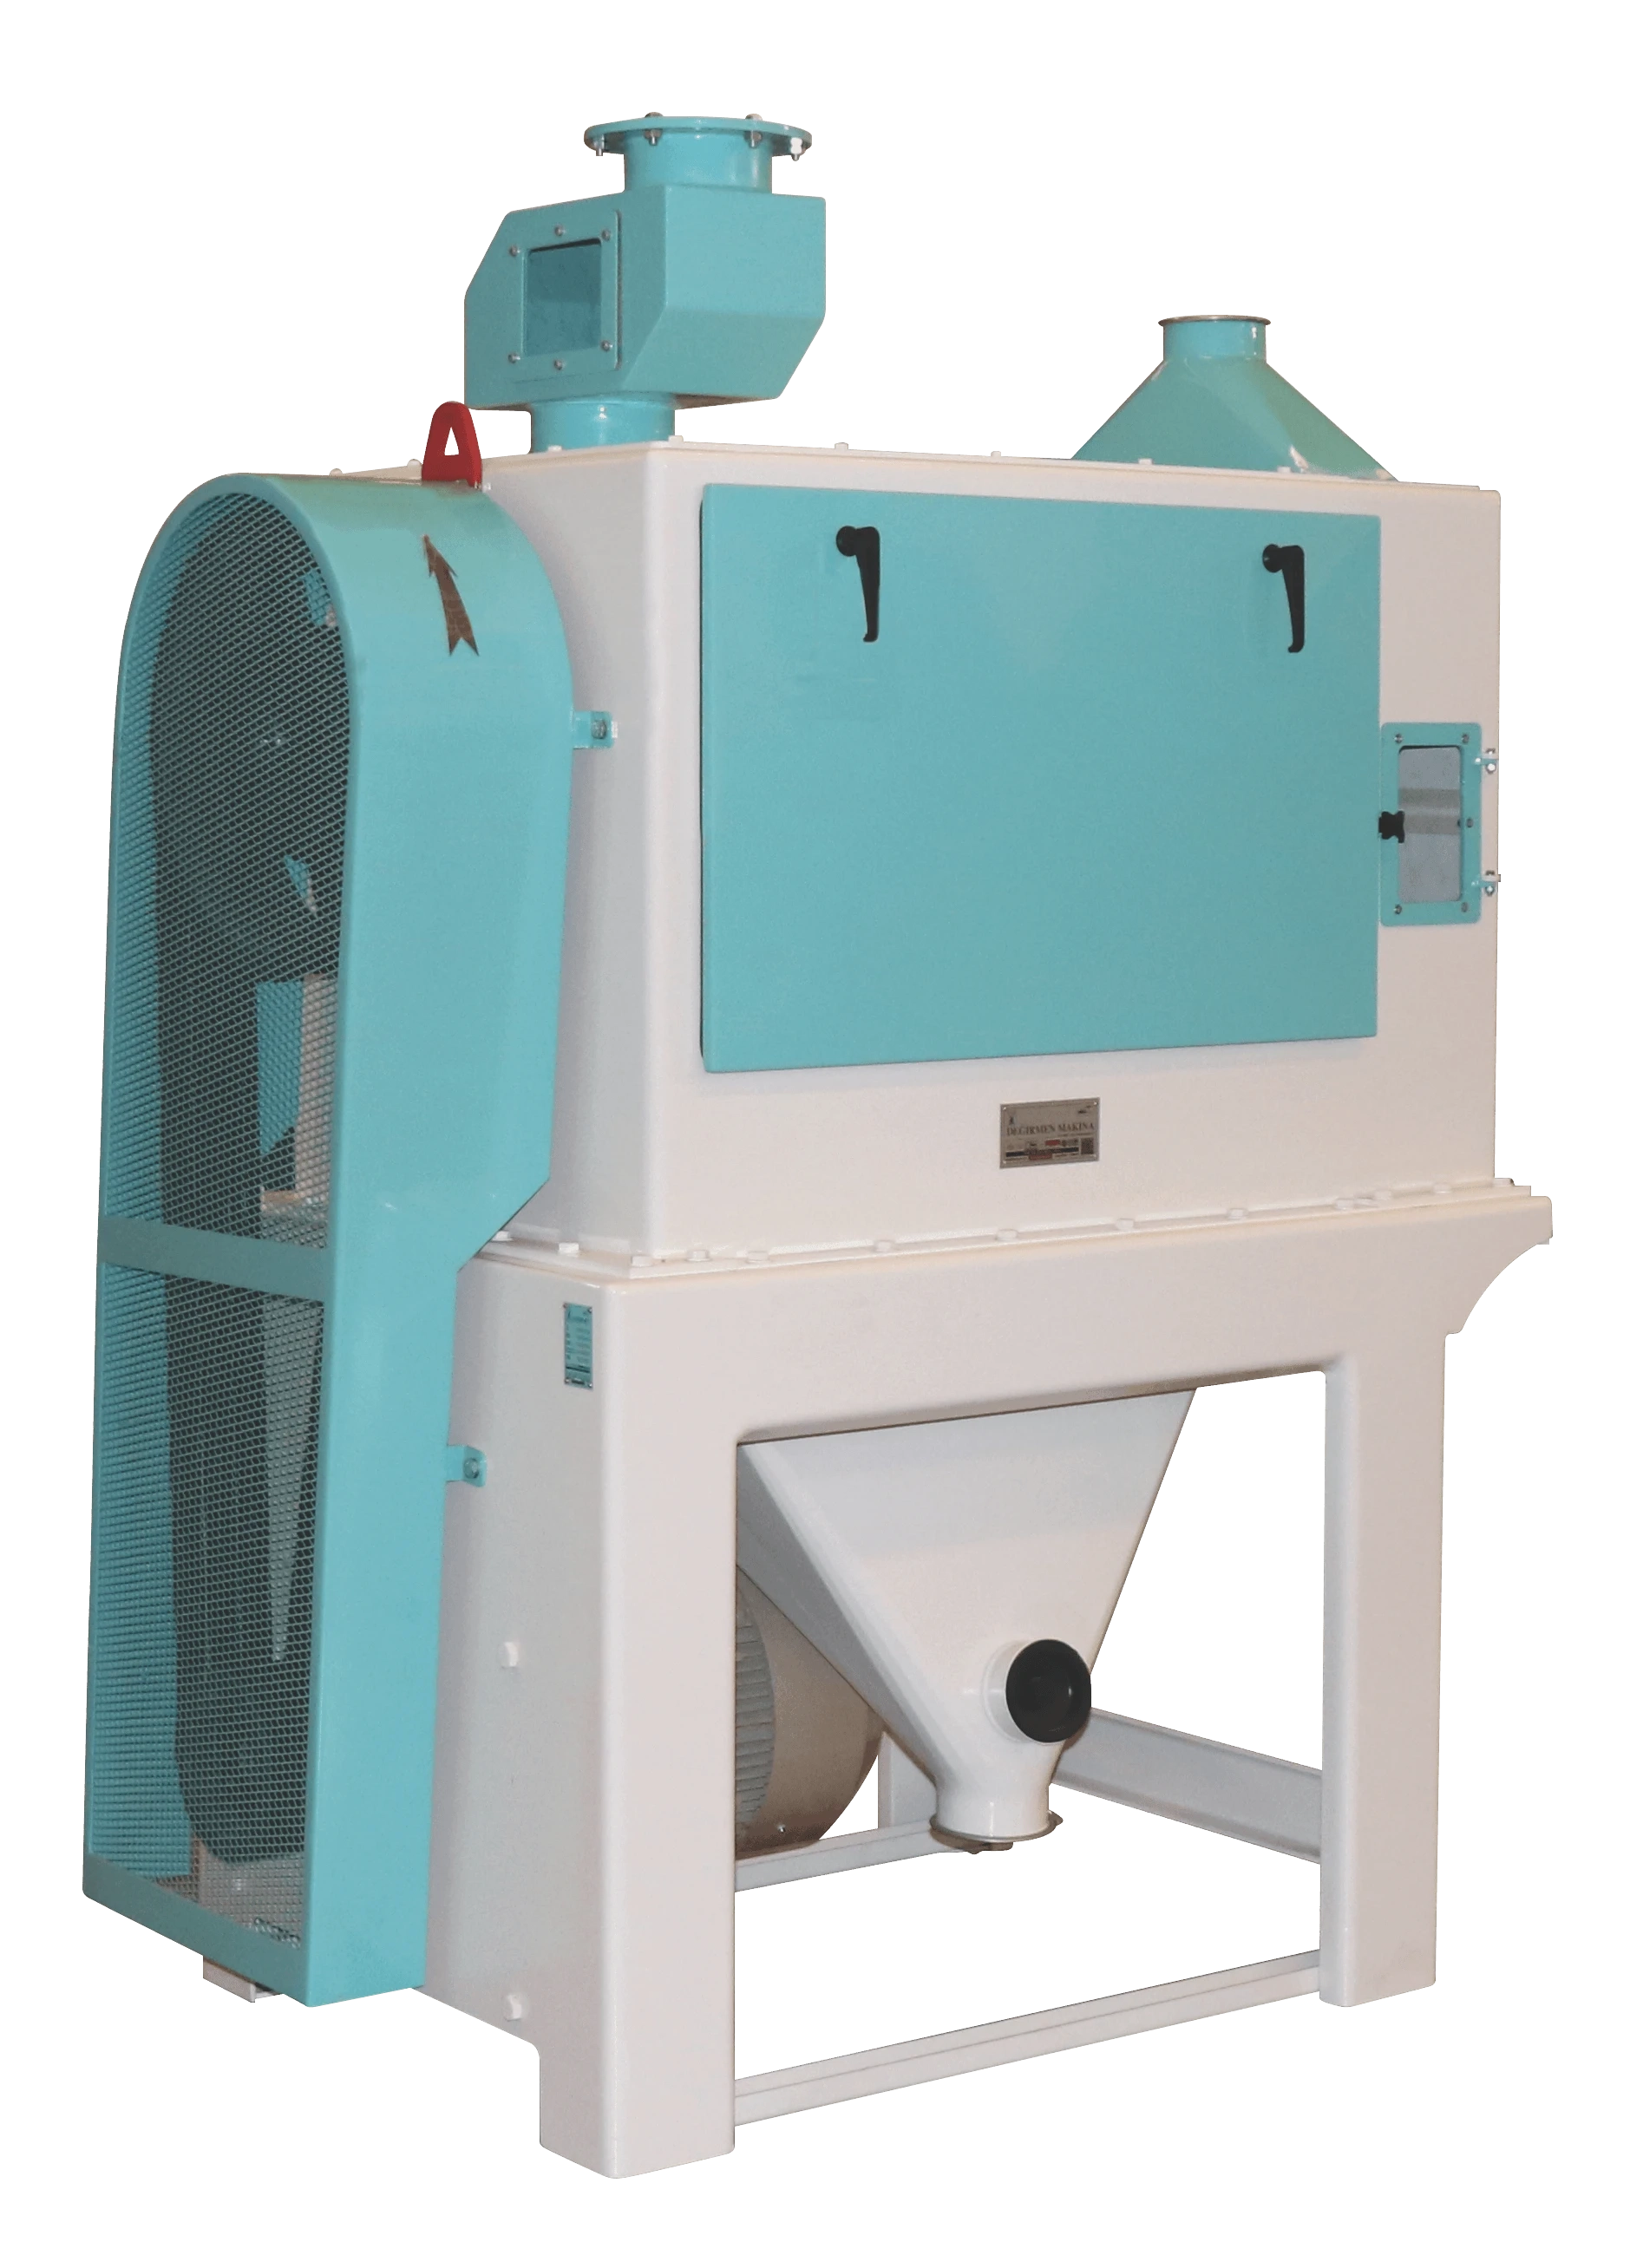
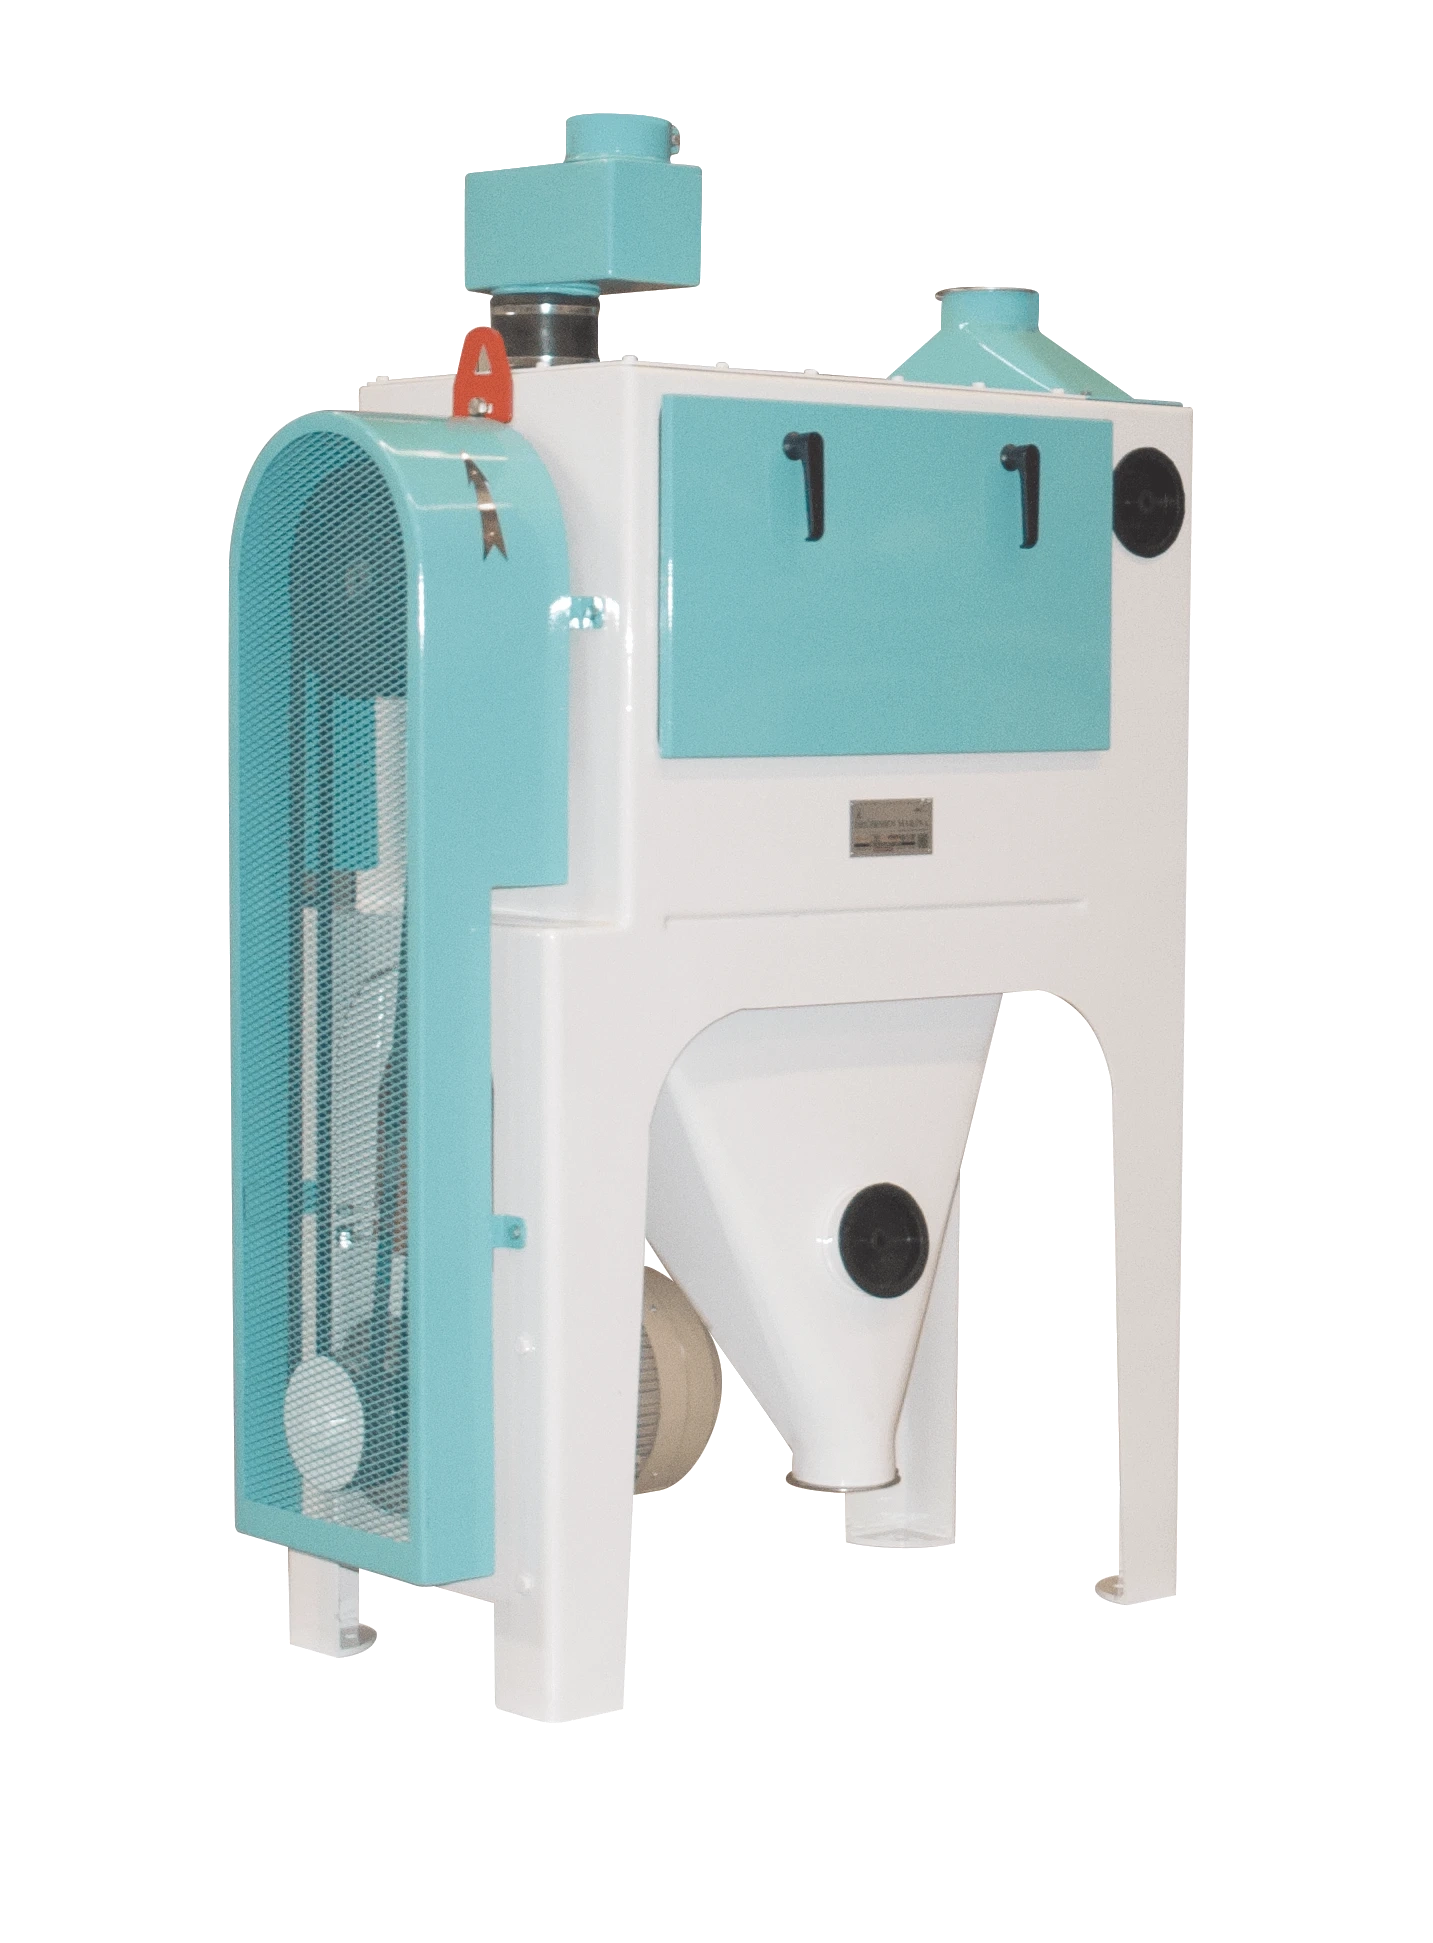
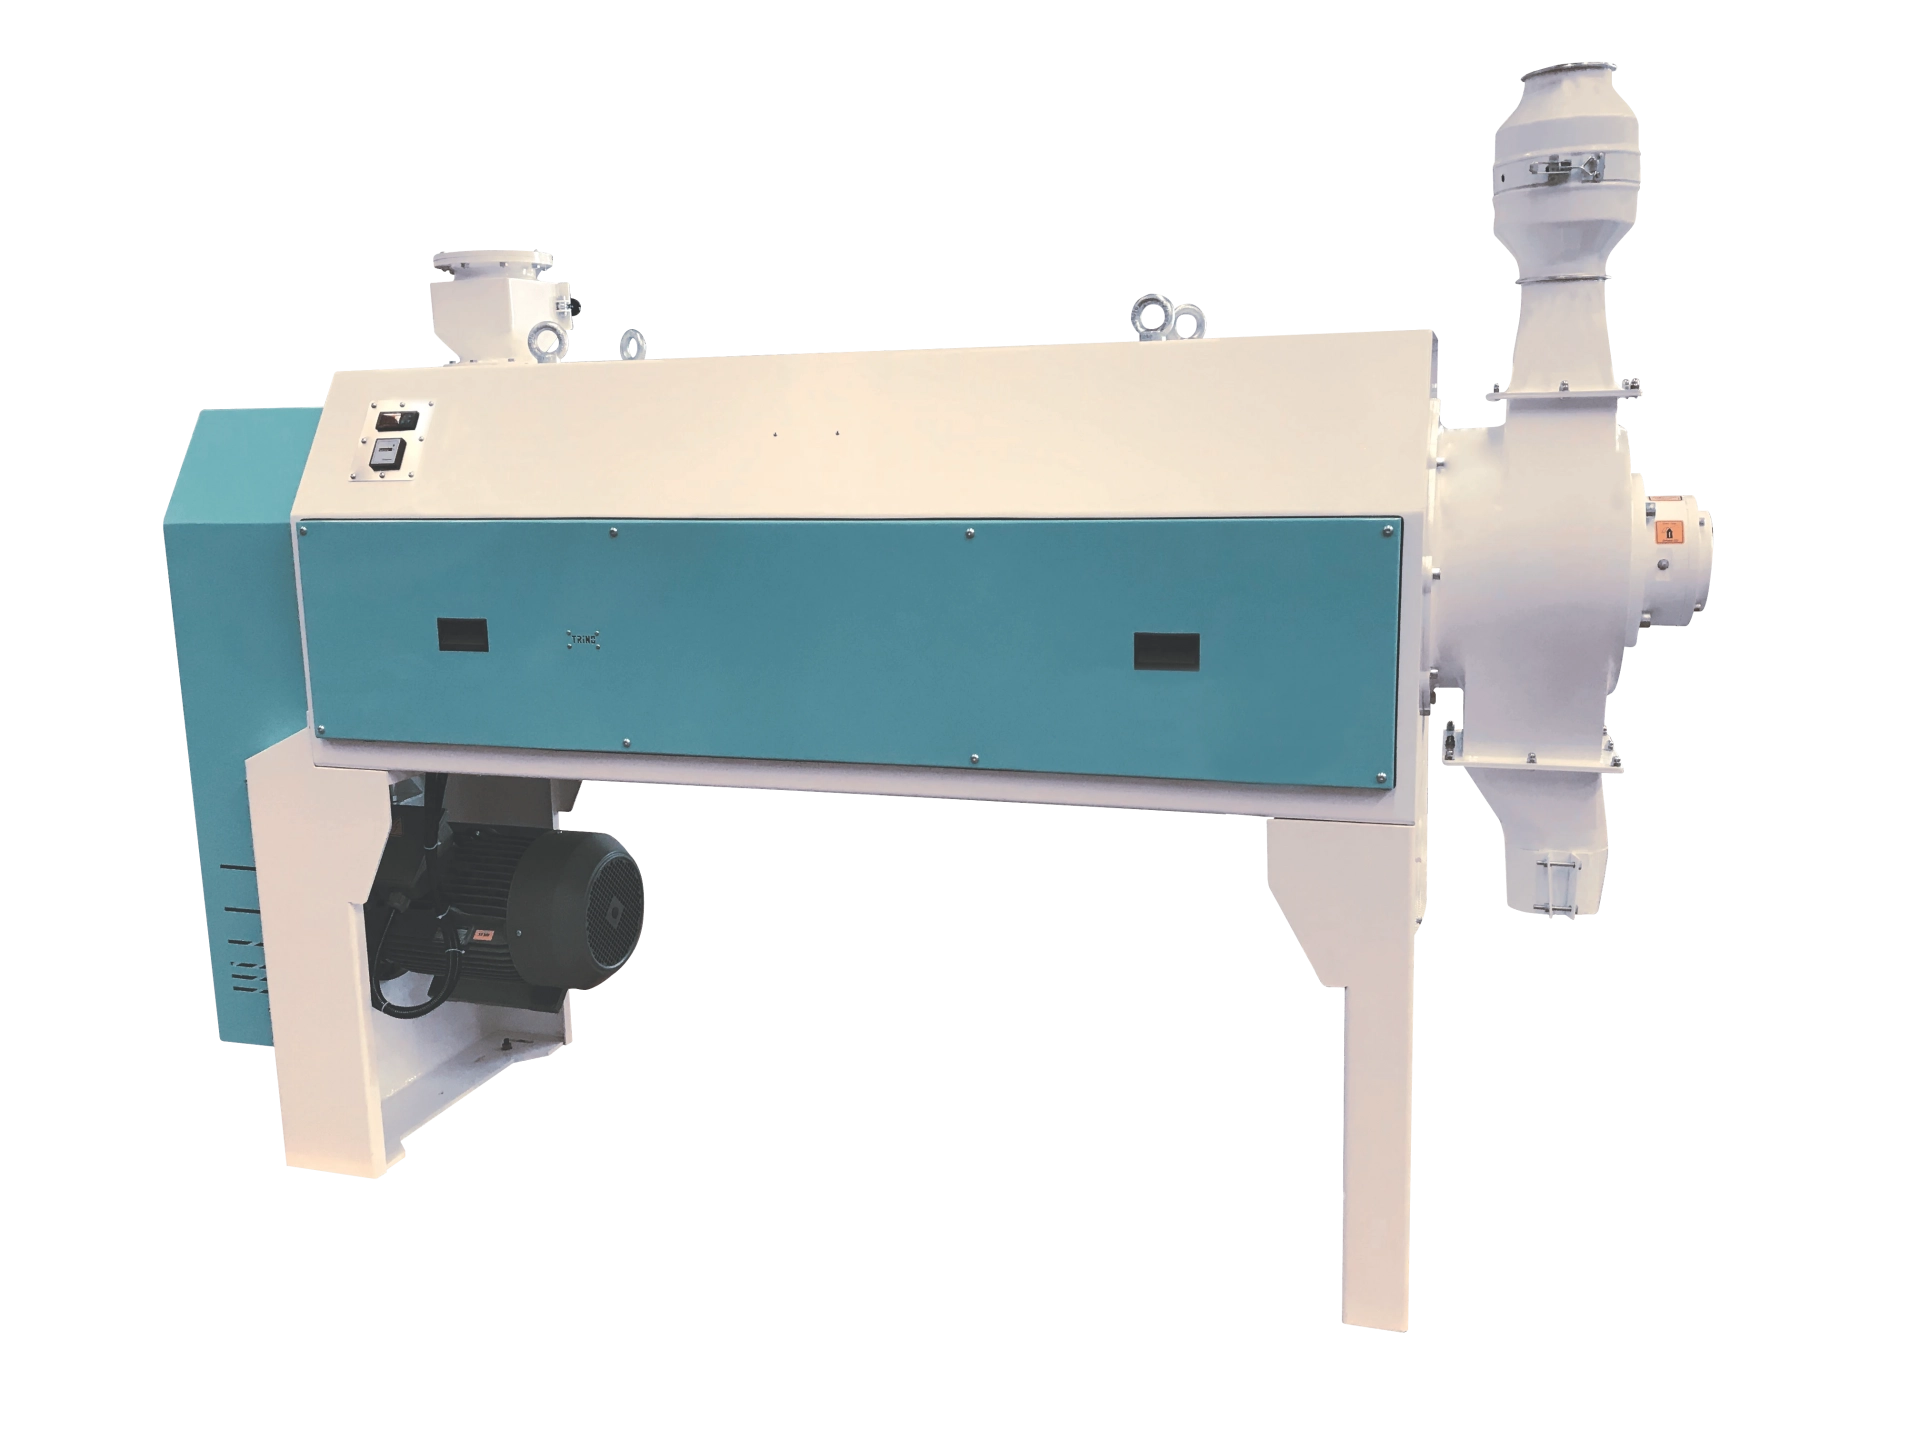
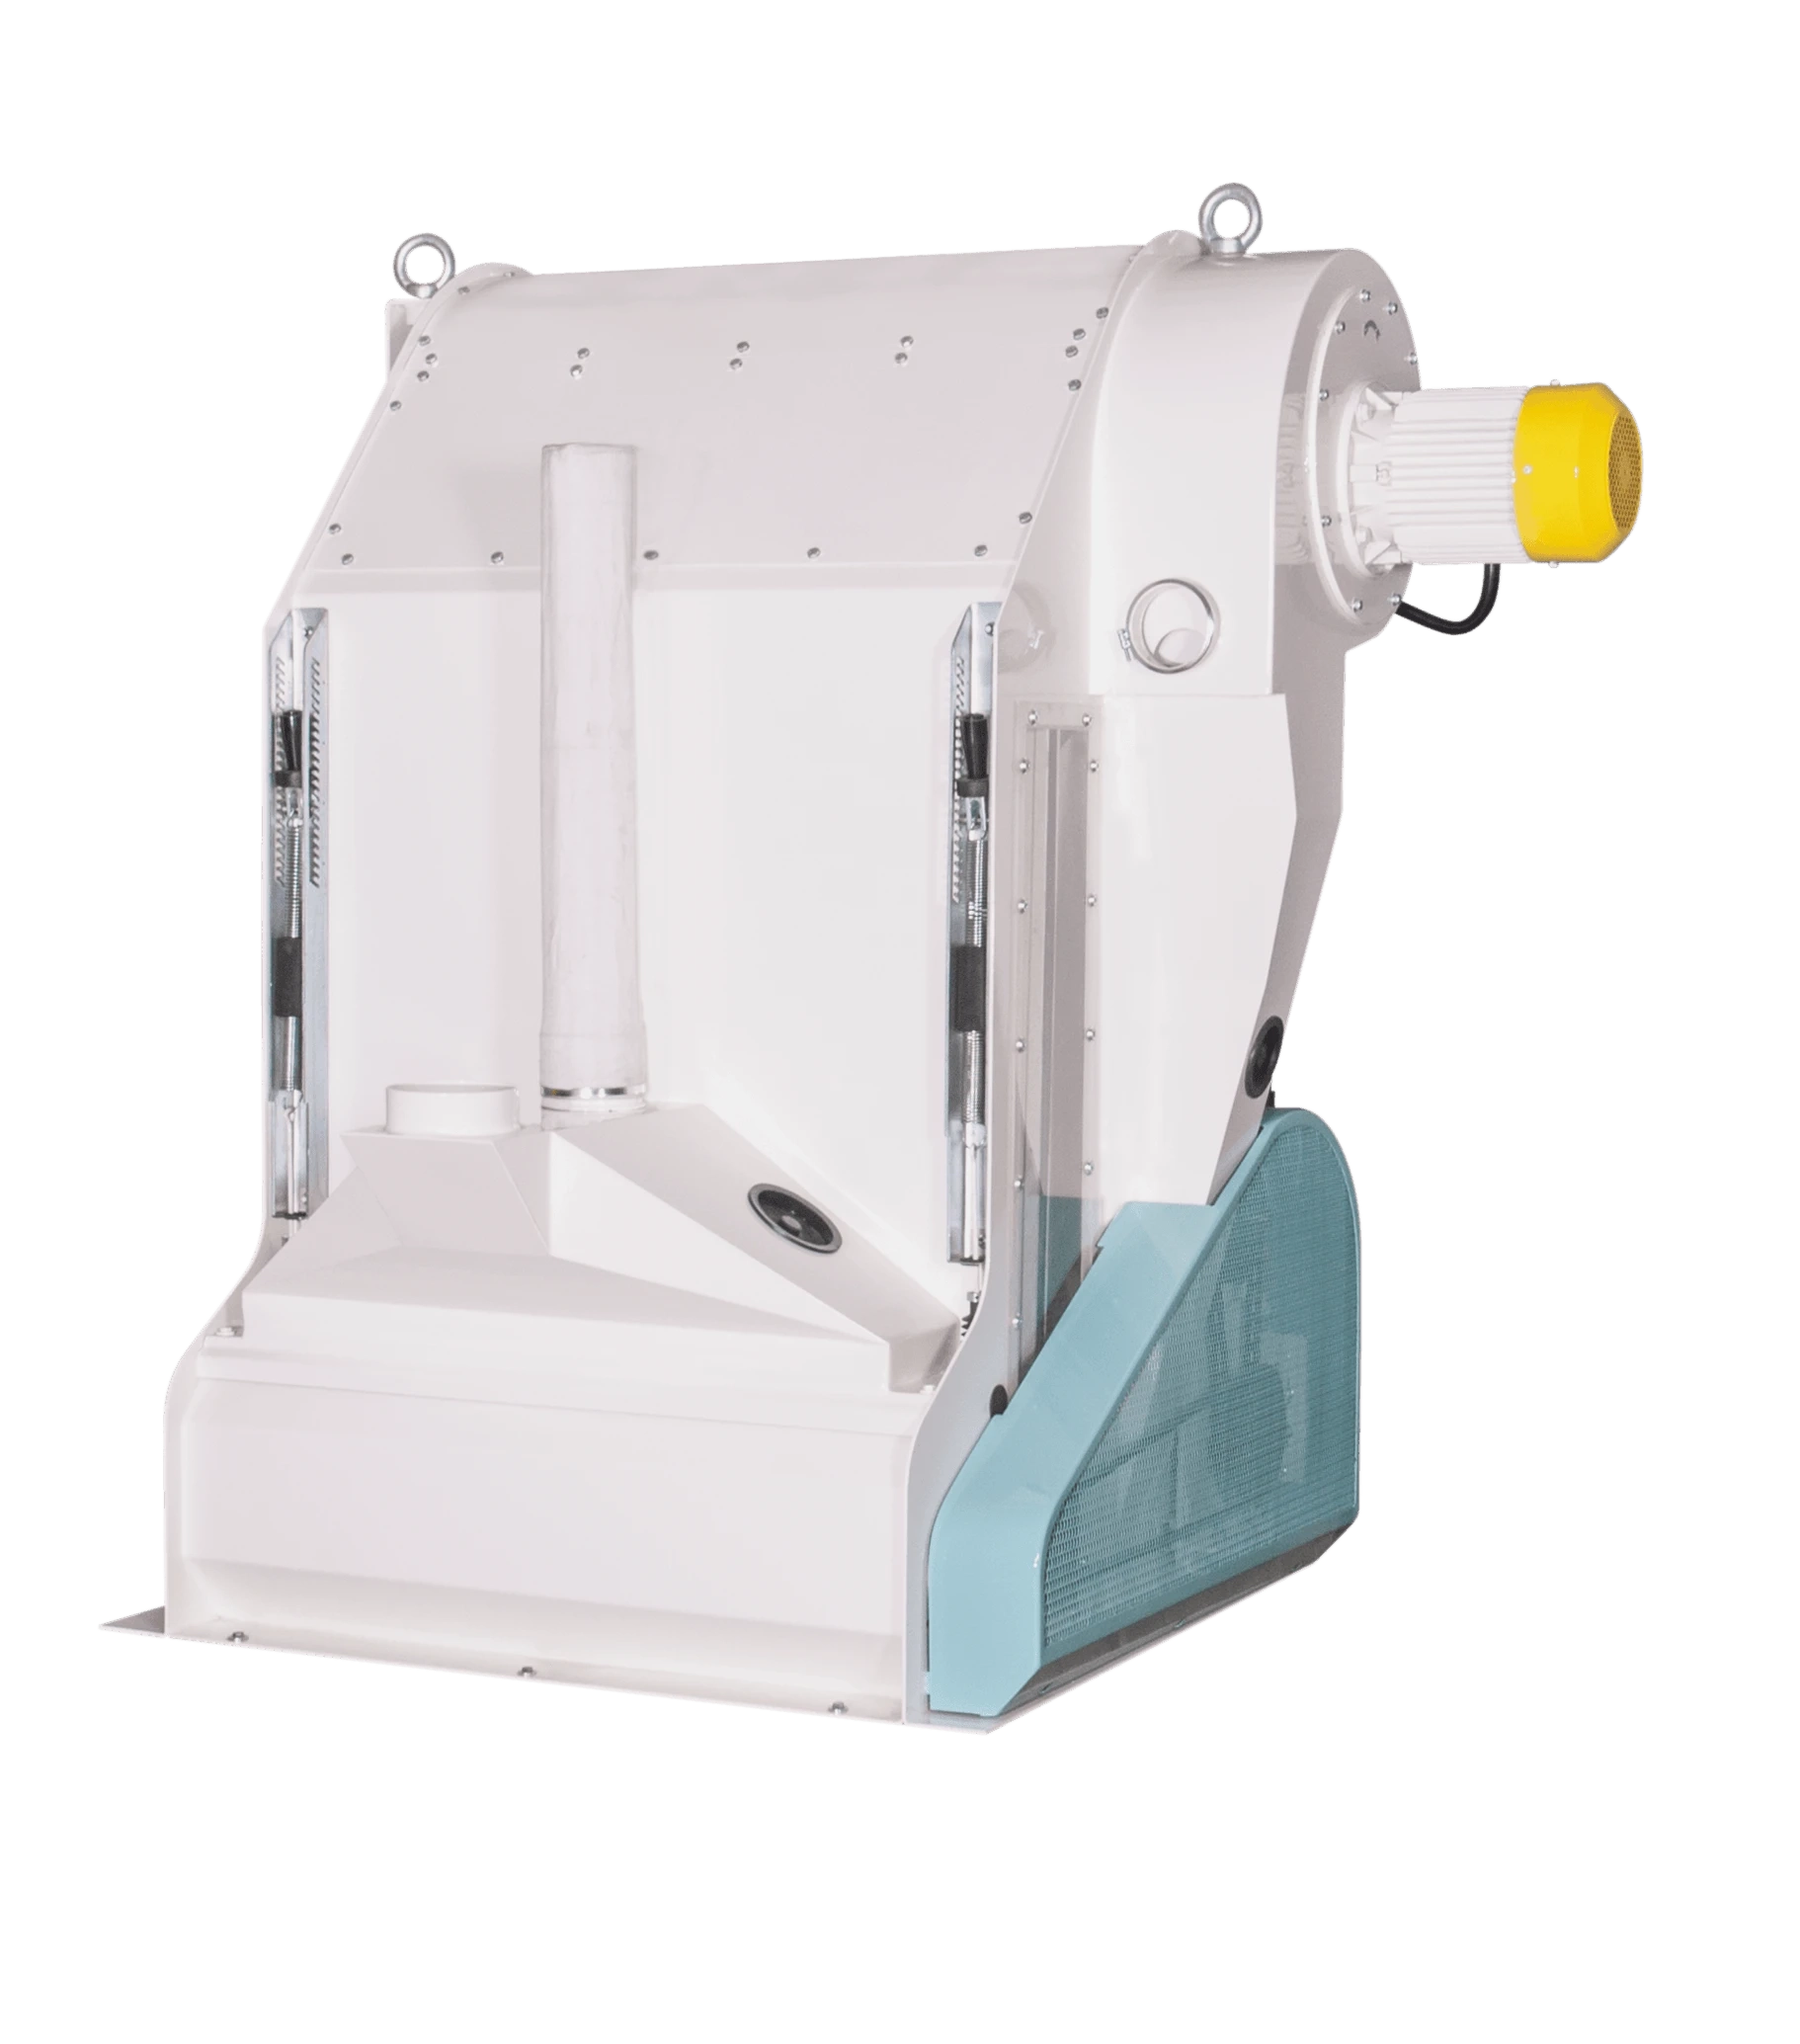
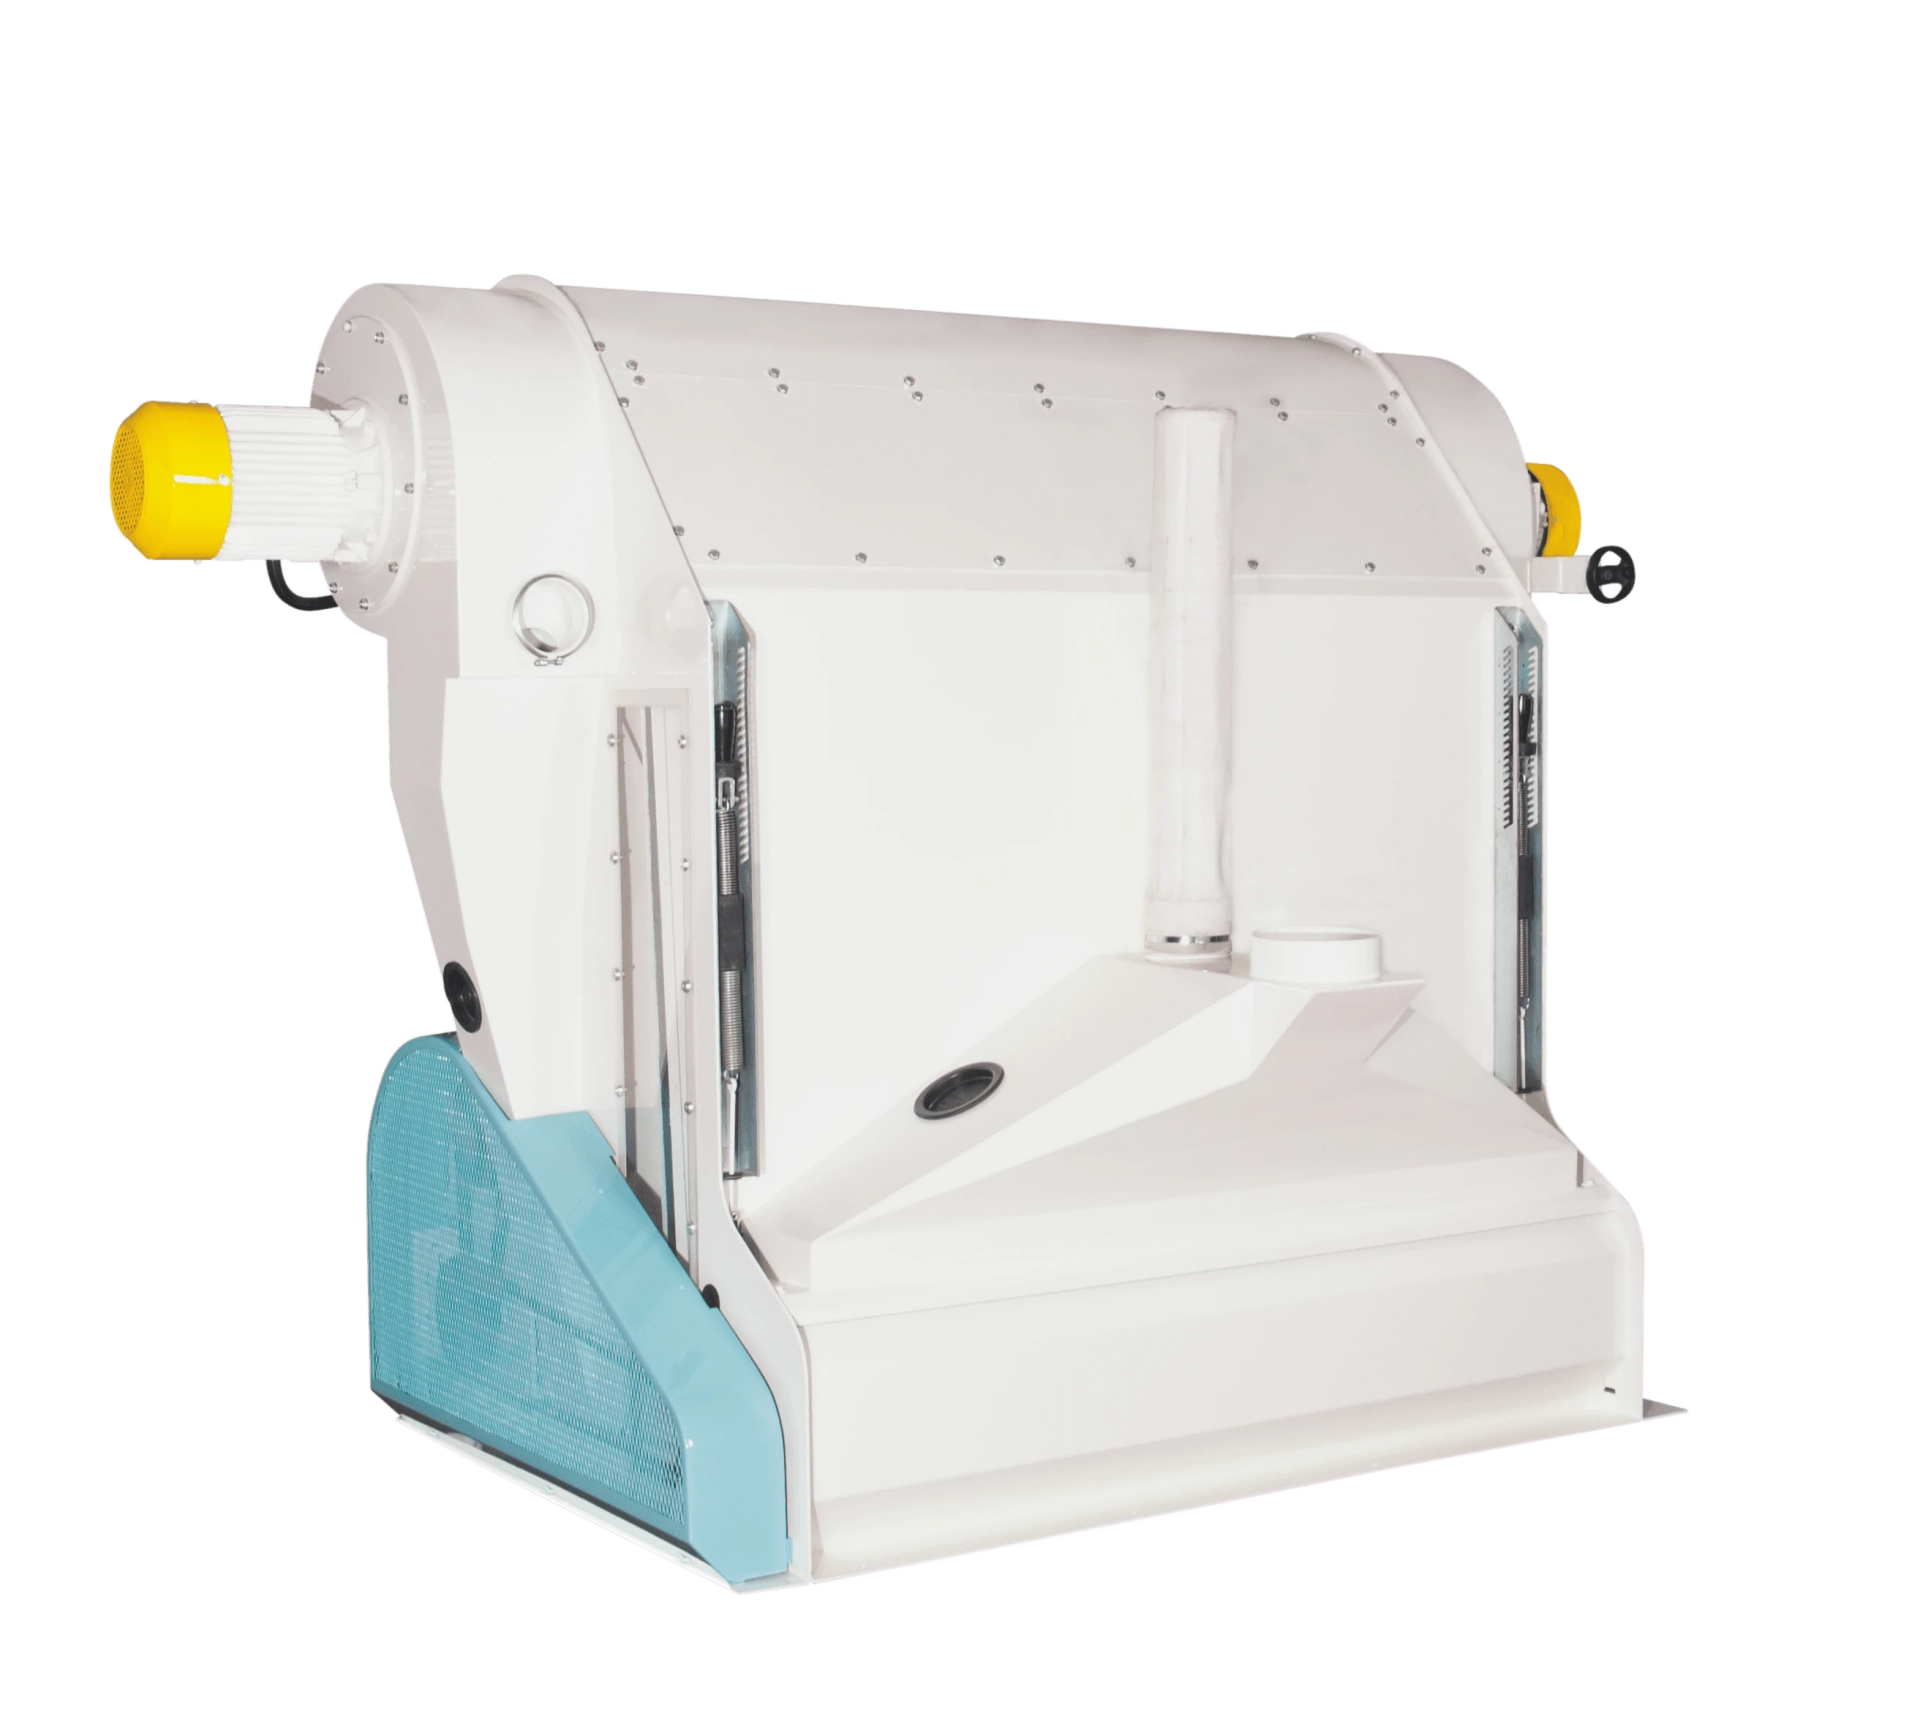
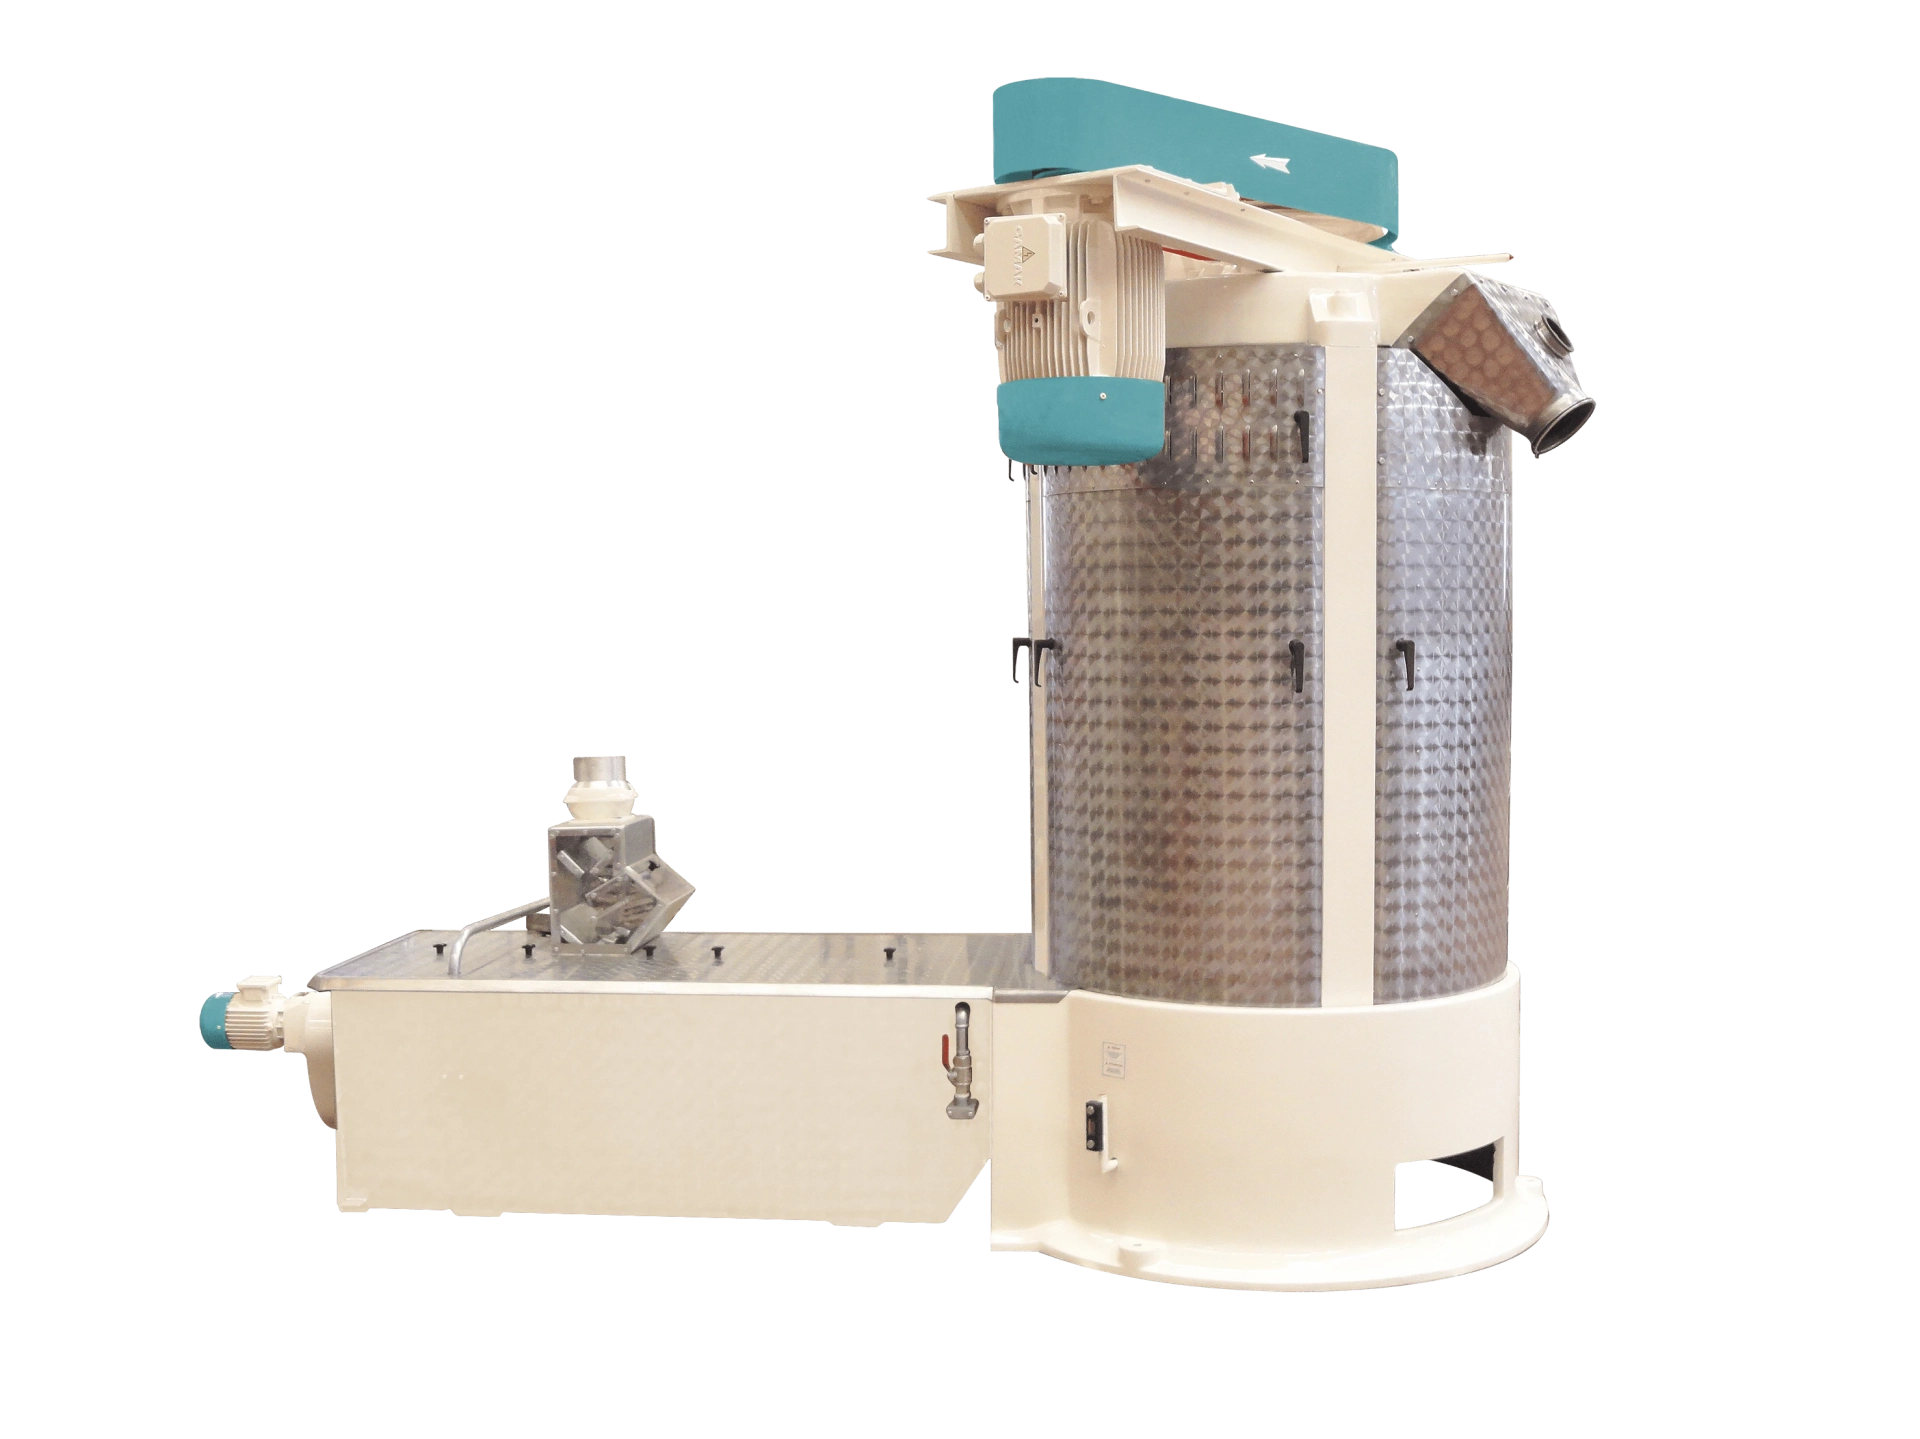
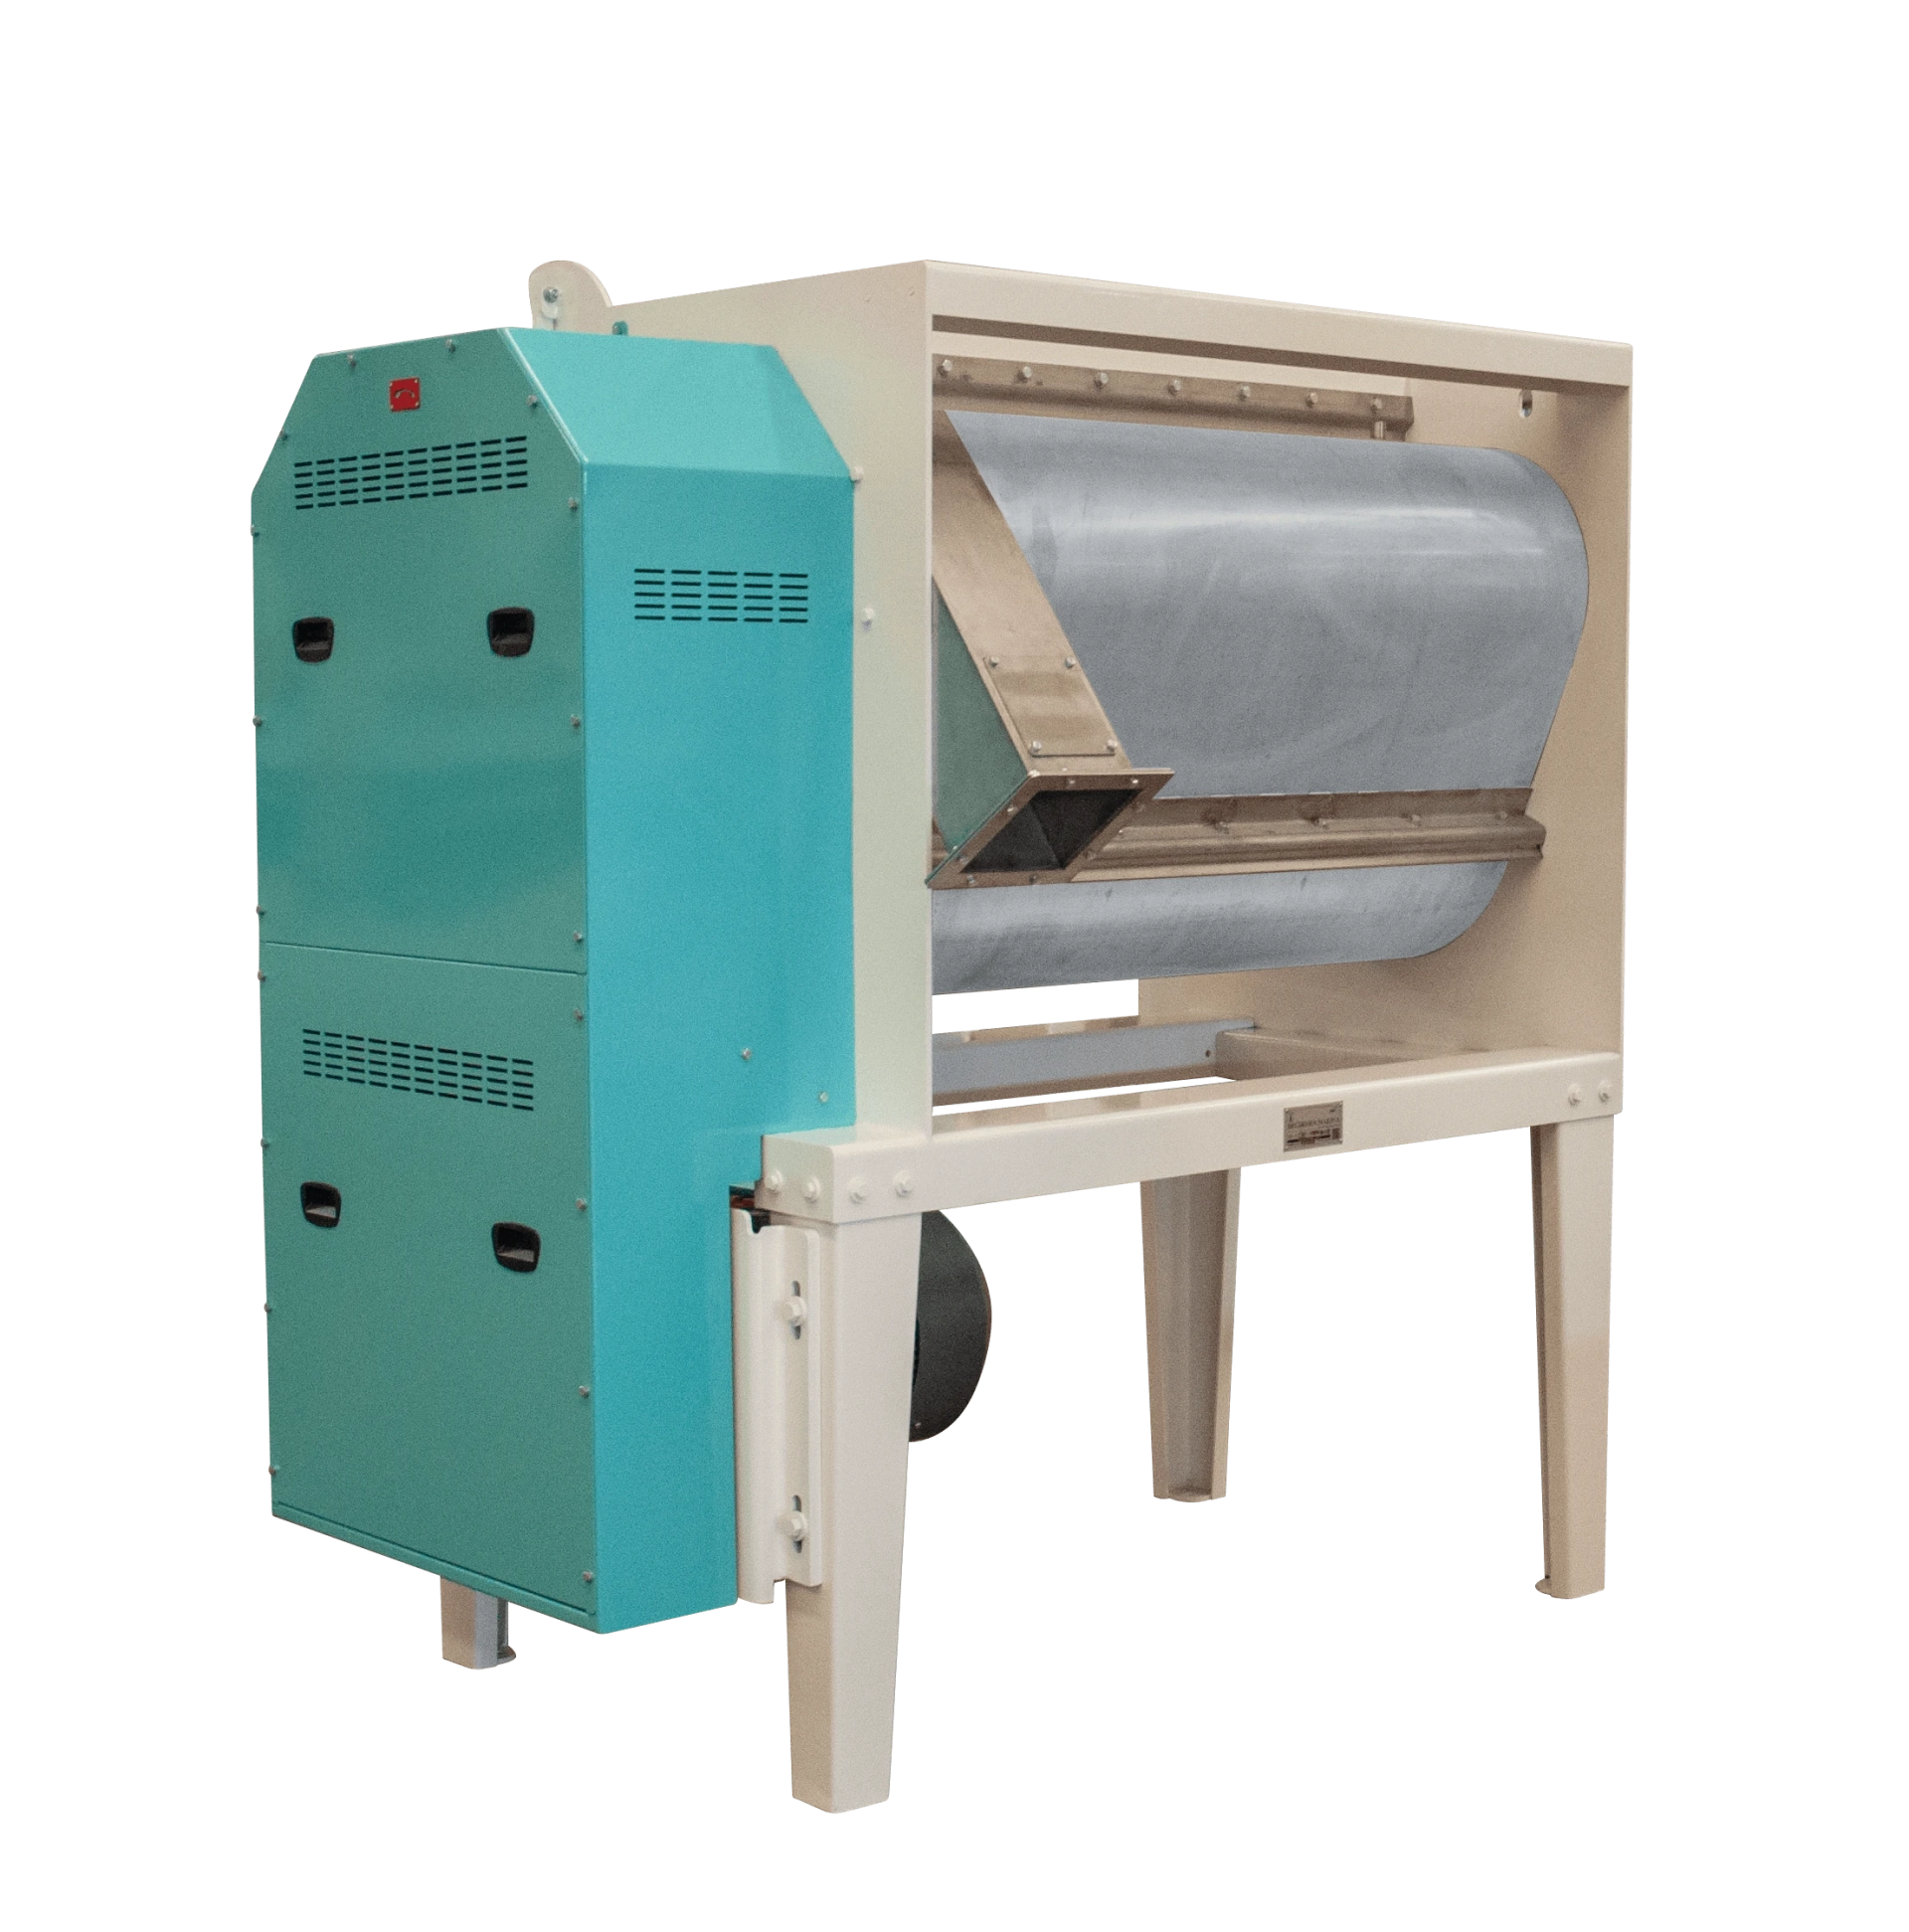
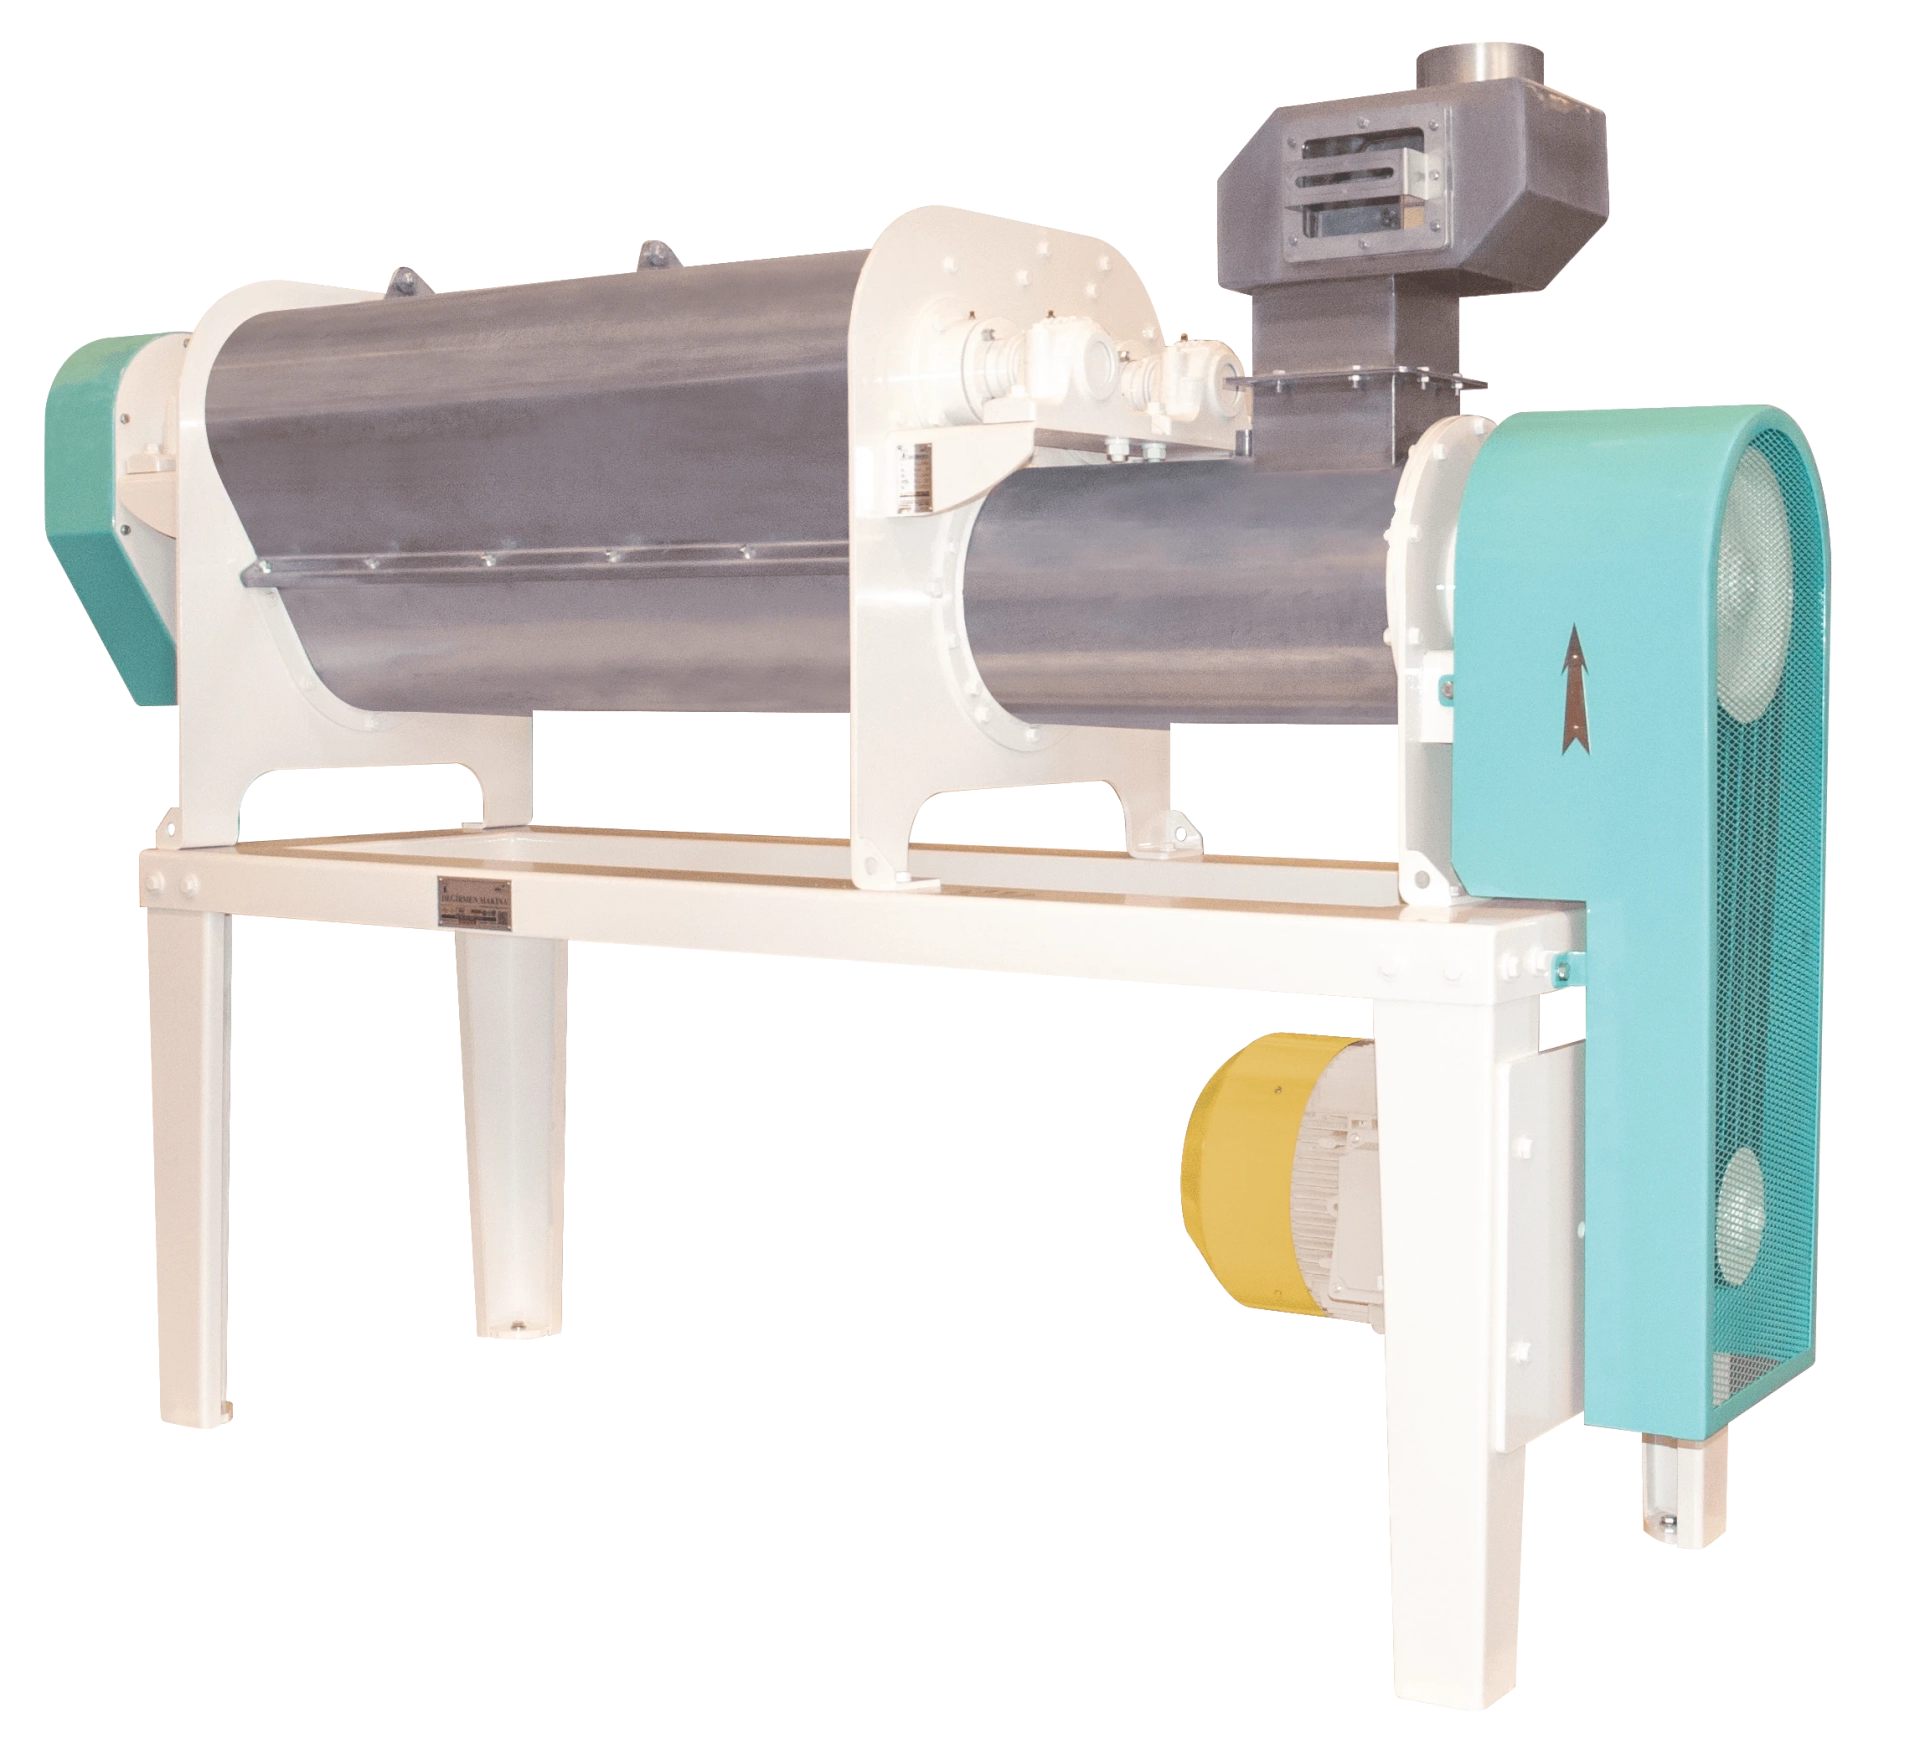
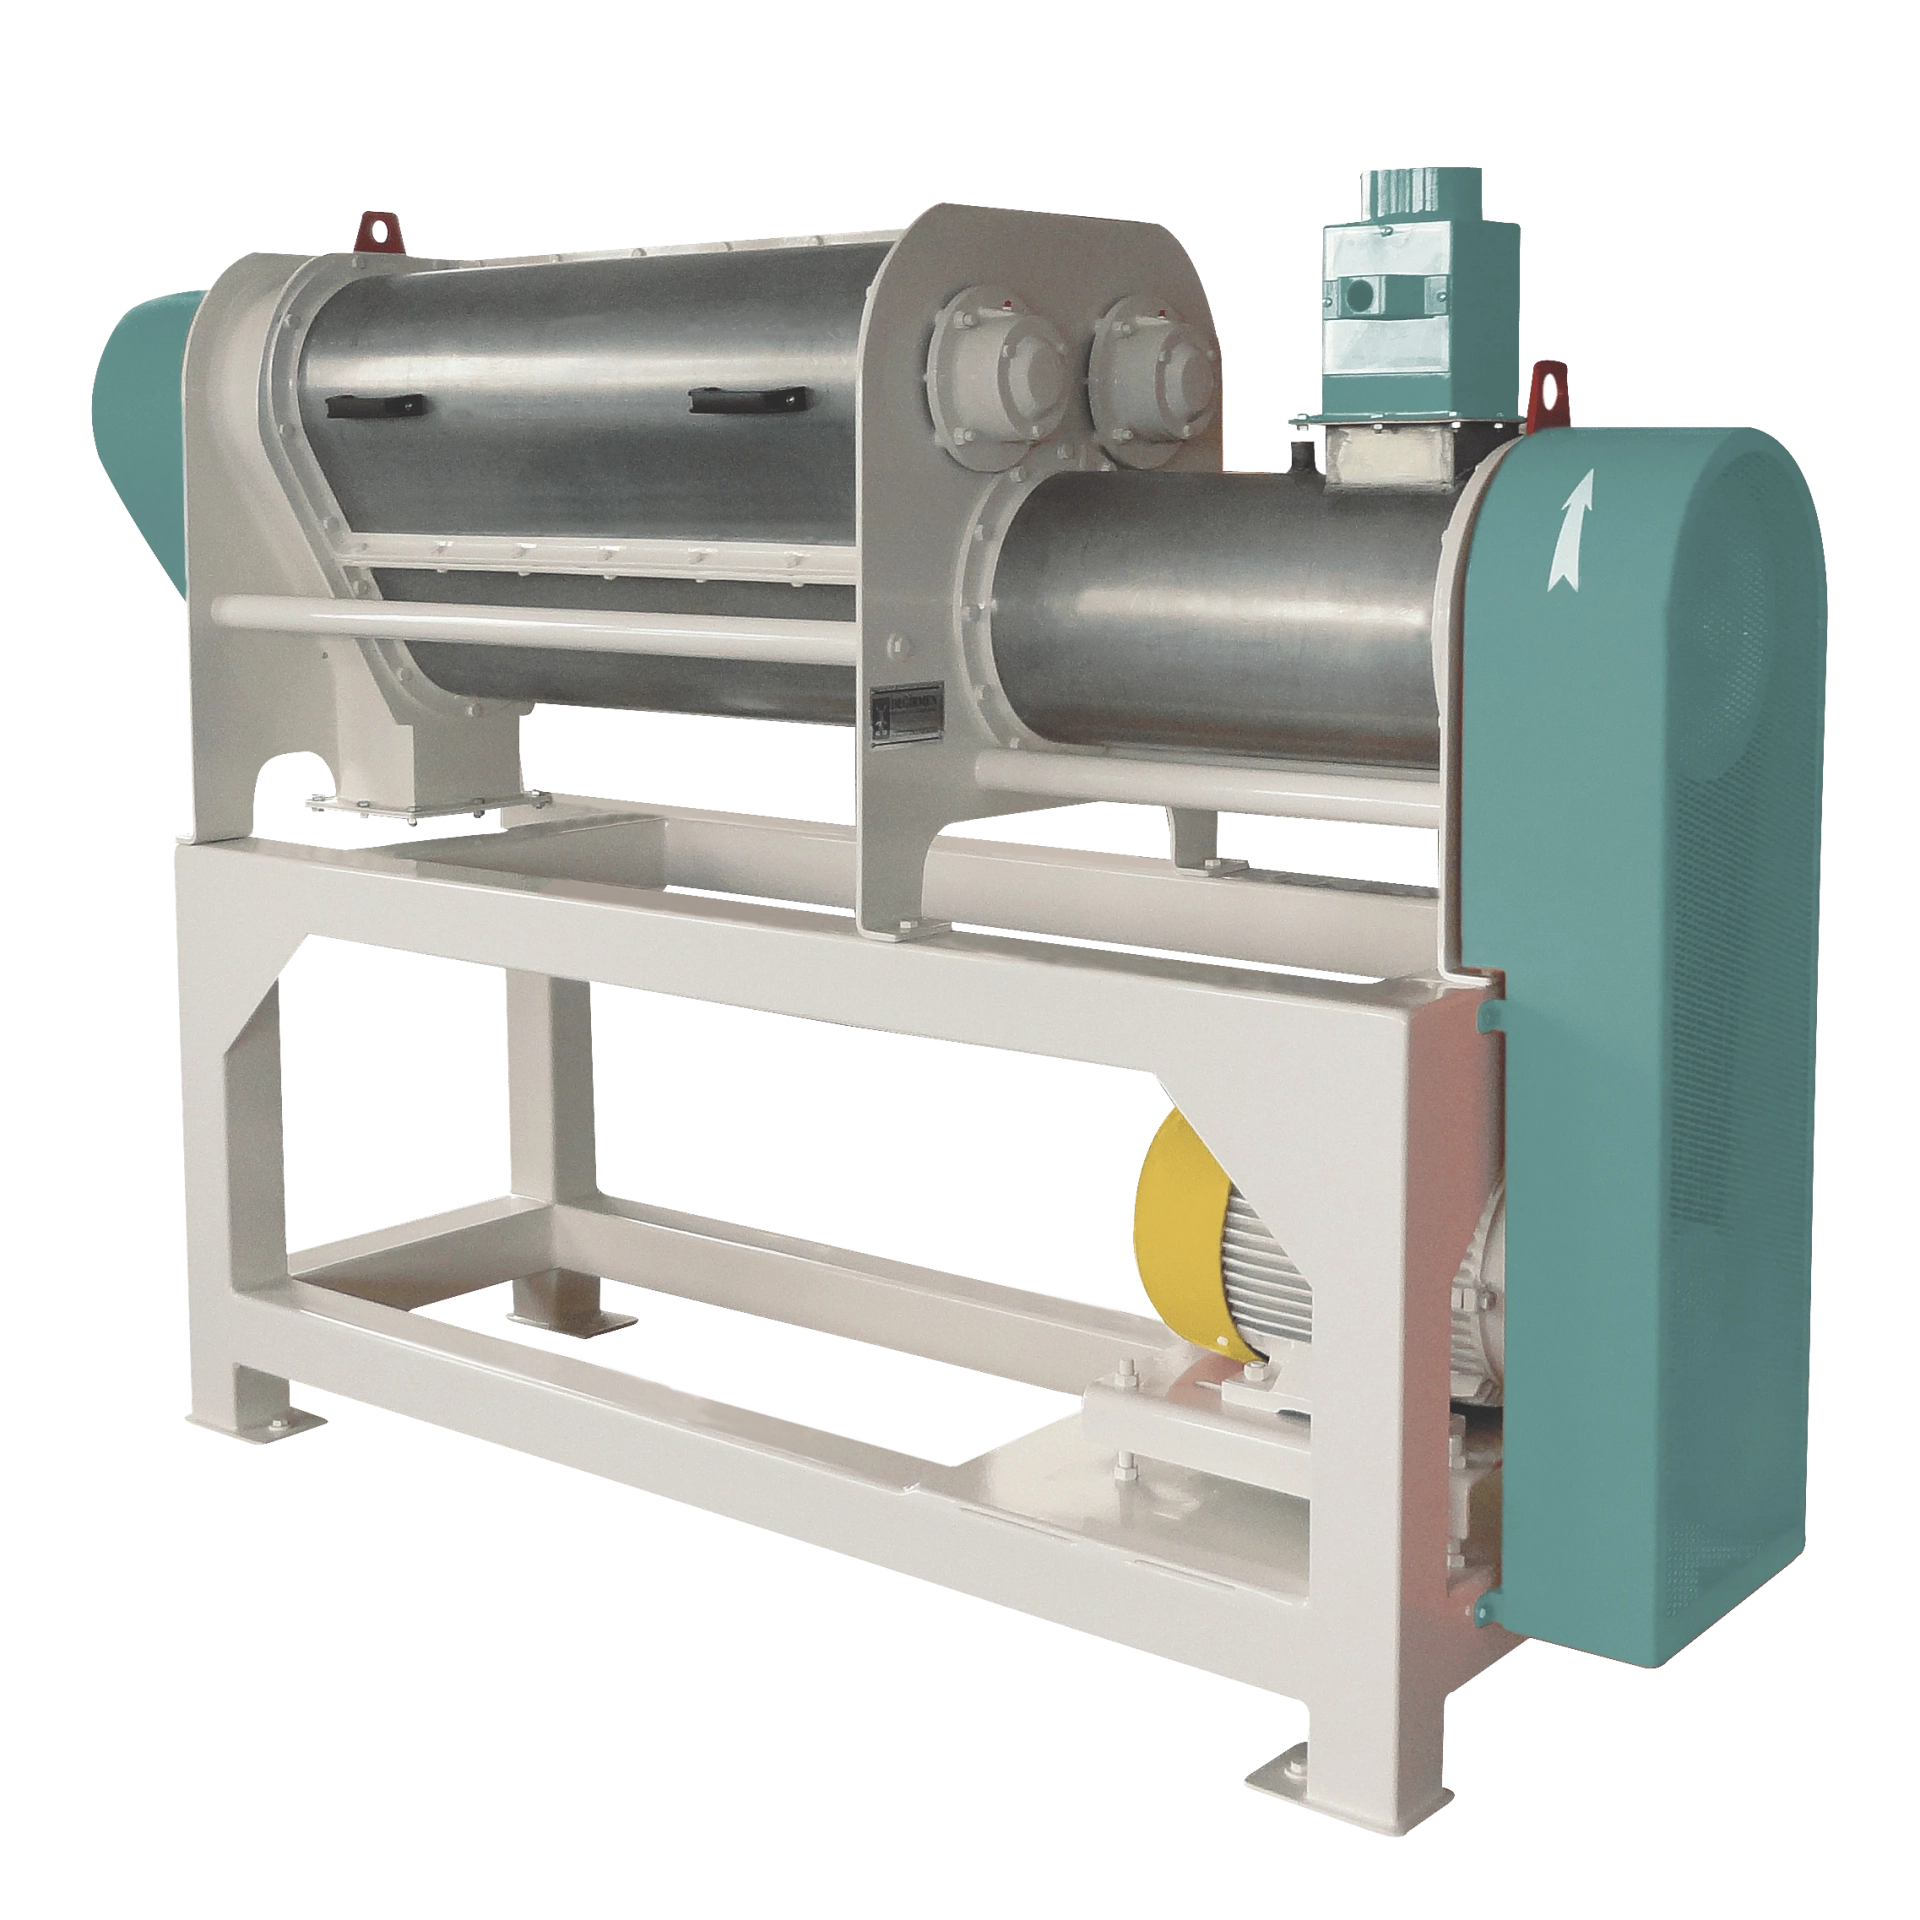
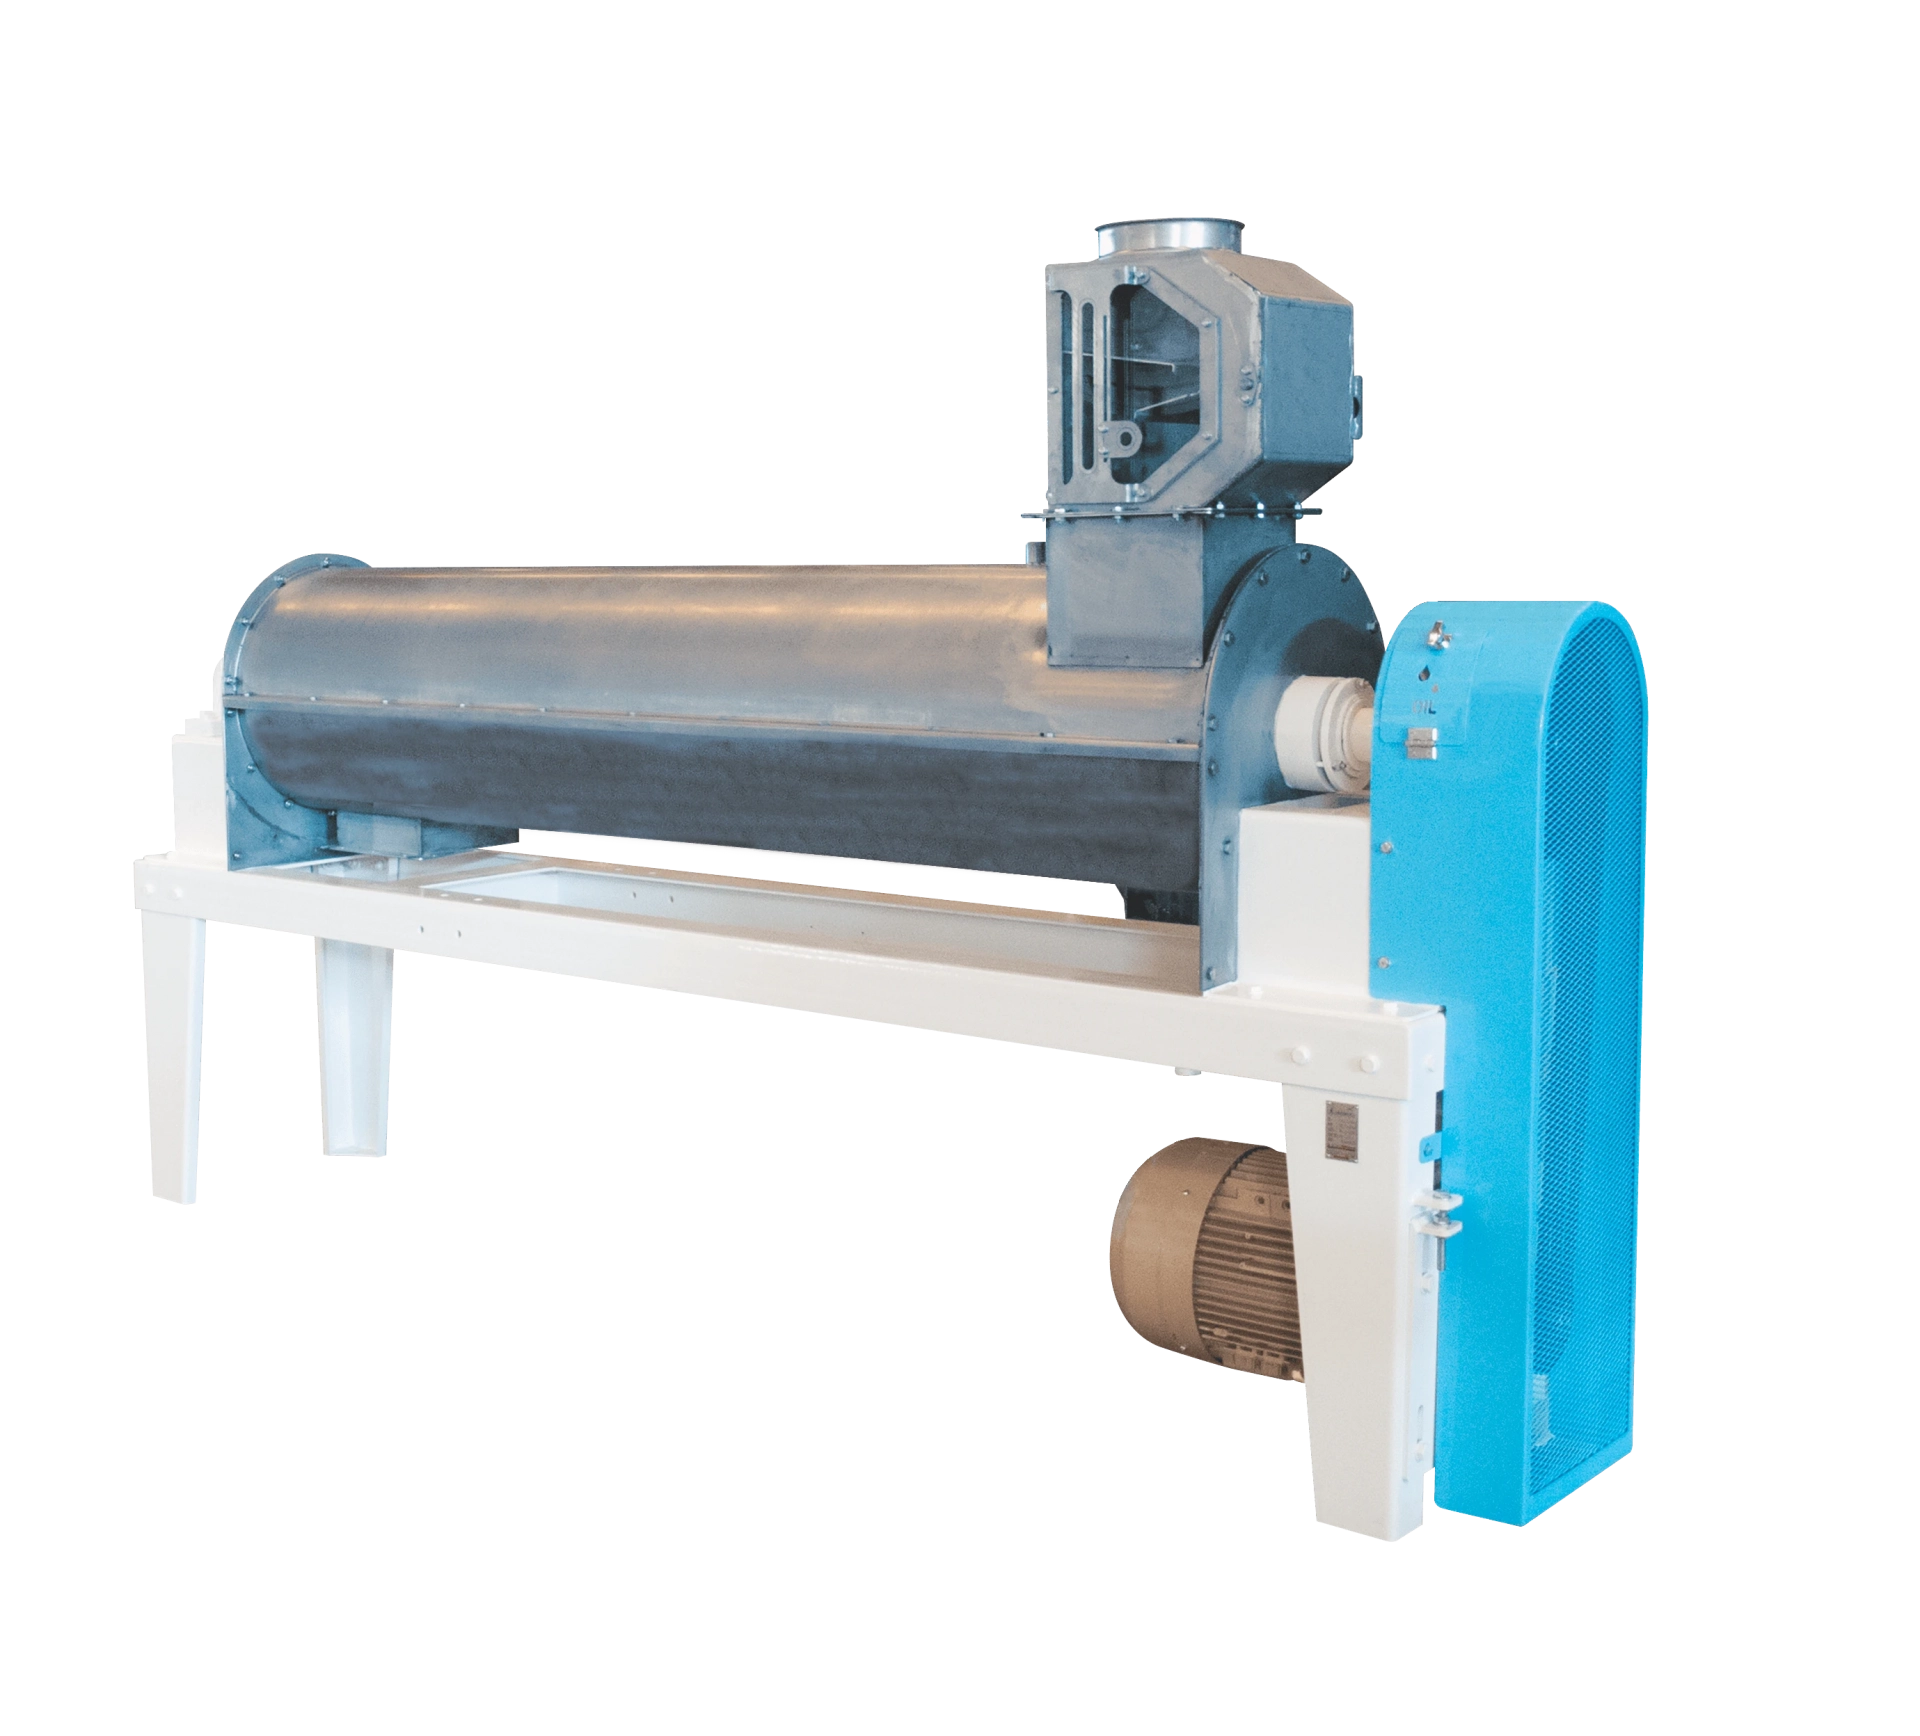
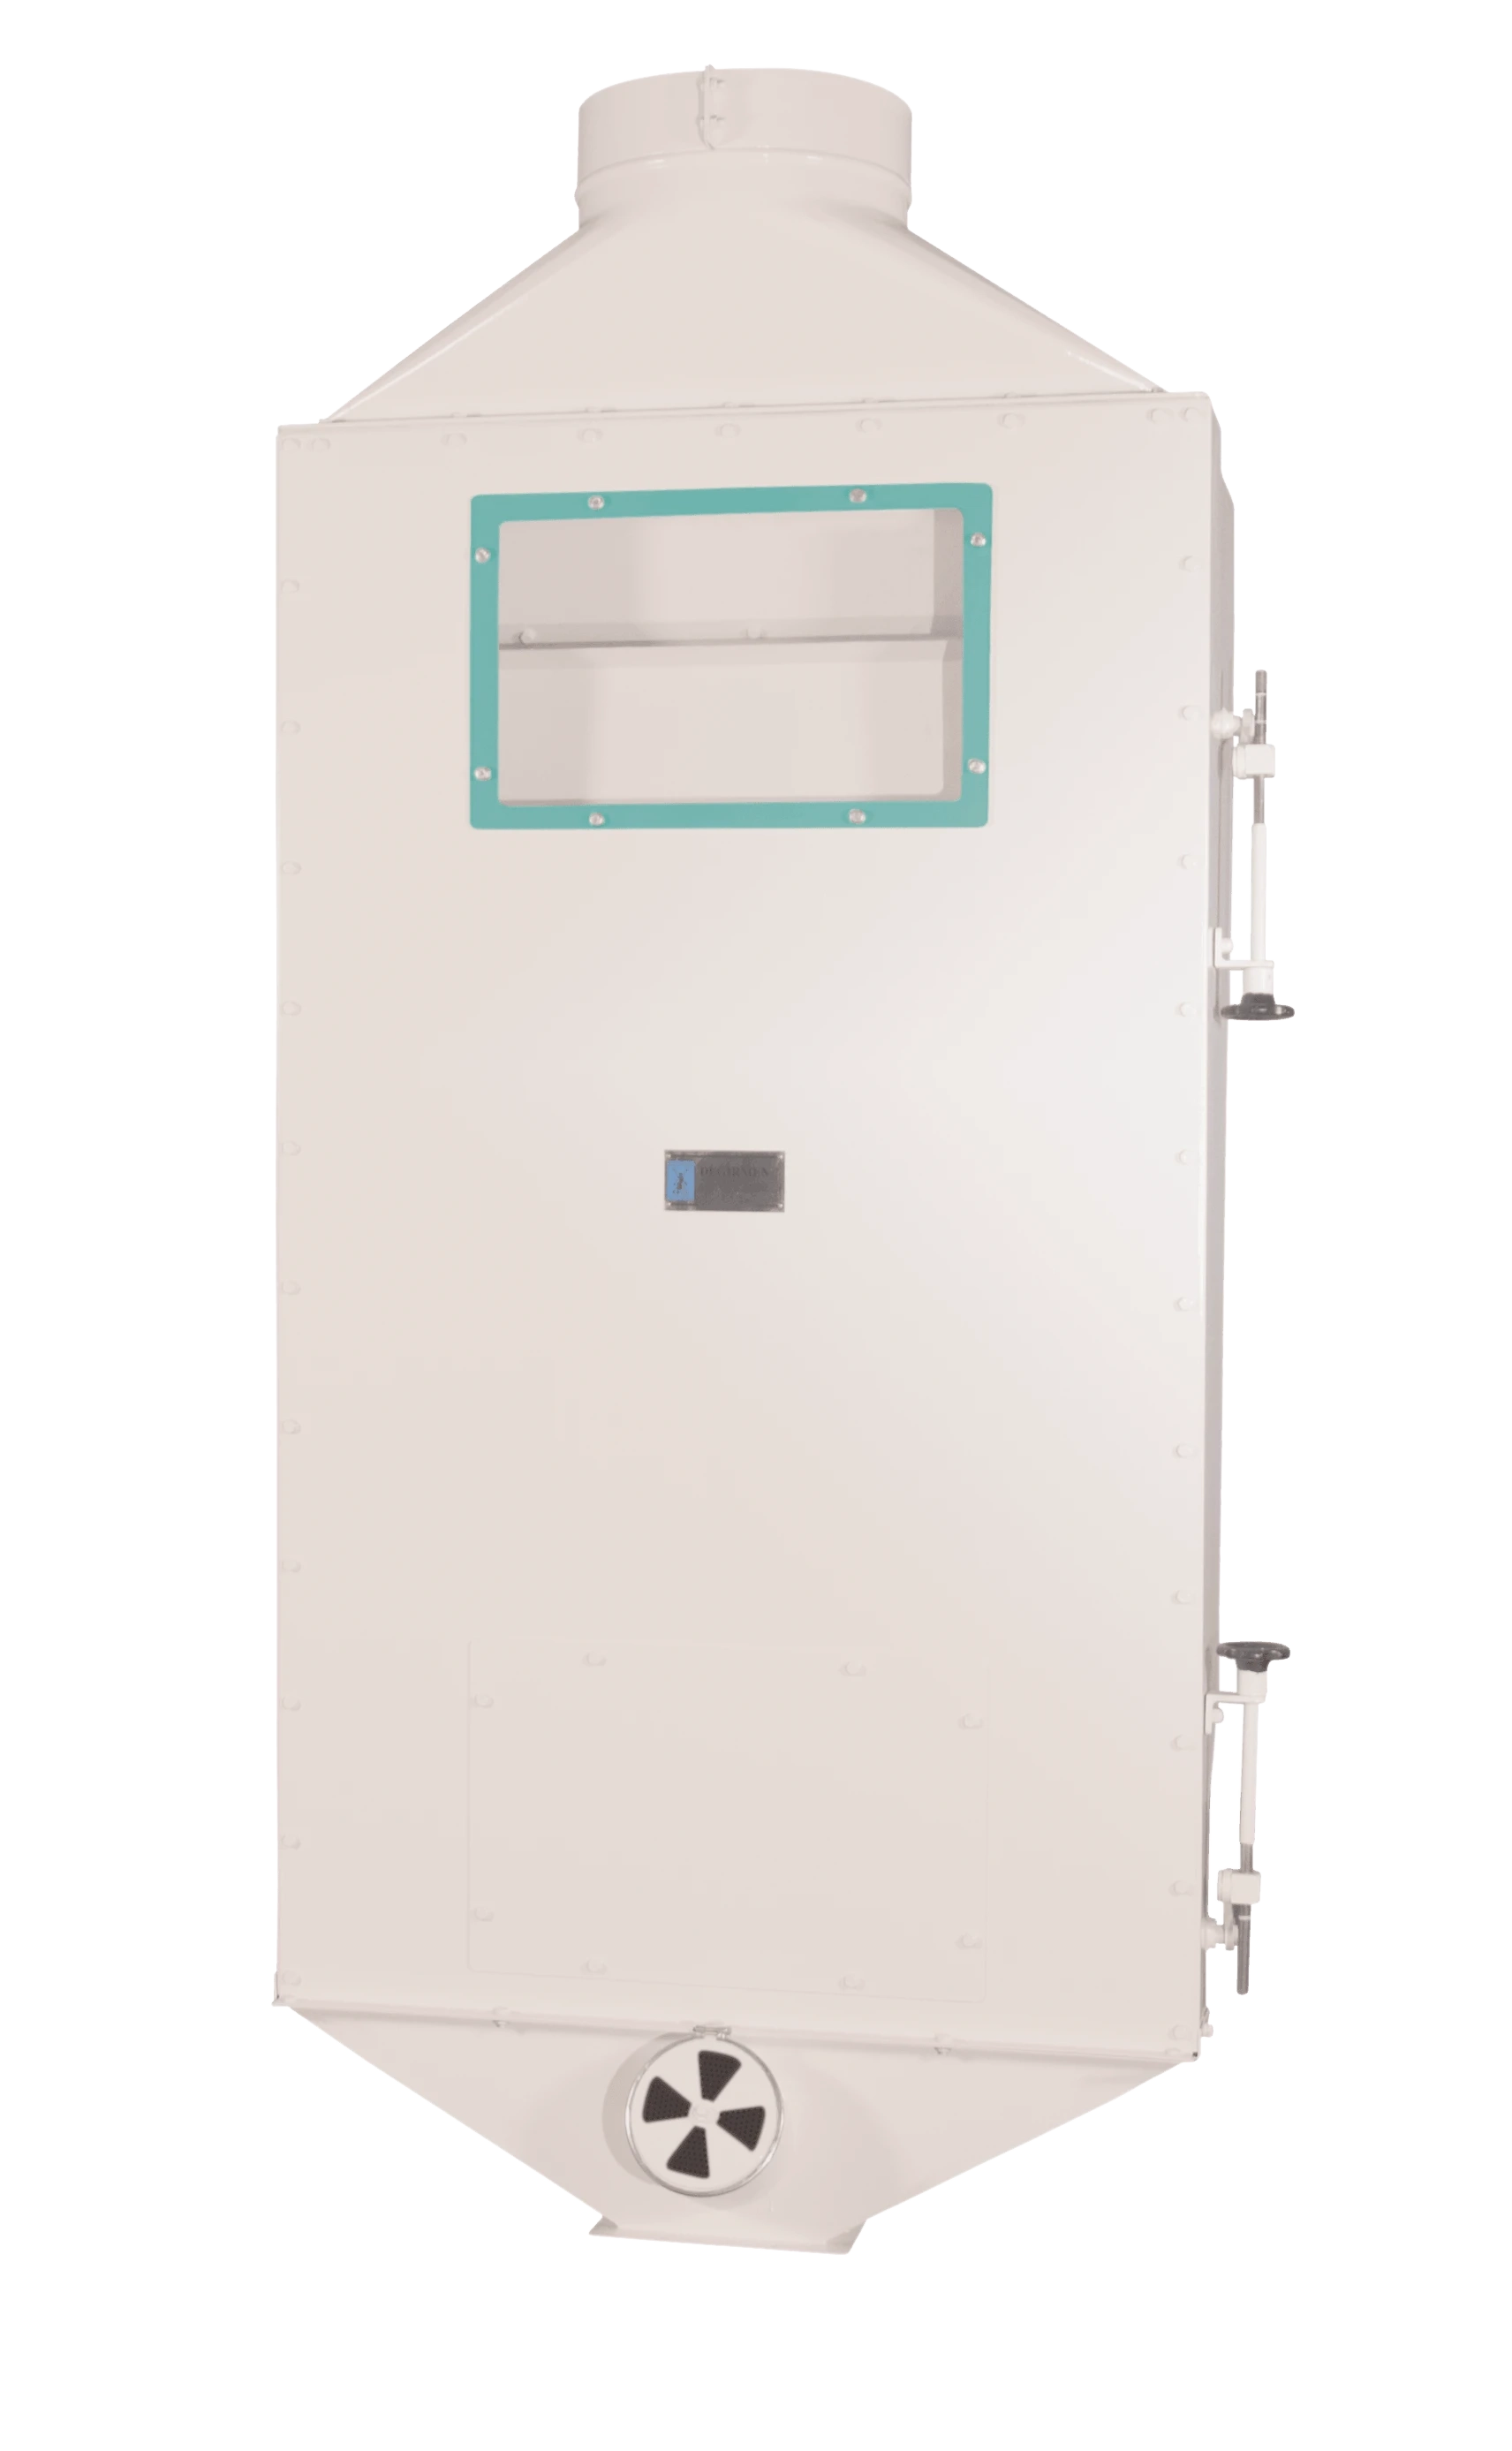
Aspirator with Vibro-Tray and Continuous Air Flow
A high-efficiency cleaning unit for the aerodynamic removal of light kernels, husks, dust and all other airborne foreign matter on grain processing and cleaning lines. Through its vibration technology and intelligent flap system, it delivers maximum separation precision without disturbing the air balance.
WORKING PRINCIPLE
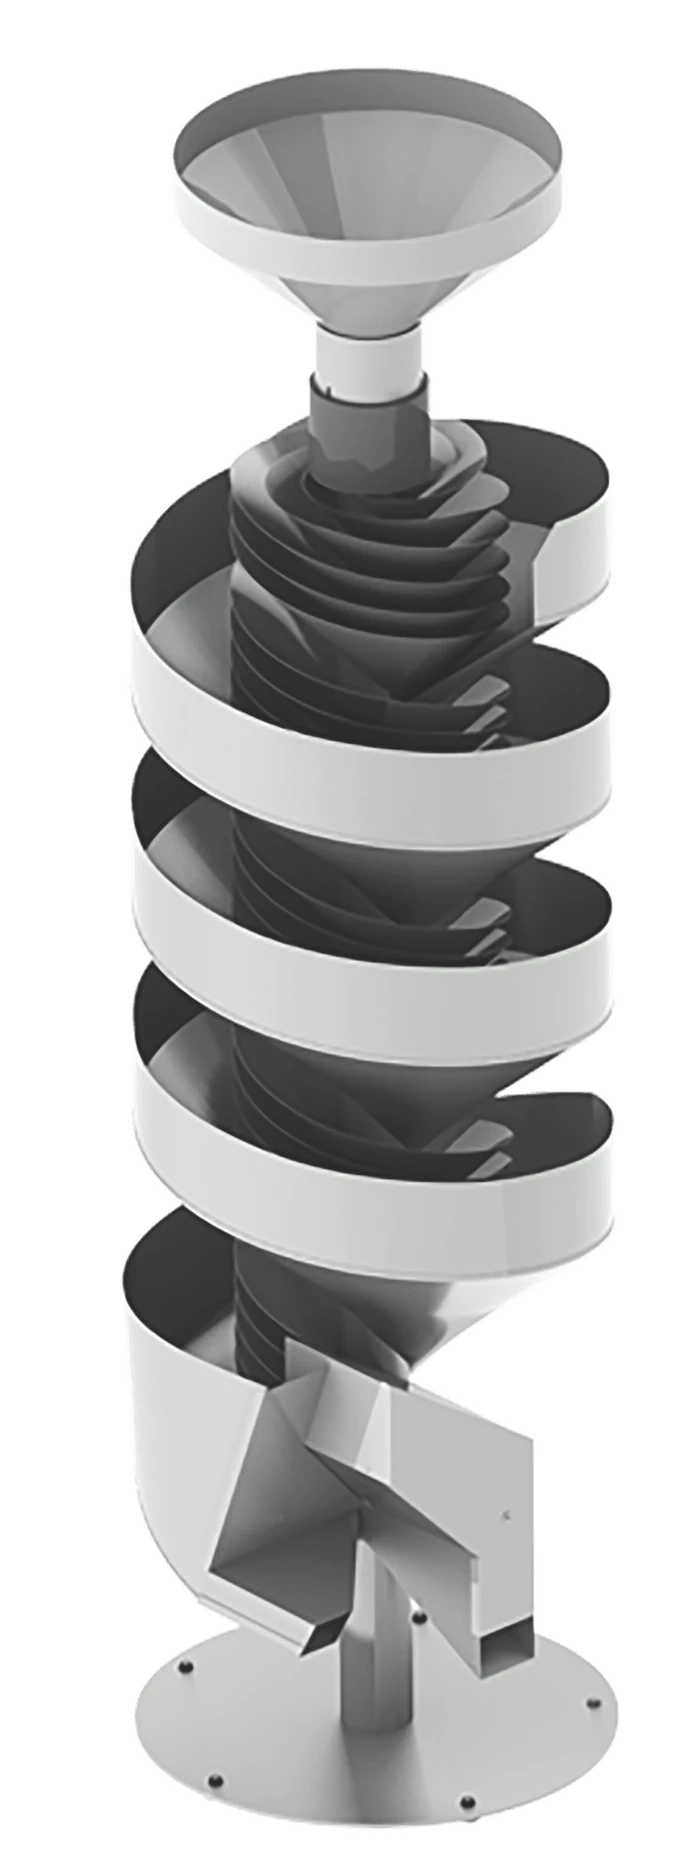
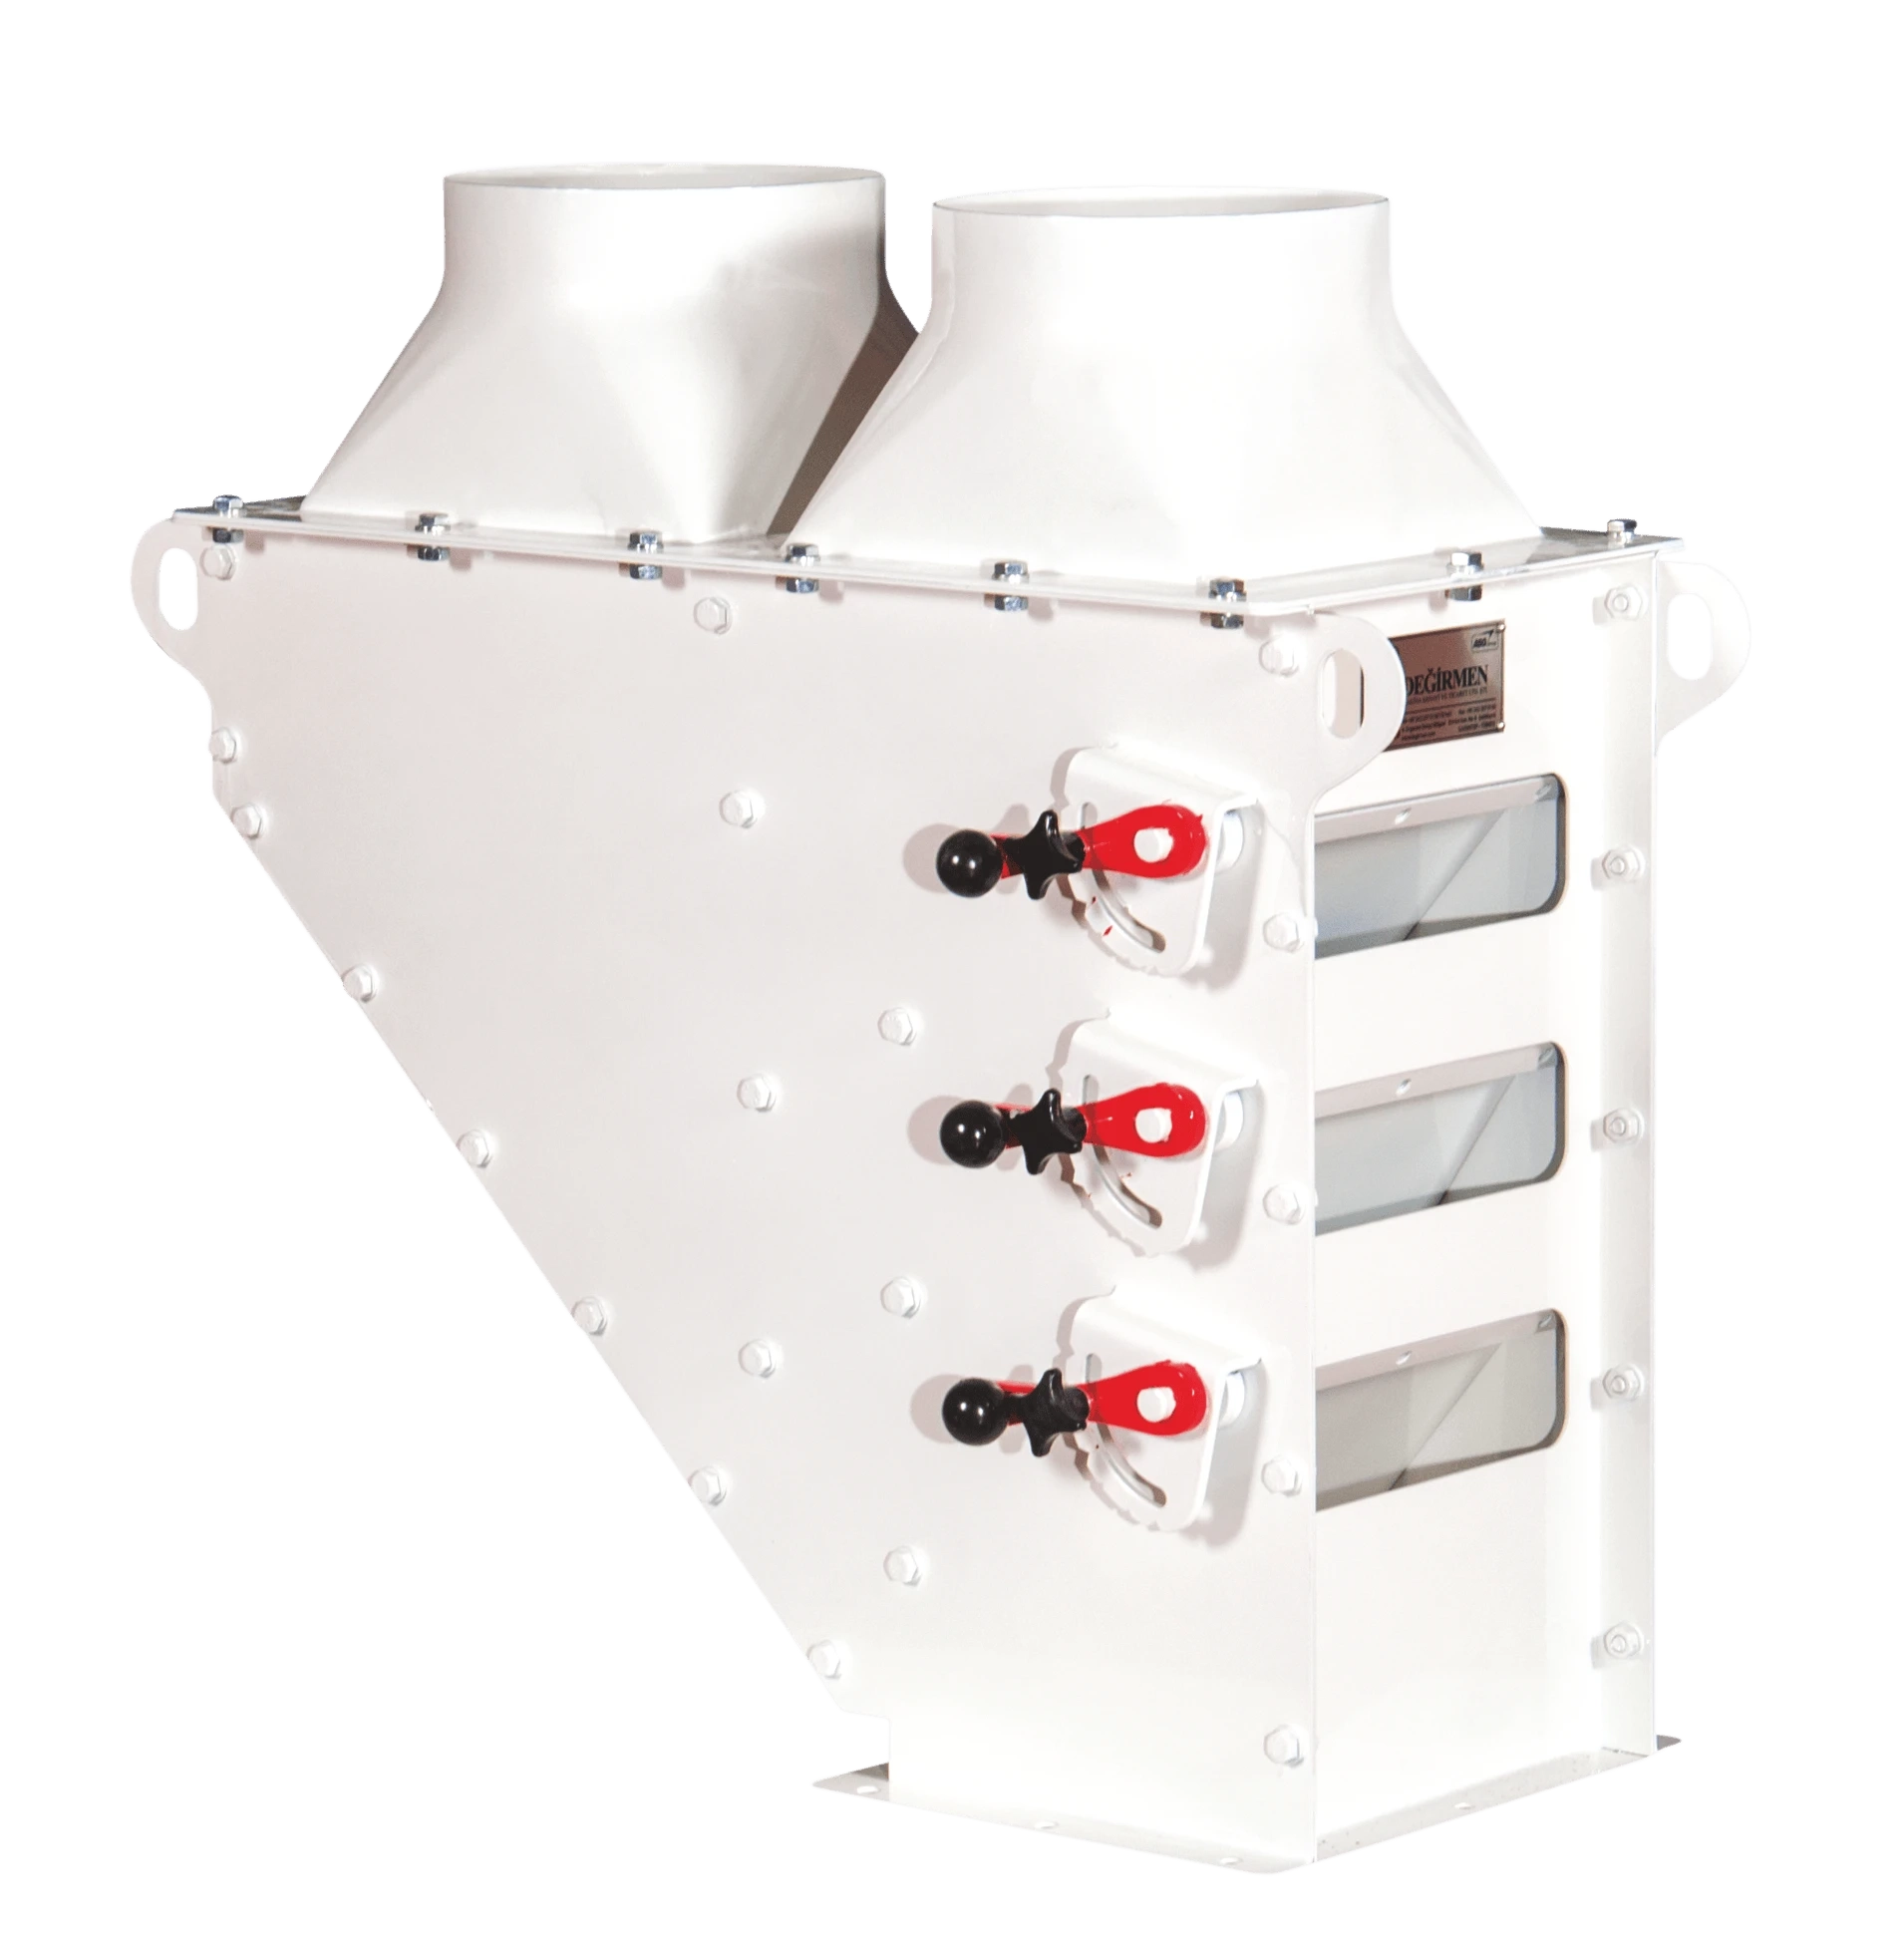
Inlet vibro-tray (uniform curtain): the incoming grain mass is spread evenly across the surface by a vibro-tray, forming a continuous ‘grain curtain’ with no pile-ups. Strong counter-flow air stream (aerodynamic filtration): a powerful air stream passes through the curtain; heavy sound kernels fall while light husks, dust and shrivelled kernels are instantly entrained. Independent sequential flap mechanism (constant-pressure discharge): the separated matter is discharged through sectional flaps that open and close one by one, preventing air in-leakage and keeping a stable static flow inside the machine.
KEY ADVANTAGES
• Stable, continuous air pressure: Sequential opening of the smart flaps prevents uncontrolled air in-leakage during discharge, keeping internal aspiration velocity constant — with no the slightest deviation in quality.
• Transparent process management (plexiglass): High-strength plexiglass viewing windows allow live monitoring of product flow and the air-cleaning moment, with adjustment on the run.
• High vibration-based efficiency: The inlet vibratory drive forms a flawless curtain even on damp or dirty products, guaranteeing 100% air penetration between the kernels.
• Modular capacities & models: A rich range of industrial models to suit different plants’ diagram densities and hourly capacities.
ENGINEERING NOTE
The Vibro Aspirator is an excellent guard station for securing product purity after the mechanical cleaning units. The combination of air-tight mechanical discharge flaps and a vibratory feed tray delivers maximum aerodynamic precision at minimum energy.
 TR
 RU
 ES